

Working Principle and Features of Cobalt Hydroxide Material Handling Equipment
For manufacturers dealing with cobalt hydroxide, efficient material handling is crucial to maintaining production efficiency and product quality. The working principle and features of the specialized equipment designed for this purpose are key to understanding its operational effectiveness and suitability for industrial applications.
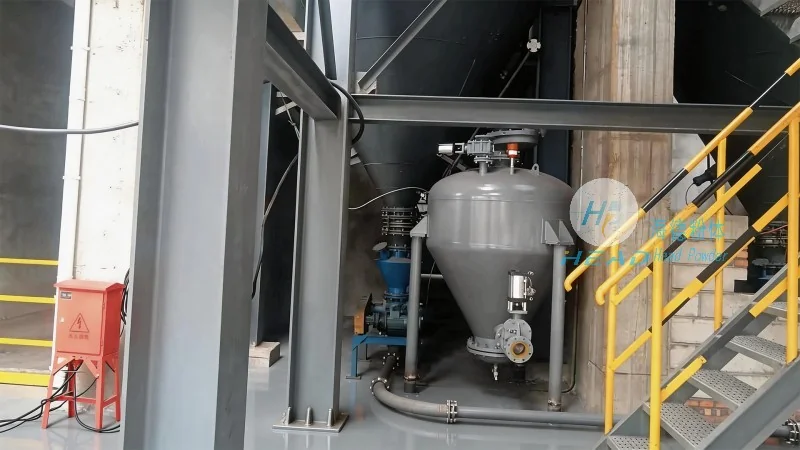
HeadPowder, a leading provider in the field, offers advanced material handling solutions tailored for cobalt hydroxide processing. With a focus on precision and reliability, their equipment is engineered to meet the demands of modern industrial operations. The company, Shandong HeadPowder Engineering Co., Ltd., is based in Shandong, China, and has established a reputation for delivering high-quality engineering solutions that enhance productivity in material handling processes.
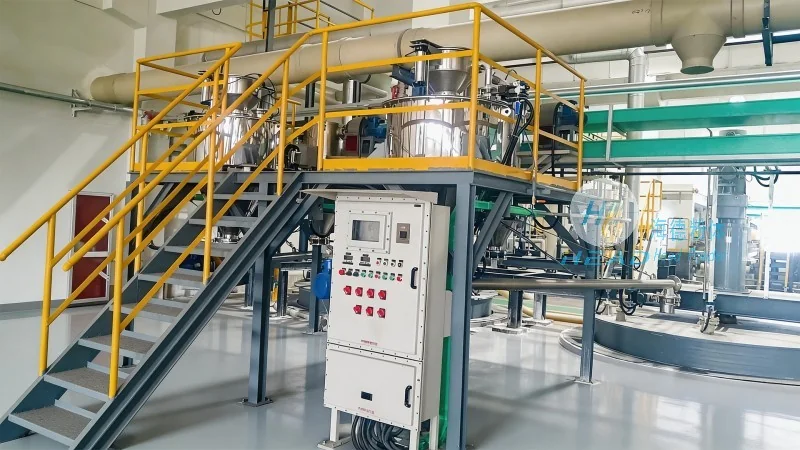
Working Principle of Cobalt Hydroxide Material Handling Equipment
The core working principle of the material handling equipment for cobalt hydroxide involves a series of integrated mechanisms designed to ensure safe and efficient transport of the material. The process typically begins with the loading of cobalt hydroxide into the equipment, where it is then transferred through a series of conveyor systems or pneumatic transport lines. Advanced control systems monitor the flow rate and pressure, ensuring that the material moves smoothly without any blockages or spills. The equipment utilizes low-friction components and specialized seals to prevent contamination and maintain the purity of the cobalt hydroxide, which is critical for downstream processing steps. Additionally, the system incorporates safety features such as overload protection and emergency stop mechanisms to safeguard both the material and the operational environment.
Key Features of Cobalt Hydroxide Material Handling Equipment
Several distinctive features set the material handling equipment for cobalt hydroxide apart from conventional systems. One of the primary features is its ability to handle the material with minimal contamination, which is essential for maintaining the high purity standards required in cobalt hydroxide production. The equipment is designed with corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of cobalt hydroxide and prevent degradation over time. Another notable feature is the adjustable speed control, allowing operators to optimize the transport rate based on production needs and material characteristics. The system also includes real-time monitoring capabilities, providing data on flow rates, temperature, and pressure to facilitate proactive maintenance and operational adjustments. Furthermore, the equipment is built for durability and long-term performance, with modular components that can be easily replaced or upgraded to extend its service life.
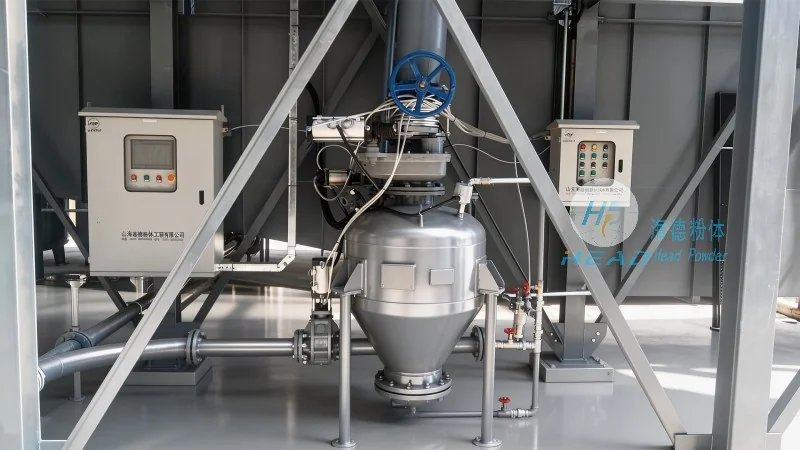
Operational Advantages and Efficiency
The implementation of specialized cobalt hydroxide material handling equipment offers several operational advantages that contribute to overall process efficiency. By reducing the risk of material loss or contamination, the equipment helps maintain consistent product quality, which is vital for meeting customer specifications and regulatory standards. The automated control systems minimize the need for manual intervention, reducing labor costs and the potential for human error. Additionally, the equipment's design allows for seamless integration into existing production lines, ensuring a smooth transition without disrupting ongoing operations. The durability and low maintenance requirements of the equipment further enhance its cost-effectiveness, as it requires fewer repairs and replacements over its service life. Overall, the use of such equipment optimizes the material handling process, leading to improved productivity and reduced operational costs for manufacturers.