

Principle and Working Scene Characteristics of Tonne Bag Material Handling Systems
Efficient material handling is a critical component of modern industrial operations, and tonne bag material handling systems have emerged as a robust solution for managing large volumes of bulk materials. These systems are designed to streamline the process of handling, transporting, and storing tonne bags, which are commonly used for transporting bulk goods such as chemicals, minerals, and agricultural products. The following content explores the fundamental principles of tonne bag material handling systems and highlights key characteristics of their operational scenarios.
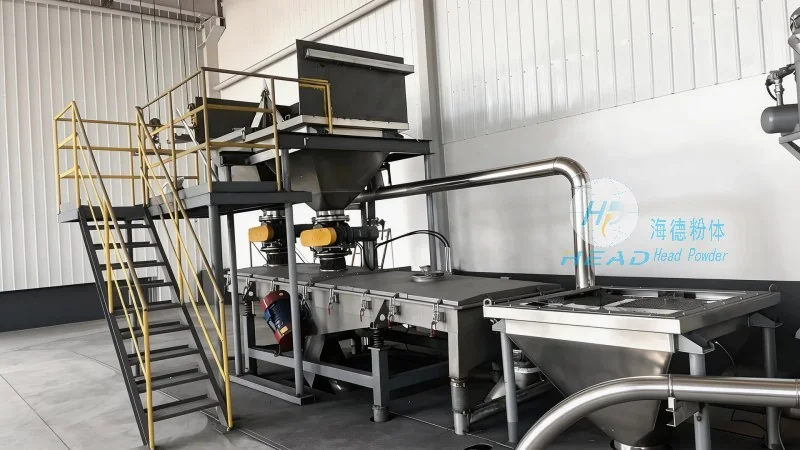
Introduction to Tonne Bag Material Handling Systems
Tonne bags, also known as super sacks or bulk bags, are large, flexible containers capable of holding substantial quantities of material—typically ranging from 500 kg to several tons. These bags are widely utilized in industries where bulk material transport is essential due to their cost-effectiveness and ease of handling. The tonne bag material handling system integrates various components, including loading mechanisms, conveying equipment, and storage solutions, to ensure seamless material flow from the point of origin to the final destination.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of material handling solutions, is headquartered in Shandong, China. With a strong commitment to innovation and quality, the company specializes in designing and manufacturing advanced systems tailored to the needs of diverse industrial sectors. HeadPowder's expertise lies in optimizing material handling processes, enhancing operational efficiency, and ensuring compliance with industry standards. The company's facilities and technical team are dedicated to delivering reliable and durable solutions that meet the evolving demands of modern industries.
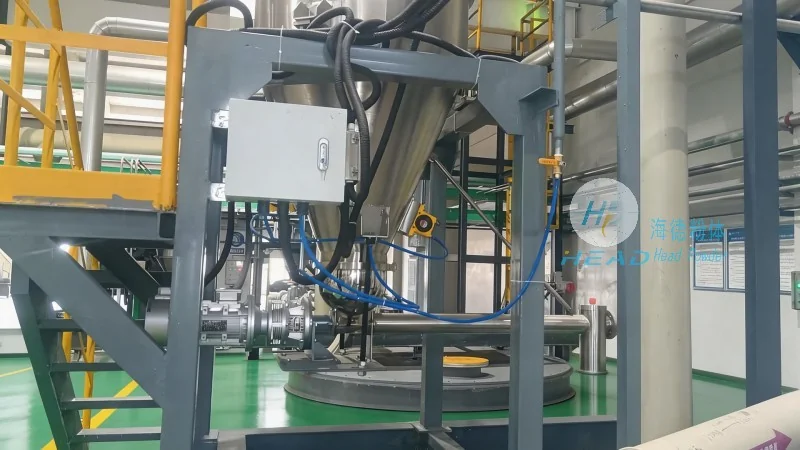
The Principle of Tonne Bag Material Handling Systems
The core principle of tonne bag material handling systems revolves around the efficient transfer of bulk materials while maintaining the integrity of the tonne bags. The system typically operates through a combination of mechanical and hydraulic components that facilitate the loading, lifting, and conveying of the bags. For instance, loading operations may involve using a hopper or a loading platform to fill the tonne bags with material, followed by sealing mechanisms to prevent spillage. The conveying phase often employs conveyor belts, elevators, or pneumatic systems to transport the filled bags to storage or processing areas. The system is designed to minimize manual labor, reduce handling time, and enhance safety by automating critical steps in the material handling process.
Key Working Scene Characteristics
The operational characteristics of tonne bag material handling systems vary significantly based on the specific industry and application. In chemical manufacturing, for example, these systems are used to handle hazardous materials, requiring strict safety protocols and specialized equipment to prevent contamination or accidents. The systems are equipped with features such as sealed loading areas and emergency shut-off mechanisms to ensure compliance with environmental and safety regulations. In mining and mineral processing, tonne bag handling systems are crucial for transporting raw materials from extraction sites to processing facilities, where the ability to handle large volumes efficiently is paramount. The systems are often integrated with bulk material storage silos or hoppers, allowing for continuous material flow and reducing downtime.
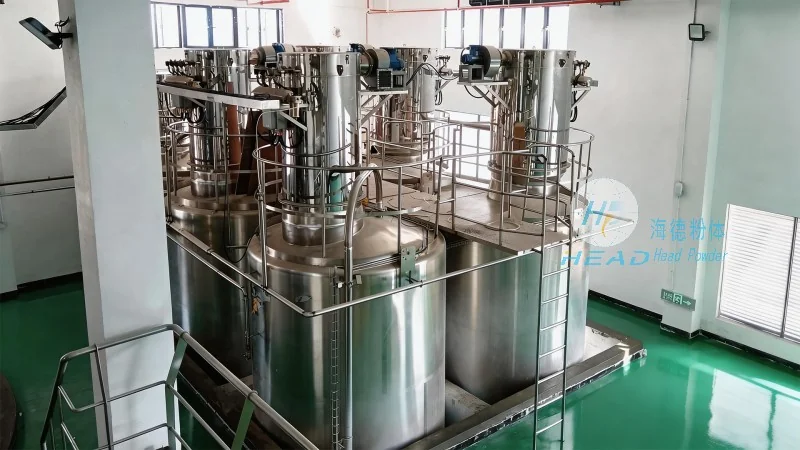
Applications and Operational Efficiency
Tonne bag material handling systems are versatile and can be adapted to a wide range of applications, from small-scale operations to large industrial plants. The flexibility of the system allows it to handle various types of materials, including powders, granules, and liquids, by adjusting the design of the tonne bags and the conveying equipment. The operational efficiency of these systems is measured by factors such as throughput capacity, energy consumption, and maintenance requirements. Advanced systems incorporate sensors and automation controls to monitor performance in real-time, enabling operators to optimize the process and reduce operational costs. The reliability of the system is further enhanced by the use of durable materials and regular maintenance schedules, ensuring consistent performance over extended periods.
Conclusion
Tonne bag material handling systems represent a sophisticated solution for managing bulk materials in industrial settings. By integrating advanced technology and robust design, these systems enhance operational efficiency, reduce labor costs, and improve safety. As industries continue to evolve, the demand for efficient material handling solutions will remain high, making tonne bag material handling systems a vital component of modern industrial operations. With its expertise and commitment to quality, Shandong HeadPowder Engineering Co., Ltd. plays a significant role in providing tailored solutions that meet the specific needs of various industries, contributing to the overall advancement of material handling technologies.