

Principle and Working Scene Characteristics of PFA Powder Pneumatic Conveyor
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced PFA powder pneumatic conveyors. These systems are engineered to efficiently handle PFA powders, a fluoropolymer known for its excellent chemical resistance, thermal stability, and non-stick properties. The PFA powder pneumatic conveyor is a critical piece of equipment in industries where PFA materials are processed, offering reliable and safe material transport solutions.
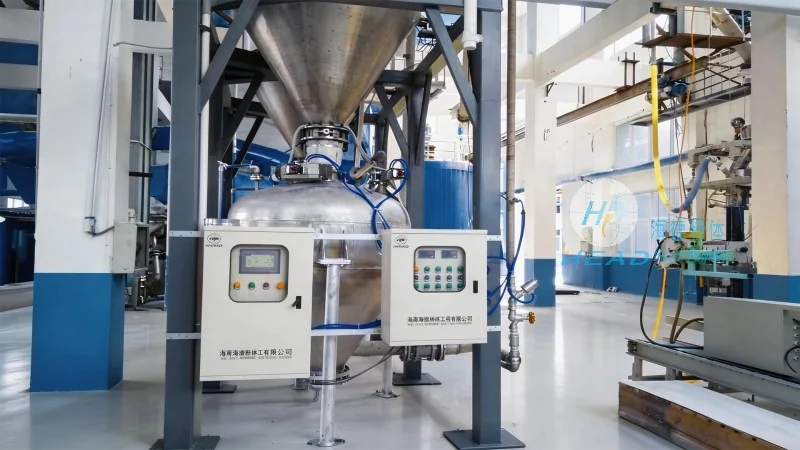
Understanding the Working Principle of PFA Powder Pneumatic Conveyors
The core principle of a pneumatic conveyor involves using compressed air or gas to transport bulk powders through a pipeline system. In the case of PFA powder conveyors, the system is specifically tailored to handle the unique characteristics of PFA powders, such as their fine particle size and potential for static charge accumulation. The conveyor typically consists of a hopper for material storage, a blower or compressor to generate the air flow, and a series of pipes with appropriate fittings. The material is introduced into the hopper and then drawn into the pipeline by the airflow, moving from the inlet to the discharge point. The design ensures that the PFA particles are conveyed without clogging or degradation, maintaining the integrity of the material throughout the process.
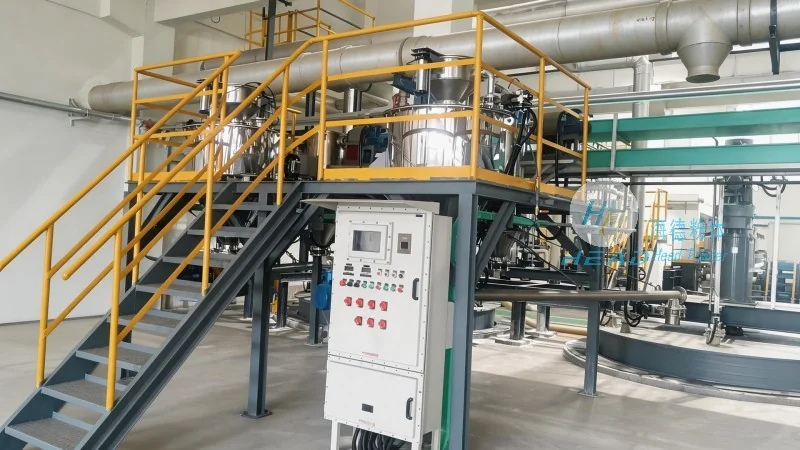
Key Working Scene Characteristics of PFA Powder Pneumatic Conveyors
The application of PFA powder pneumatic conveyors is characterized by several key features that make them suitable for specific industrial environments. Firstly, these systems are ideal for applications requiring high purity and minimal contamination, as the enclosed pipeline design prevents exposure to external elements. Secondly, they offer flexibility in terms of layout, allowing for vertical, horizontal, or mixed-direction transport, which is crucial for complex production lines. Thirdly, the conveyors are designed to handle varying particle sizes and flow rates, ensuring consistent performance even with changes in material properties. Additionally, the systems are equipped with features like pressure relief valves and filtration systems to maintain operational safety and material quality. In industrial settings, such as chemical processing plants, PFA manufacturing facilities, and research laboratories, these conveyors play a vital role in streamlining material handling processes and enhancing overall operational efficiency.
Advantages and Practical Applications in Industrial Settings
HeadPowder's PFA powder pneumatic conveyors offer several advantages that make them a preferred choice for industries dealing with PFA materials. The primary benefit is the ability to transport PFA powders over long distances without the need for mechanical components like belts or screws, which can introduce contamination or wear. This also reduces maintenance costs and downtime. Another advantage is the system's ability to handle both dry and slightly moist PFA powders, adapting to different production requirements. In practical applications, these conveyors are used in the production of PFA tubing, PFA fittings, and other fluoropolymer products, where consistent material quality is essential. They are also employed in the handling of PFA powders during research and development, where precise control over material transport is critical. The systems are designed to meet the stringent requirements of various industries, including pharmaceuticals, electronics, and aerospace, where PFA's properties are leveraged for specialized applications.
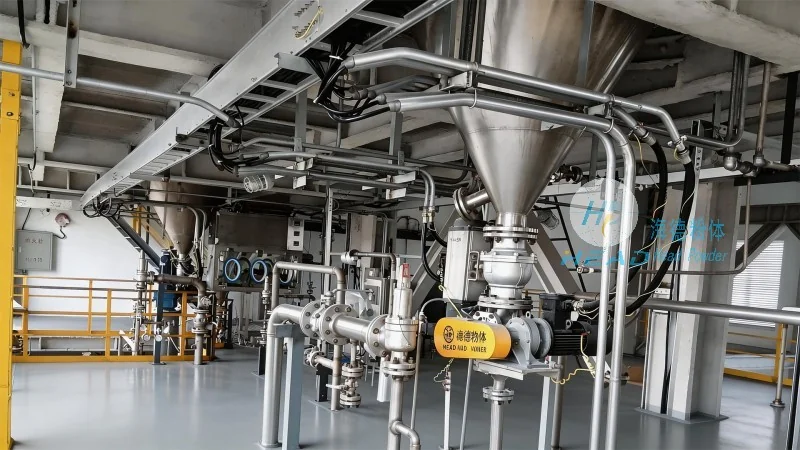
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to innovate in the field of PFA powder pneumatic conveyors, providing tailored solutions that meet the diverse needs of industrial clients. By combining advanced engineering with a deep understanding of PFA material properties, HeadPowder ensures that its conveyors deliver reliable performance, high efficiency, and long-term durability. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the global market for PFA processing equipment. As industries increasingly rely on PFA materials for their unique performance characteristics, the demand for efficient and reliable PFA powder conveyors remains strong, and HeadPowder is positioned to meet this demand with cutting-edge technology and expert service.