

Principle and Working Scene Characteristics of Automatic Quantitative Powder Material Pneumatic Conv
Automatic quantitative powder pneumatic conveying systems represent a sophisticated technology designed to handle the precise and efficient transportation of bulk powder materials. These systems are engineered to meet the stringent requirements of various industrial applications, ensuring accurate material measurement and reliable transport under diverse operational conditions.
Core Principles of Pneumatic Conveying Technology
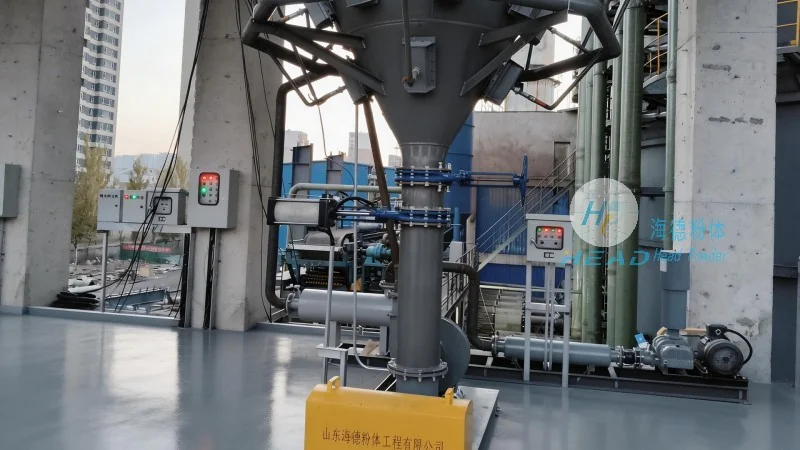
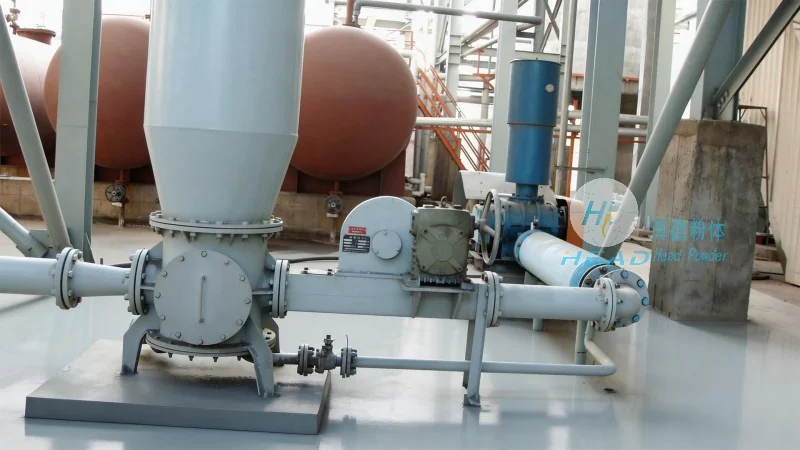
The fundamental principle of pneumatic conveying involves the use of a pressurized or vacuum environment to move powder materials through a pipeline. In an automatic quantitative system, this process is integrated with advanced control mechanisms to achieve precise dosage and consistent flow rates. The system typically comprises several key components, including a material feeder, a conveying pipeline, a pressure vessel or receiver, and a control unit. The material feeder is responsible for delivering the powder to the pipeline at a controlled rate, while the conveying medium—often air or a mixture of air and other gases—propels the material through the system. The control unit monitors and adjusts the flow parameters in real-time, ensuring that the material is conveyed accurately and without loss or degradation.
Key Working Scene Characteristics
The working scene characteristics of these systems are tailored to address the specific demands of different industrial environments. For instance, in pharmaceutical manufacturing, where product purity and contamination control are paramount, the system must operate under sterile conditions and maintain strict particle size uniformity. In the food processing industry, the equipment must be constructed from food-grade materials and comply with hygiene regulations to prevent cross-contamination. Similarly, in chemical processing, the system is designed to handle abrasive or corrosive powders, utilizing durable components and specialized sealing mechanisms to ensure long-term reliability. Additionally, the systems are adaptable to varying production scales, from small-scale laboratory applications to large-scale industrial production lines, making them versatile for diverse operational needs.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
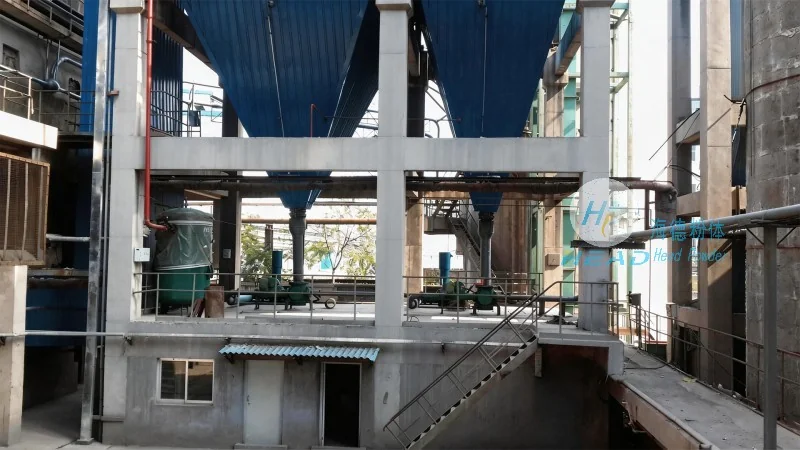
HeadPowder, a leading provider of advanced powder handling solutions, specializes in the design, manufacturing, and integration of automatic quantitative pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to enhance operational efficiency, reduce material waste, and improve overall process control. The company's expertise lies in customizing solutions to meet the unique requirements of each client, ensuring optimal performance and reliability in demanding industrial environments. HeadPowder's products are backed by rigorous testing and compliance with international standards, reflecting the company's dedication to excellence and customer satisfaction.
Applications and Benefits
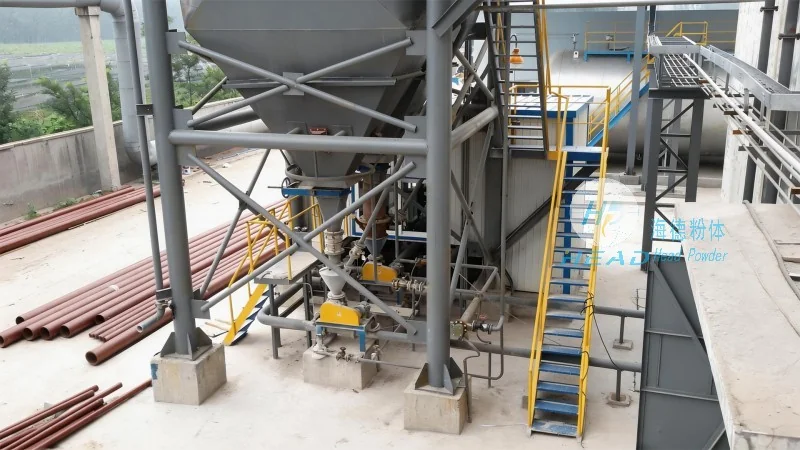
The automatic quantitative powder pneumatic conveying systems developed by HeadPowder find wide applications across multiple sectors. In the chemical industry, these systems are used for transporting raw materials and finished products, improving production throughput and reducing labor costs. In the food and beverage sector, they facilitate the efficient handling of powders such as flour, sugar, and protein supplements, maintaining product quality and consistency. The pharmaceutical industry benefits from the system's ability to handle sensitive materials with minimal exposure to air and contaminants, ensuring compliance with regulatory standards. Furthermore, the systems offer significant advantages in terms of space efficiency, as they can be installed in compact areas while maintaining high throughput. The integration of advanced control technology also enables remote monitoring and data analysis, allowing for proactive maintenance and process optimization.