

Clean Solution for Efficient Sorghum Distillers Grains Conveying: An In-Depth Look at Pneumatic Conv
For manufacturers in the distillery industry, the efficient and hygienic handling of sorghum distillers grains is a critical operational challenge. Traditional methods, such as belt conveyors or screw conveyors, often introduce contamination risks and require frequent cleaning, which can disrupt production schedules and increase maintenance costs. Pneumatic conveying technology offers a superior solution, providing a clean, dust-free, and highly efficient method for transporting these high-value byproducts. This article explores the benefits and applications of pneumatic conveying systems specifically designed for sorghum distillers grains, highlighting how they enhance productivity and maintain product quality.
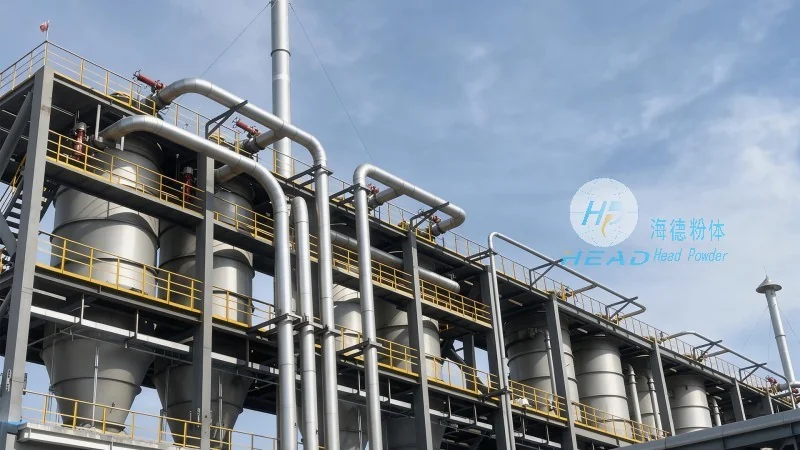
Pneumatic Conveying: How It Works and Its Advantages
Pneumatic conveying systems use air or gas to transport bulk materials through a pipeline network. In the context of sorghum distillers grains, these systems typically employ a positive pressure or negative pressure (vacuum) approach. Positive pressure systems push material through the pipeline using a blower, while negative pressure systems draw material in using a vacuum pump. The choice between the two depends on factors like material characteristics, distance, and system layout. The key advantages of pneumatic conveying for distillers grains include: 1) Hygienic and Clean Operation: Unlike mechanical conveyors, pneumatic systems eliminate direct contact with the material, reducing the risk of contamination from equipment wear or external sources. This is particularly important for food and beverage byproducts that may be used in animal feed or other applications where purity is essential. 2) High Efficiency and Capacity: Pneumatic conveyors can handle large volumes of material at high speeds, significantly reducing the time required for material transport compared to traditional methods. This leads to increased production throughput and lower labor costs. 3) Flexibility and Scalability: The modular design of pneumatic systems allows for easy expansion or reconfiguration as production needs change. This adaptability is valuable for distilleries that may need to adjust their processing capacity over time. 4) Reduced Maintenance: With fewer moving parts compared to mechanical conveyors, pneumatic systems experience lower wear and tear, resulting in lower maintenance requirements and longer equipment lifespan.
HeadPowder Engineering: Pioneering Pneumatic Solutions for Distilleries
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial conveying equipment, specializes in developing customized pneumatic conveying systems tailored to the unique needs of the distillery industry. With years of experience in the field, HeadPowder has developed a range of solutions designed to optimize the handling of sorghum distillers grains. The company’s products are engineered to meet stringent hygiene standards, ensuring that the material remains clean and free from contaminants throughout the conveying process. HeadPowder’s team of engineers works closely with clients to assess their specific operational requirements, from material flow rates and pipeline lengths to environmental and safety considerations, to design a system that maximizes efficiency and minimizes downtime.
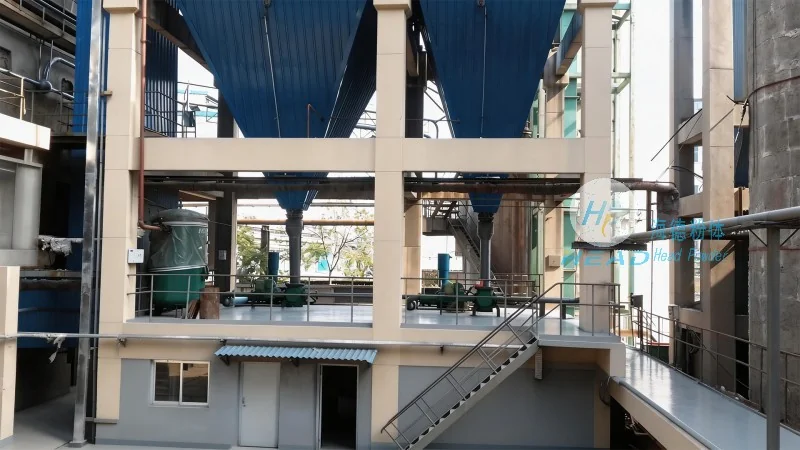
Key Features of HeadPowder’s Pneumatic Conveying Systems
HeadPowder’s pneumatic conveying systems for sorghum distillers grains are equipped with several advanced features that enhance performance and reliability: 1) Advanced Material Handling Design: The systems are designed to handle the specific properties of sorghum distillers grains, including their moisture content and particle size distribution. This ensures smooth and consistent material flow without blockages or clogging. 2) Energy-Efficient Blowers and Vacuum Pumps: HeadPowder uses high-efficiency blower and vacuum pump technologies to minimize energy consumption while maintaining optimal conveying performance. This not only reduces operational costs but also aligns with sustainability goals. 3) Modular and Easy to Install: The components of the system are designed for easy installation and maintenance, allowing for quick setup and minimal disruption to existing production lines. 4) Customizable Control Systems: The conveying systems can be integrated with existing control panels or automated systems, providing real-time monitoring and control of material flow. This enables operators to adjust parameters as needed to optimize performance.
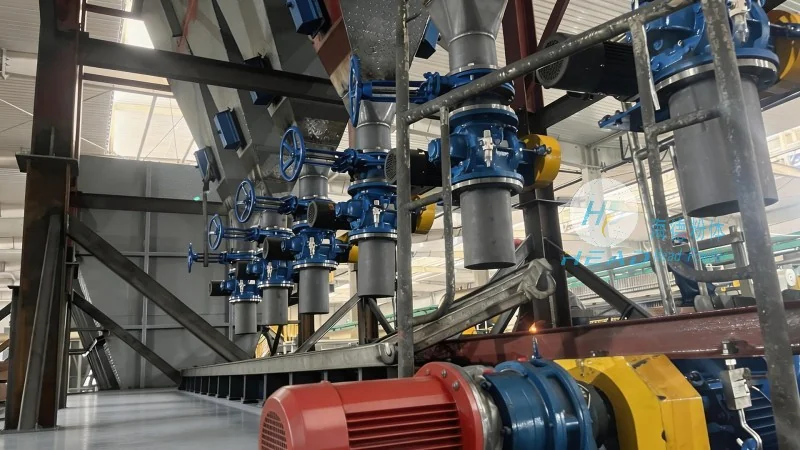
Applications and Use Cases
The applications of pneumatic conveying for sorghum distillers grains are diverse and widespread across the distillery industry. Some common use cases include: 1) Transporting Grains from Fermentation Tanks to Storage Silos: After fermentation, the distillers grains are collected from the tanks and conveyed to storage silos for later use as animal feed or for further processing. Pneumatic systems provide a clean and efficient way to move these materials over long distances without the need for manual handling. 2) Conveying Grains to Processing Lines: In some distilleries, the distillers grains are further processed into animal feed or other value-added products. Pneumatic conveying is used to transport the grains to these processing lines, ensuring that the material is delivered in a hygienic and consistent manner. 3) Handling Waste Streams: Distilleries often generate waste streams that need to be transported to disposal or recycling facilities. Pneumatic systems can handle these waste materials efficiently, reducing the environmental impact of the operation.
Conclusion: Choosing the Right Conveying Solution for Your Distillery
Efficient and clean handling of sorghum distillers grains is essential for maintaining productivity and product quality in the distillery industry. Pneumatic conveying technology offers a superior solution compared to traditional methods, providing a hygienic, high-capacity, and flexible method for material transport. Shandong HeadPowder Engineering Co., Ltd. is a trusted partner in providing customized pneumatic conveying systems that meet the specific needs of distilleries. By investing in a pneumatic conveying system from HeadPowder, distilleries can enhance their operational efficiency, reduce maintenance costs, and ensure the purity of their distillers grains. For distilleries looking to optimize their material handling processes, pneumatic conveying is a clean and effective choice that delivers long-term benefits.