

Classification and Application of Small Bean Pneumatic Conveying Systems
Small bean pneumatic conveying systems are vital components in the processing and handling of small, granular agricultural products like coffee beans, soybeans, and other similar materials. These systems leverage the power of air to transport materials, offering significant advantages over traditional mechanical conveyors. Key benefits include dust-free operation, reduced material degradation, low maintenance requirements, and the ability to handle materials in a hygienic environment. The classification and application of these systems are critical for optimizing production workflows and ensuring consistent product quality across various industries.
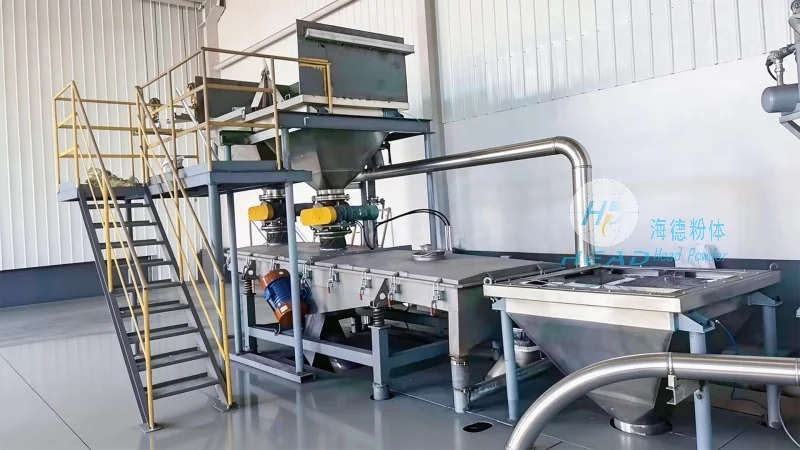
Classification of Pneumatic Conveying Systems for Small Beans
Pneumatic conveying systems for small beans are typically categorized based on the air velocity and material concentration during transport. The two primary types are dilute-phase and dense-phase systems. Dilute-phase systems operate by suspending material particles in a high-velocity air stream, usually at velocities exceeding 20 meters per second. This method is ideal for short to medium-distance transport and is commonly used for light materials that require minimal pressure. Dense-phase systems, conversely, transport material in a more concentrated form, often using lower air velocities and higher pressure to move the material in a controlled manner. This approach is suitable for longer distances and for materials that are more sensitive to handling, as it provides gentler transport conditions.
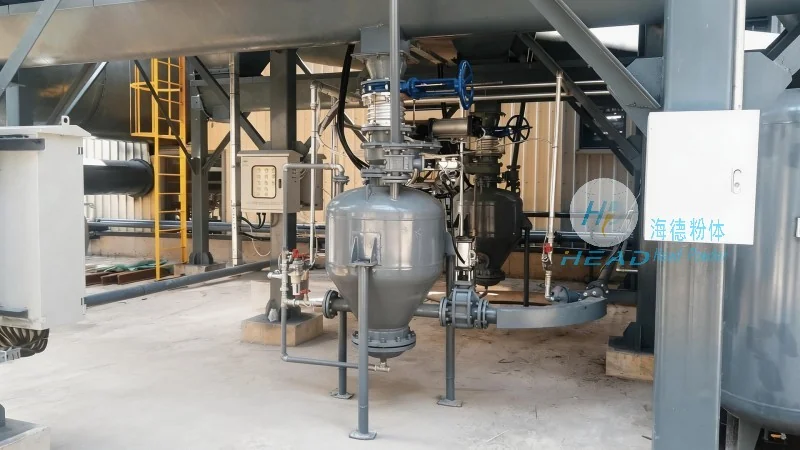
Application Analysis of Small Bean Pneumatic Conveying Systems
Small bean pneumatic conveying systems are widely utilized across multiple sectors, including food processing, agriculture, and pharmaceuticals. In the coffee industry, these systems play a crucial role in the supply chain, transporting coffee beans from storage silos to roasting facilities. The systems ensure a continuous flow of raw materials while minimizing exposure to air and moisture, which helps preserve the beans' flavor and aroma. Similarly, in the food processing sector, these systems are employed to move soybeans, chickpeas, and other legumes from processing lines to packaging areas. The gentle handling provided by pneumatic conveyors helps maintain the nutritional value and texture of the products, which is essential for consumer acceptance. In the pharmaceutical and chemical industries, these systems are used to transport small, fine particles that require sterile and controlled environments. The ability to operate in a dust-free manner makes them suitable for applications where contamination control is paramount, ensuring product safety and compliance with regulatory standards.
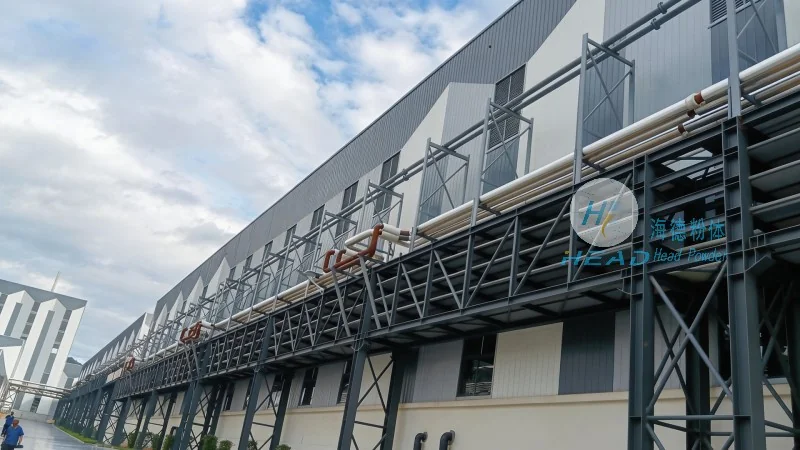
Advantages of Small Bean Pneumatic Conveying Systems
Compared to traditional mechanical conveyors, small bean pneumatic conveying systems offer several distinct advantages. One of the most significant benefits is the elimination of dust and debris, which not only improves workplace safety but also reduces the risk of product contamination. The systems also provide a more hygienic environment, which is particularly important in food and pharmaceutical applications where cleanliness is a top priority. Additionally, pneumatic conveyors can handle a wide range of materials, from light to heavy, and can transport materials over longer distances without the need for multiple transfer points. This reduces the overall footprint of the production facility and improves operational efficiency. Another advantage is the low maintenance requirement, as there are fewer moving parts compared to mechanical systems, leading to lower downtime and maintenance costs over the system's lifespan.
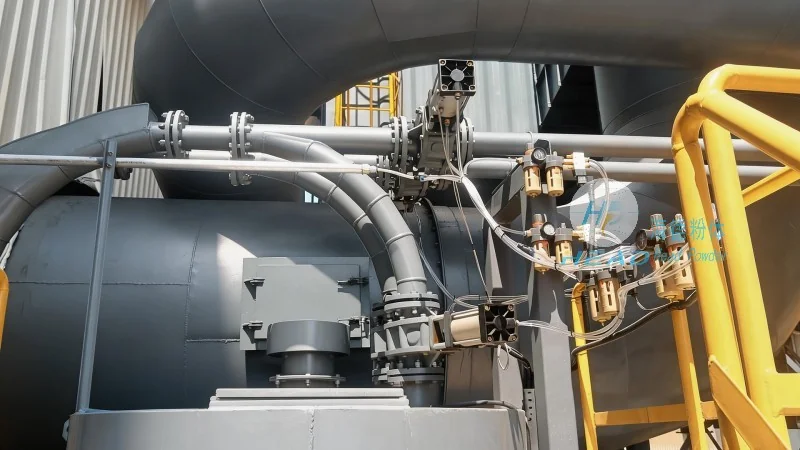
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., branded as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. The company specializes in designing and manufacturing customized solutions tailored to the specific needs of clients in various industries. With a strong commitment to innovation and quality, headpowder has established itself as a trusted partner in the market, providing reliable and efficient systems that meet the highest standards. The company's headquarters is located in Shandong, China, where it continues to develop advanced technologies and refine its products to meet the evolving demands of the industry. Headpowder's systems are known for their durability, energy efficiency, and user-friendly design, making them suitable for both small-scale and large-scale production operations.