

Gravity Dust Removal Pneumatic Conveying: What It Is and Its Design Principles
Gravity dust removal pneumatic conveying is a specialized method used in industrial processes to transport fine powders or dust particles through a pipeline using air as the conveying medium. This technology is particularly effective for handling materials that are prone to caking, agglomeration, or are sensitive to mechanical stress, making it a preferred choice in various sectors such as pharmaceuticals, food processing, and chemical manufacturing. The core of this system lies in the efficient separation of dust from the conveying air and the controlled movement of the material through the pipeline, which are both critical aspects of its design and operation.
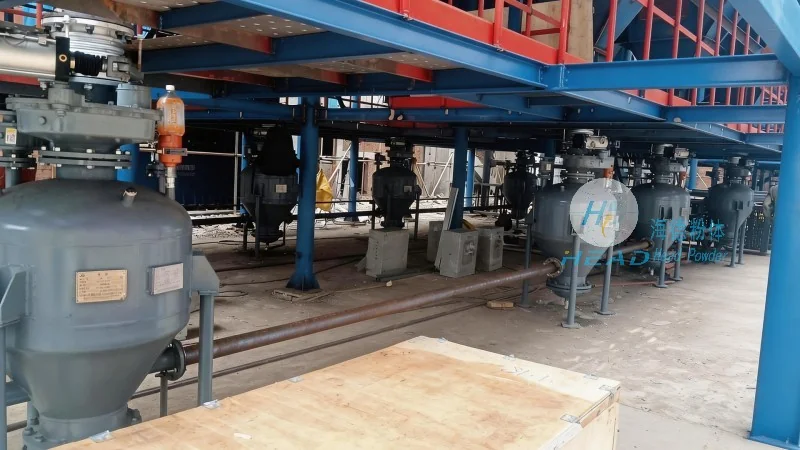
Understanding the Core Components of Gravity Dust Removal Pneumatic Conveying Systems
The gravity dust removal pneumatic conveying system typically consists of several key components that work in tandem to achieve effective material transport. At the heart of the system is the dust separator, which is designed to capture and remove fine particles from the conveying air before it is released back into the environment or recirculated. This separator often employs gravity settling chambers or cyclone separators to ensure that the air is clean and free from particulate matter, thereby preventing contamination and ensuring compliance with environmental regulations. The material feed hopper is another crucial component, as it stores the bulk material and feeds it into the conveying line at a controlled rate. The hopper is usually equipped with a feeder, such as a rotary valve or a screw feeder, which regulates the flow of material into the pipeline. The pipeline itself is constructed from materials that are resistant to corrosion and wear, such as stainless steel or plastic, to ensure durability and maintain the quality of the conveyed material. Additionally, the system may include a pressure regulator and a filter to maintain consistent air pressure and ensure that the air remains clean throughout the conveying process.
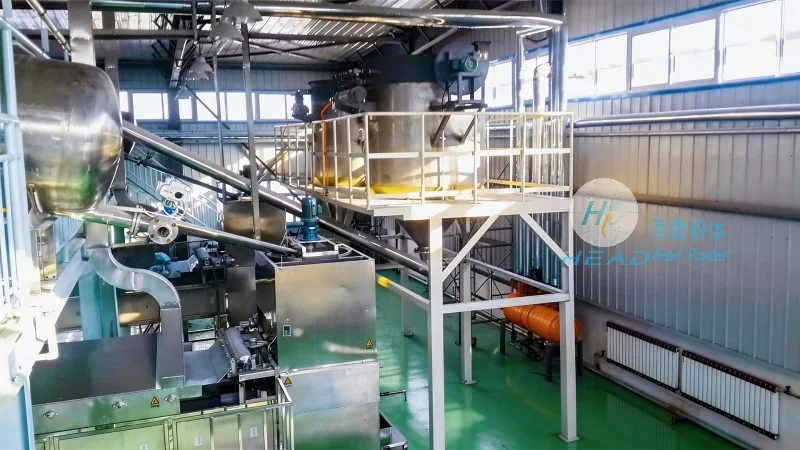
Design Principles Behind Gravity Dust Removal Pneumatic Conveying
The design principles of gravity dust removal pneumatic conveying are centered on balancing the forces acting on the particles and the air flow within the system. One of the primary design considerations is the velocity of the air in the pipeline, which must be sufficient to lift and transport the material but not so high as to cause excessive wear on the equipment or to generate too much dust. The velocity is typically determined based on the particle size, density, and the desired conveying distance. Another critical factor is the pressure drop across the system, which is influenced by the length of the pipeline, the number of bends, and the type of fittings used. Proper design ensures that the pressure drop is minimized to maintain energy efficiency and to avoid the need for excessive air volume. The system also incorporates a dust removal mechanism, such as a cyclone or a bag filter, to capture any fine particles that may escape the primary separator. This secondary filtration is essential for maintaining air quality and preventing dust accumulation in the surrounding environment. Furthermore, the design takes into account the material's properties, such as its flowability and tendency to agglomerate, by incorporating features like vibrators or agitators in the hopper to prevent blockages and ensure smooth material flow.
Applications and Benefits of Gravity Dust Removal Pneumatic Conveying
Gravity dust removal pneumatic conveying is widely used in industries where the handling of fine powders is essential. In the pharmaceutical industry, for example, this technology is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. The system's ability to maintain a clean environment and prevent cross-contamination makes it ideal for such applications. In the food processing sector, it is used to convey ingredients like flour, sugar, and spices, where hygiene and product quality are paramount. The system's gentle handling of the material ensures that the product's integrity is preserved, and the dust removal feature prevents product contamination. In the chemical industry, it is employed to transport powders like cement, limestone, and other bulk chemicals, where the system's ability to handle abrasive materials and maintain consistent flow is crucial. The benefits of this technology include improved process efficiency, reduced labor costs, and enhanced safety by minimizing the need for manual handling of powders. Additionally, the system's ability to handle a wide range of materials and its adaptability to different process requirements make it a versatile solution for various industrial applications.
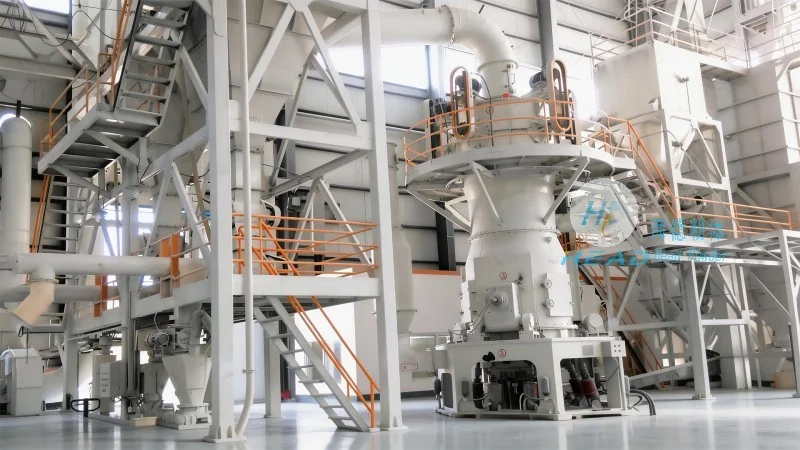
HeadPowder's Expertise in Gravity Dust Removal Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced pneumatic conveying systems, including gravity dust removal solutions. With a strong commitment to innovation and quality, HeadPowder has developed state-of-the-art systems that are tailored to meet the specific needs of its clients. The company's expertise lies in the design and manufacturing of customized conveying systems that incorporate the latest technology in dust separation and material handling. HeadPowder's team of engineers and technicians work closely with clients to understand their process requirements and provide solutions that optimize material transport while ensuring compliance with environmental and safety standards. The company's facilities in Shandong, China, are equipped with advanced manufacturing capabilities and rigorous quality control processes to ensure that each system meets the highest standards of performance and reliability. HeadPowder's products are known for their durability, efficiency, and ease of maintenance, making them a preferred choice for industries that demand high-performance conveying solutions. The company's focus on customer satisfaction and technical support ensures that clients receive not only a high-quality product but also the necessary guidance to maximize the benefits of their pneumatic conveying system.