

What is Coffee Material Handling? Understanding Its Design Principles
Coffee material handling refers to the processes and equipment used to transport, move, and manage coffee-related materials throughout the production and processing stages. This includes everything from raw coffee beans to finished coffee powders or grounds. Efficient coffee material handling is crucial for maintaining product quality, ensuring consistent processing, and optimizing operational efficiency in coffee manufacturing facilities.
Introduction to Coffee Material Handling Systems
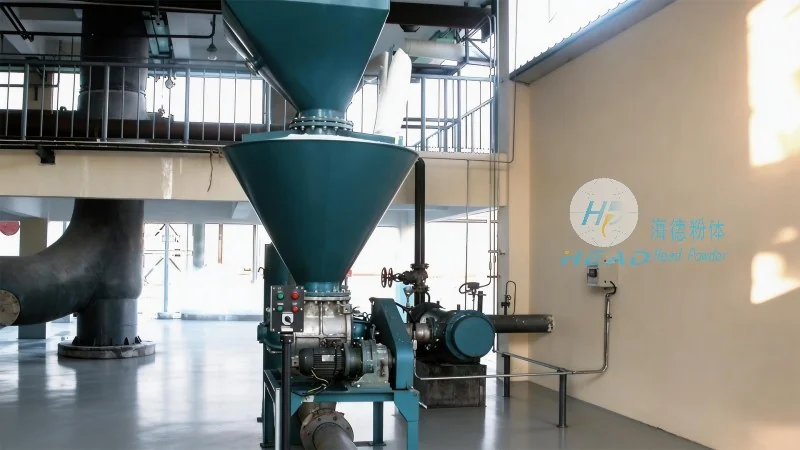
Coffee material handling systems are integral to the entire coffee production workflow. From the moment coffee beans are received at a processing plant to the final packaging of coffee powders, various equipment and techniques are employed to move these materials safely and effectively. The goal is to minimize damage to the coffee beans, maintain their quality attributes, and streamline the overall production line. This involves a combination of mechanical devices, control systems, and strategic layout planning to create a seamless material flow.
Key Components of Coffee Material Handling
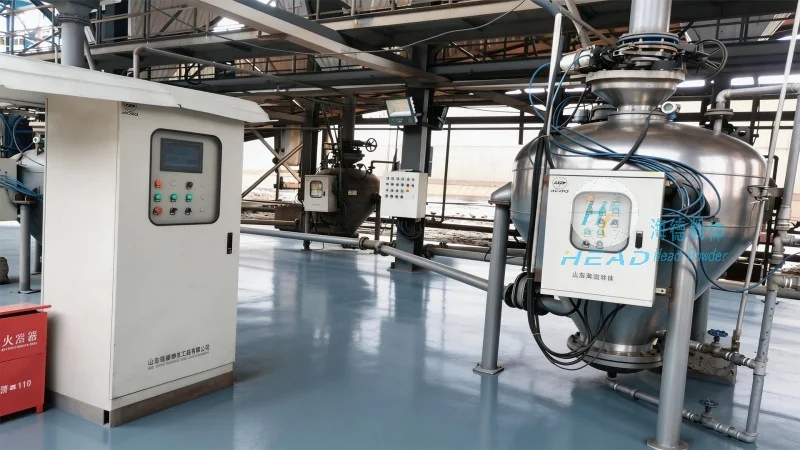
The core components of a coffee material handling system typically include conveyor belts, elevators, vibrating feeders, and sorting mechanisms. Each component serves a specific purpose in the material flow. For instance, conveyor belts are used for horizontal or slight incline movement of coffee beans or powders, while elevators lift materials vertically to different levels of the processing facility. Vibrating feeders ensure uniform material distribution, preventing blockages and ensuring consistent feeding rates to downstream equipment. Sorting mechanisms, such as air classifiers or optical sorters, may be integrated to separate different grades or types of coffee beans based on size, color, or density.
Design Principles for Efficient Coffee Material Handling
The design of coffee material handling systems follows several key principles to ensure optimal performance. First, the system must be tailored to the specific characteristics of the coffee materials being handled. Coffee beans vary in size, shape, and density, and the equipment must be able to accommodate these variations without causing damage. Second, the design prioritizes minimal product degradation. Coffee beans are sensitive to mechanical stress, temperature changes, and moisture, so the equipment is designed to handle them gently. This includes using smooth surfaces, low friction components, and controlled speed settings. Third, the system is optimized for high throughput and reliability. The layout is designed to minimize material handling time and reduce the risk of bottlenecks, ensuring that the production line operates continuously without interruptions. Additionally, the design considers ease of maintenance and cleaning, as coffee processing equipment must meet strict hygiene standards.
HeadPowder's Expertise in Coffee Material Handling Solutions
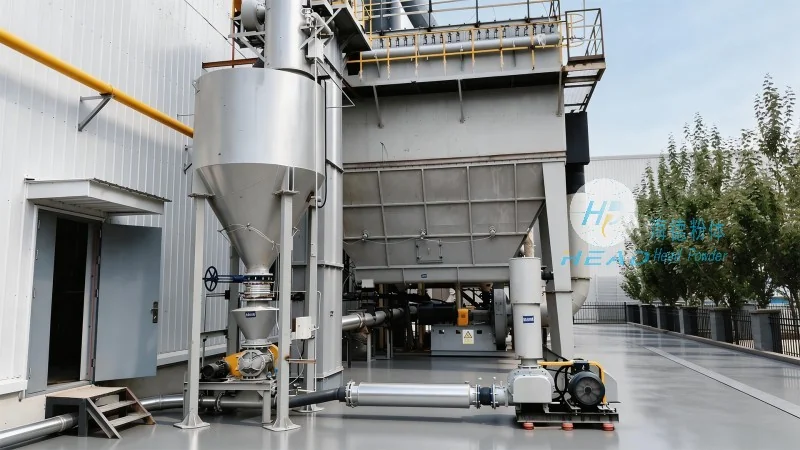
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized coffee material handling solutions. With a focus on engineering excellence and customer-centric design, HeadPowder develops and manufactures custom equipment tailored to the unique needs of coffee manufacturers. The company’s headquarters is located in Shandong, China, where it leverages advanced technology and industry expertise to deliver high-quality solutions. HeadPowder’s team of engineers works closely with clients to understand their production requirements, material characteristics, and operational constraints, then designs and implements efficient material handling systems that adhere to the principles of gentle handling, minimal degradation, and optimized throughput. By integrating cutting-edge design and robust construction, HeadPowder ensures that coffee material handling systems not only meet but exceed industry standards, supporting the long-term success of coffee production facilities worldwide.