

What is a dust-free powder pneumatic conveying system? What are its design principles?
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier based in Shandong, China, specializing in the design, development, and production of advanced dust-free powder pneumatic conveying systems. The company has been committed to providing high-quality solutions for various industries that require efficient and clean powder handling.
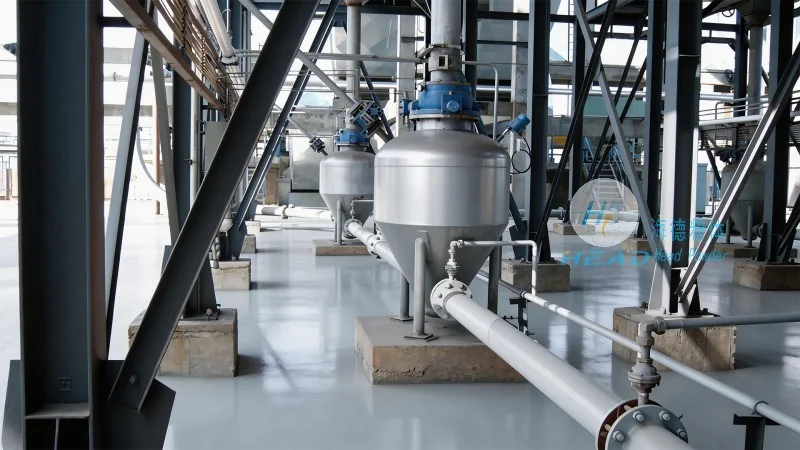
Understanding Dust-Free Powder Pneumatic Conveying Systems
A dust-free powder pneumatic conveying system is a sophisticated technology used to transport dry powders and granules through a closed pipeline using compressed air or other gas as the conveying medium. Unlike traditional methods like bucket elevators or belt conveyors, this system ensures that the powder remains completely enclosed, preventing dust emissions and maintaining a clean working environment. This is particularly crucial in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and worker safety are paramount.
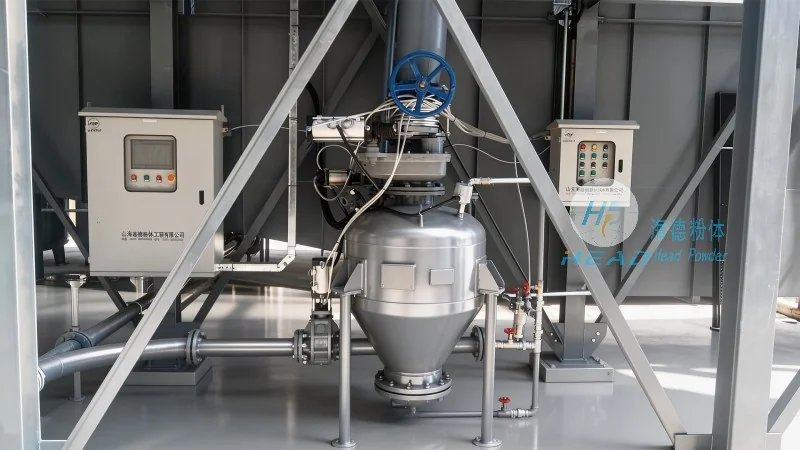
Design Principles Behind the Systems
The core design principle of a dust-free pneumatic conveying system is to create a sealed environment that isolates the powder from the external atmosphere. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line with appropriate fittings and valves, and a receiver for the discharged material. The air is introduced into the system at a controlled pressure and velocity, which lifts and transports the powder particles through the pipeline. The design must consider factors like particle size, density, and moisture content to ensure optimal conveying efficiency and minimal pressure drop. Additionally, the system incorporates filtration and dust collection mechanisms to maintain the purity of the conveyed material and protect the environment.
Advantages of Dust-Free Pneumatic Conveying Systems
One of the key advantages of a dust-free pneumatic conveying system is its ability to maintain a clean and safe working environment. By keeping the powder enclosed, it prevents dust from contaminating the workspace or being inhaled by workers, thus reducing health risks and improving overall safety. Another advantage is the high efficiency in material transport, as the system can handle large volumes of powder with minimal energy consumption compared to other methods. The enclosed design also helps in maintaining the quality of the powder, as it is not exposed to air, moisture, or contaminants that could affect its properties. Furthermore, the system is flexible and can be easily integrated into existing production lines, allowing for seamless operation and minimal downtime.
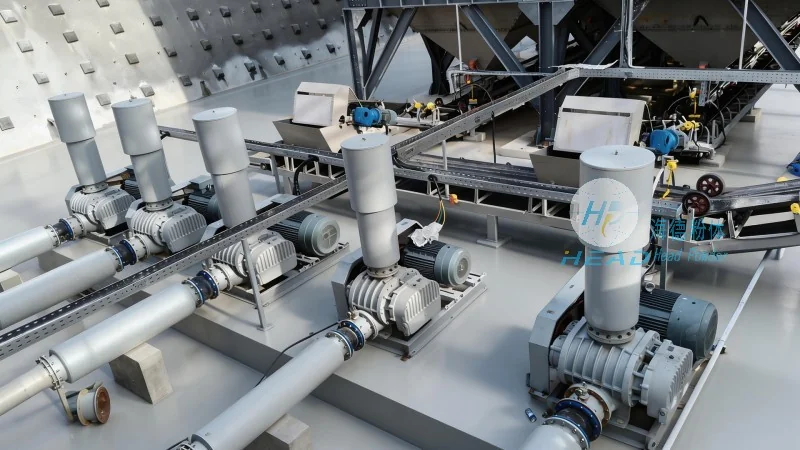
Conclusion: Reliable and Efficient Solutions from HeadPowder
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive solutions for dust-free powder pneumatic conveying systems, combining advanced technology with expert engineering. With a focus on quality and customer satisfaction, the company provides tailored systems that meet the specific needs of various industries. By leveraging their experience and expertise, HeadPowder ensures that clients receive reliable and efficient solutions that enhance productivity while maintaining the highest standards of safety and environmental compliance.