

Working Principle and Features of the Aluminum Sulfate Pneumatic Conveyor
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying systems for various industrial applications. This article delves into the working principle and key features of the aluminum sulfate pneumatic conveyor, a critical equipment for efficient material handling in chemical processing industries.
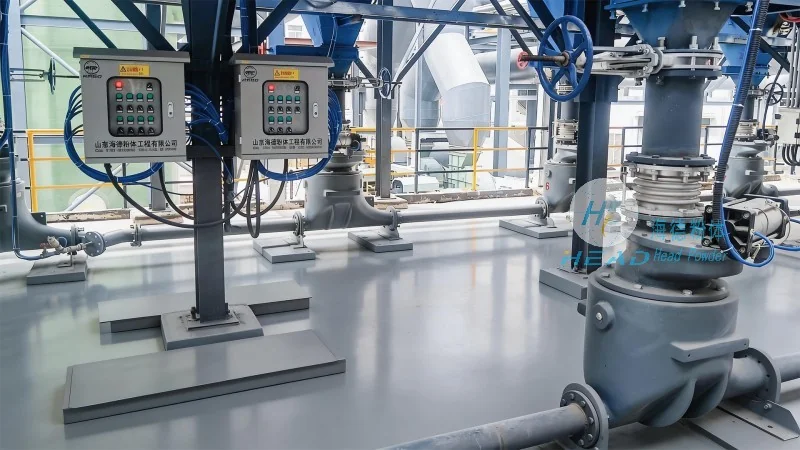
Introduction to Aluminum Sulfate Pneumatic Conveying Systems
Aluminum sulfate, also known as alum, is a widely used chemical in water treatment, paper manufacturing, and other industrial processes. The efficient transportation of this powder from storage to processing units is essential for maintaining production efficiency and minimizing downtime. The aluminum sulfate pneumatic conveyor addresses these needs by utilizing air pressure to move the material through a pipeline system, offering a dust-free and automated solution.
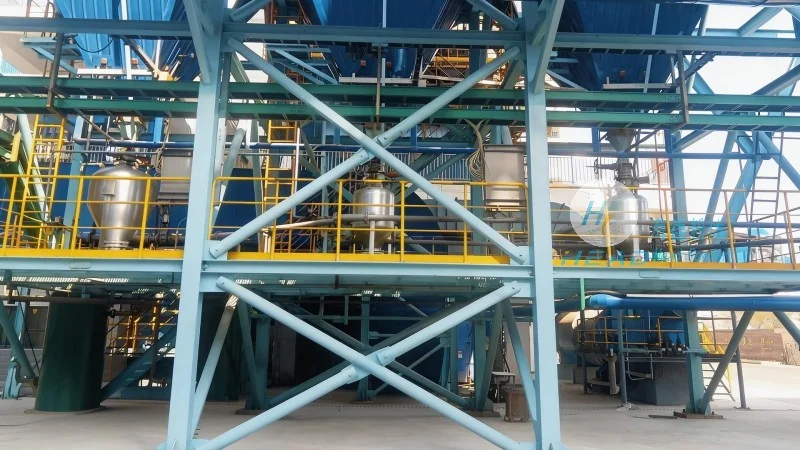
Working Principle of the Aluminum Sulfate Pneumatic Conveyor
The core of the aluminum sulfate pneumatic conveyor lies in its pneumatic conveying mechanism. The system operates by generating a flow of air within a closed pipeline network. At the feeding point, the aluminum sulfate powder is introduced into the pipeline, where it is entrained by the high-velocity air stream. This air-powder mixture travels through the pipeline to the discharge point, where the air is separated from the powder, and the powder is collected in the receiving hopper. The air, now clean, is either vented to the atmosphere or recirculated back into the system, depending on the design. The entire process is controlled by a series of valves, regulators, and sensors that ensure consistent flow rates and prevent blockages or overloading.
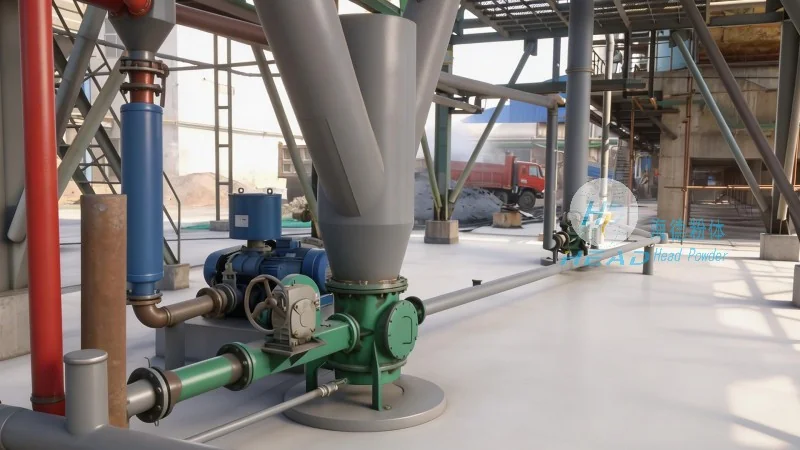
Key Features of the Aluminum Sulfate Pneumatic Conveyor
The aluminum sulfate pneumatic conveyor from HeadPowder Engineering Co., Ltd. is designed with several features that enhance its performance and reliability. Firstly, the system is equipped with a robust material handling capability, capable of transporting aluminum sulfate at high flow rates while maintaining low pressure differentials. This ensures that the conveyor can handle large volumes of material without excessive energy consumption. Secondly, the design incorporates dust suppression mechanisms, such as cyclone separators and filtration systems, to minimize airborne dust and comply with environmental regulations. Thirdly, the conveyor is built with corrosion-resistant materials, such as stainless steel, to withstand the acidic nature of aluminum sulfate and prevent material degradation over time. Additionally, the system includes automated control features, including pressure sensors and flow meters, that allow for real-time monitoring and adjustment of the conveying process, ensuring optimal operation and preventing system failures.
Advantages of Using the Aluminum Sulfate Pneumatic Conveyor
Implementing the aluminum sulfate pneumatic conveyor offers several advantages over traditional material handling methods. The primary benefit is the elimination of manual handling, which reduces labor costs and improves workplace safety. The automated system also minimizes the risk of material contamination, as the powder is kept in a closed environment throughout the conveying process. Furthermore, the conveyor’s ability to handle large volumes of material efficiently reduces production bottlenecks and increases overall throughput. The system’s compact design also saves space in industrial facilities, making it suitable for both new installations and retrofitting existing plants. Finally, the low maintenance requirements of the pneumatic conveyor, due to its simple mechanical components, result in lower operational costs and extended equipment lifespan.
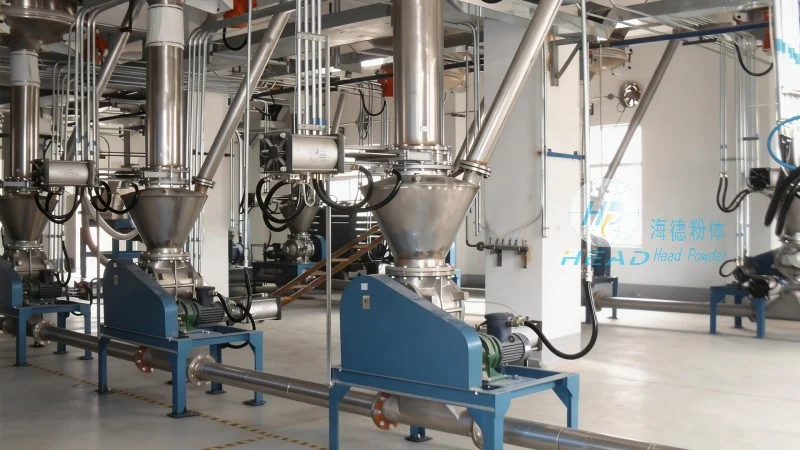
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides high-quality aluminum sulfate pneumatic conveyors that combine advanced technology with reliable performance. The working principle, which relies on air pressure to transport the material, and the key features, including dust suppression, corrosion resistance, and automated controls, make this equipment an ideal solution for industrial applications. By choosing the aluminum sulfate pneumatic conveyor from HeadPowder, businesses can enhance their material handling efficiency, reduce operational costs, and ensure compliance with environmental and safety standards.