This article provides an overview of the intelligent centralized pneumatic conveying system equipment, focusing on its working principle and key features. The system is designed to efficiently transport bulk materials through a network of pipes using compressed air, offering a flexible and automated solution for material handling in various industrial applications.
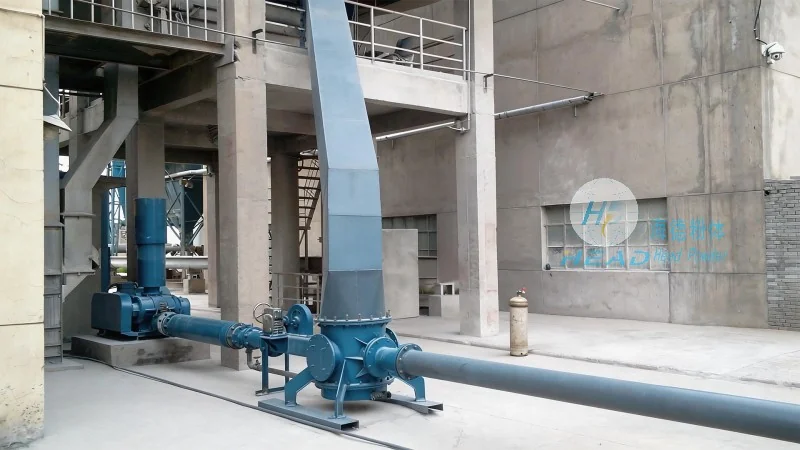
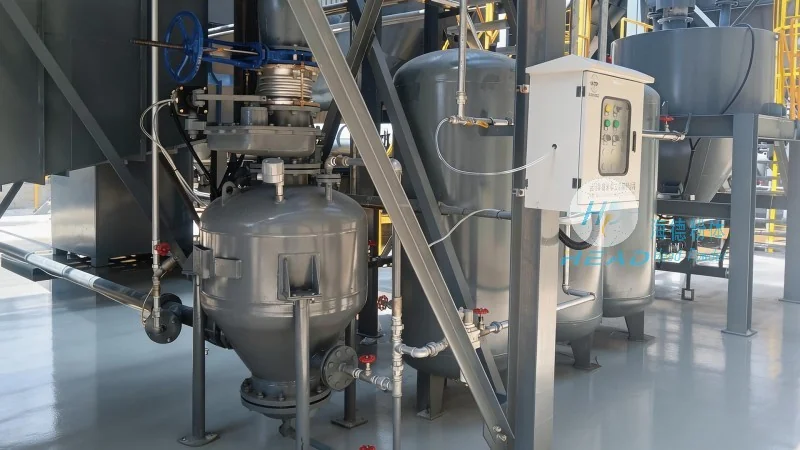
The intelligent centralized pneumatic conveying system operates on the principle of air pressure to move materials from a source to a destination. At its core, the system utilizes a combination of positive and negative pressure zones to control the flow of material. The process begins with the material being loaded into a hopper or feeder, where it is then drawn into the conveying line by a vacuum or pressure differential. Compressed air is introduced at specific points along the line to propel the material forward, ensuring consistent and reliable transport. The system incorporates advanced control technology, allowing for real-time monitoring and adjustment of the conveying parameters to optimize performance and minimize downtime.
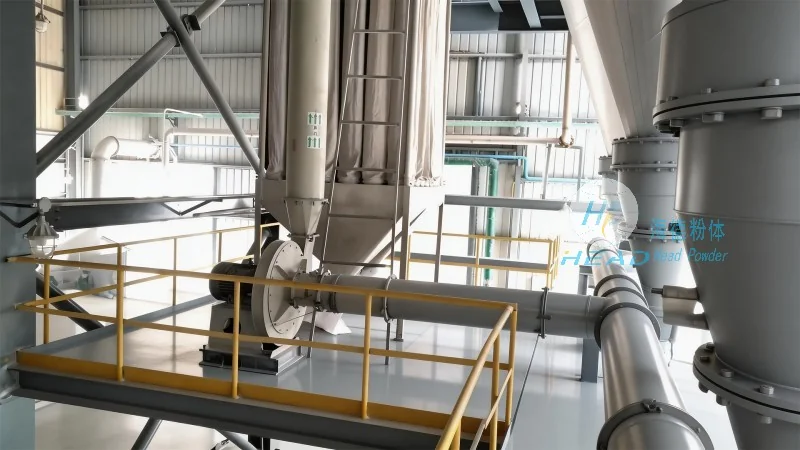
The intelligent centralized pneumatic conveying system is equipped with several advanced features that enhance its functionality and efficiency. One of the primary features is the centralized control system, which allows operators to manage multiple conveying lines from a single interface. This centralized control enables seamless coordination of material flow, ensuring that different materials are conveyed to their respective destinations without cross-contamination. Additionally, the system incorporates sensors and feedback mechanisms that continuously monitor the pressure, flow rate, and material level, providing real-time data for process optimization. The system also features automatic cleaning and maintenance routines, reducing the need for manual intervention and extending the equipment's lifespan. Another notable feature is the modular design, which allows for easy expansion or modification of the system to accommodate changing production needs. The intelligent control system further enhances operational efficiency by implementing predictive maintenance algorithms, alerting operators to potential issues before they lead to system failures.
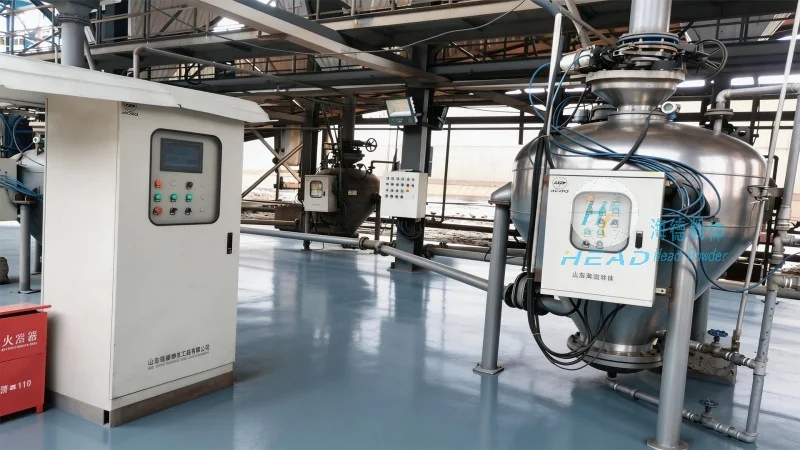
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling solutions. With a strong focus on innovation and quality, the company specializes in the design, development, and production of intelligent centralized pneumatic conveying systems. Headpowder's products are widely used in industries such as food, pharmaceuticals, chemicals, and minerals, where precise and hygienic material transport is critical. The company is committed to providing customized solutions tailored to the specific needs of each client, ensuring that the systems are optimized for their unique operational requirements. Headpowder's headquarters is located in Shandong, China, where the company maintains state-of-the-art manufacturing facilities and a dedicated research and development team. The company adheres to international quality standards and continuously invests in technology to stay at the forefront of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top