Automatic bulk material pneumatic conveying systems represent a sophisticated solution for the efficient handling and transportation of dry bulk materials in industrial settings. These systems are designed to automate the process of material feeding, conveying, and distribution, ensuring precise control over the entire operation. The core of such systems lies in the pneumatic conveying technology, which utilizes compressed air or other gases to move materials through a network of pipes and components.
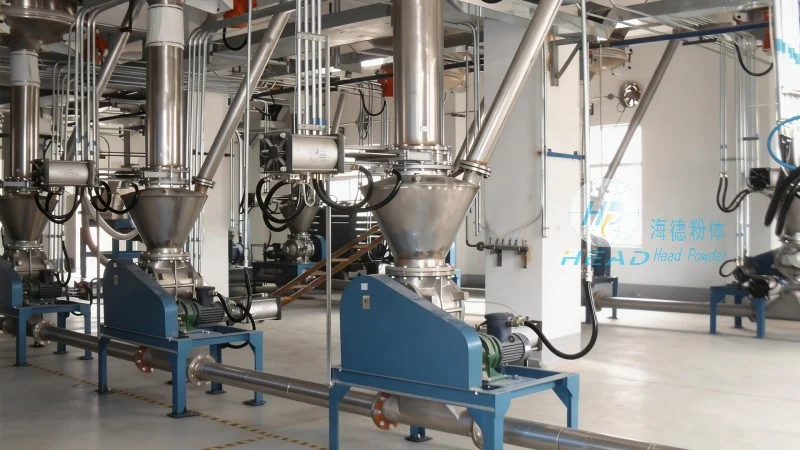
The fundamental working principle of an automatic bulk material pneumatic conveying system involves the creation of a pressure differential within a closed system. Compressed air is introduced into the material hopper or feeder, where it lifts and propels the bulk material into the conveying pipeline. The system typically includes a series of components such as a feeder, a pressure vessel, a filter, and a receiver. The feeder ensures a consistent flow of material, while the pressure vessel maintains the necessary air pressure. As the material is conveyed through the pipeline, it is separated from the air by a filter, and the cleaned air is then discharged. The material is collected in the receiver, ready for subsequent processing or use. This process eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational reliability.
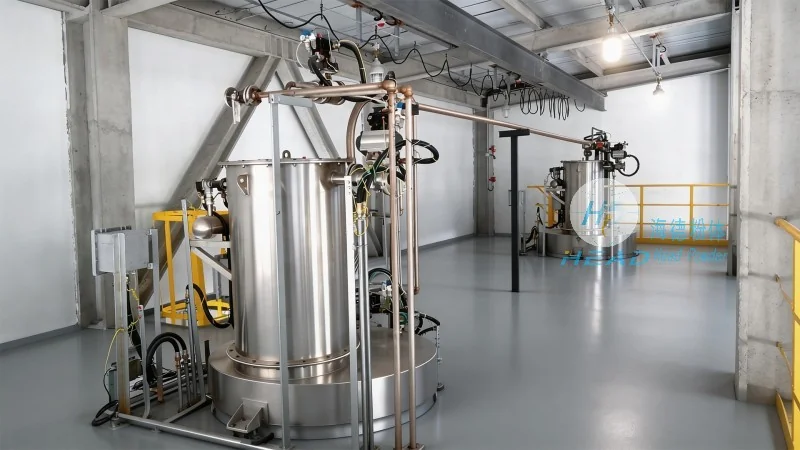
Automatic bulk material pneumatic conveying systems offer several distinct advantages that make them ideal for various industrial applications. One of the primary features is their high efficiency in material handling. By using compressed air, these systems can transport materials over long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. The systems are also highly flexible, allowing for easy integration into existing production lines and the ability to change the conveying route as needed. Another significant feature is their ability to maintain a consistent material flow rate, which is crucial for processes that require precise control over the amount of material being processed. This consistency helps in reducing waste and improving product quality. Additionally, these systems are designed with safety in mind, featuring enclosed pipelines that prevent dust emissions and protect operators from hazardous materials. The automated nature of the system reduces the need for manual intervention, minimizing the risk of human error and enhancing overall operational safety. Environmental considerations are also addressed, as the systems are equipped with filters that capture dust particles, ensuring compliance with environmental regulations and promoting a cleaner working environment.
Automatic bulk material pneumatic conveying systems are widely used in industries such as food processing, pharmaceuticals, chemicals, and mining. In the food industry, for example, these systems are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and dust-free handling. In pharmaceutical manufacturing, the systems are critical for conveying raw materials and finished products, maintaining strict contamination control. The chemical industry benefits from the systems' ability to handle abrasive and corrosive materials without damage to the equipment. The mining sector uses pneumatic conveying for transporting ores and minerals from processing plants to storage facilities. The benefits of these systems extend beyond efficiency and safety; they also contribute to cost savings by reducing labor costs and minimizing material loss due to spillage or degradation. The automated nature of the system allows for continuous operation, increasing production throughput and improving overall productivity.
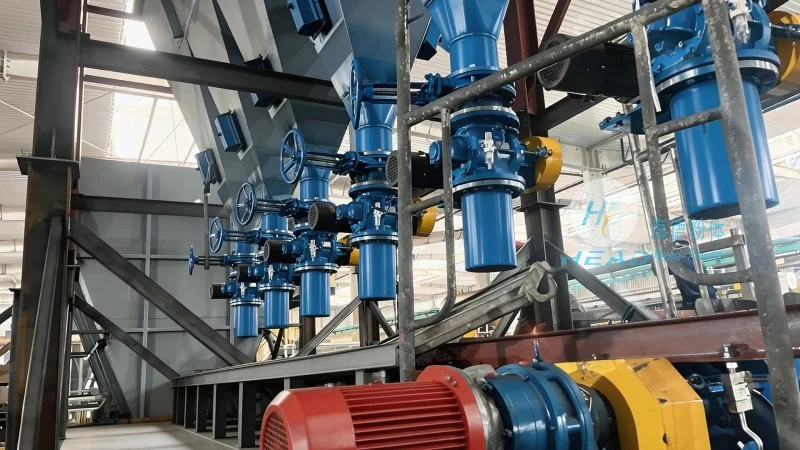
HeadPowder, a leading manufacturer of bulk material handling equipment, offers customized automatic pneumatic conveying systems tailored to the specific needs of each client. The company, based in Shandong, China, understands that each industrial application has unique requirements, and thus provides flexible solutions that can be adapted to different material types, conveying distances, and production volumes. The systems can be integrated with existing production lines or designed as standalone units, depending on the client's requirements. HeadPowder's expertise lies in the design and manufacturing of high-quality components, including feeders, filters, and receivers, ensuring durability and long-term performance. The company's commitment to quality is evident in its adherence to international standards and rigorous testing procedures for all products. Clients can rely on HeadPowder's technical support team for installation, commissioning, and ongoing maintenance services, ensuring that the systems operate at optimal efficiency throughout their service life.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top