When it comes to handling dry powders and bulk materials efficiently, the choice of equipment plays a crucial role in ensuring smooth operations and maintaining product integrity. Dry powder conveyors are specialized machinery designed to transport powders and granular materials from one location to another with precision and reliability. In this article, we will explore the working principles and key features of these essential industrial tools, focusing on how they contribute to enhanced productivity in various applications.

The core mechanism of dry powder conveyors revolves around the principles of air flow and material suspension. These systems typically operate by creating a controlled airflow that lifts and transports the dry powder particles through a pipeline. The process begins with the material being fed into the conveyor inlet, where it is then entrained by the moving air stream. As the air flows through the system, it carries the powder particles along the designated path, ensuring consistent and uniform transport. This method, often referred to as pneumatic conveying, eliminates the need for mechanical components that might cause wear or contamination, making it ideal for sensitive materials.
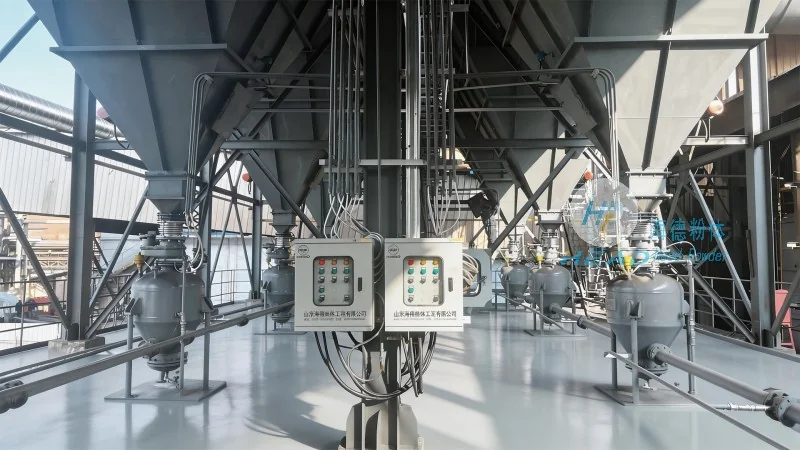
HeadPowder, a leading manufacturer based in Shandong, China, offers a range of dry powder conveyors that are designed to meet diverse industrial needs. The primary features of these systems include high efficiency in material transport, minimal product degradation, and easy maintenance. The conveyors are equipped with advanced control systems that allow for precise regulation of airflow and pressure, ensuring optimal performance under varying conditions. Additionally, the design incorporates materials that are resistant to corrosion and wear, enhancing the longevity of the equipment. The systems are also designed to be flexible, allowing for integration into existing production lines without significant modifications.
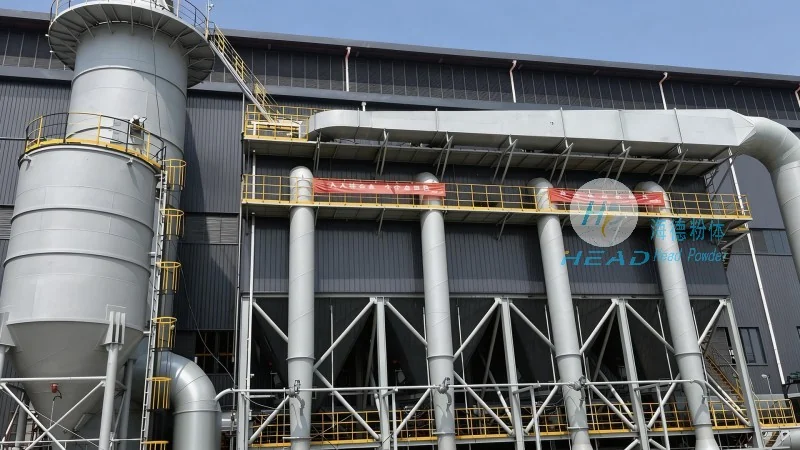
Dry powder conveyors find extensive applications in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining. The ability to handle sensitive materials without compromising their quality makes these systems invaluable in sectors where product purity is paramount. The benefits of using dry powder conveyors include reduced labor costs, improved safety by eliminating manual handling, and increased operational efficiency. By automating the material transport process, businesses can achieve higher throughput while maintaining consistent quality standards.
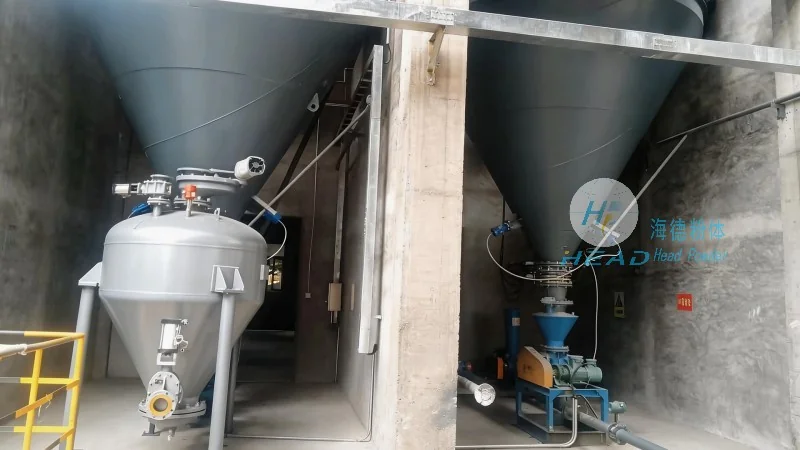
In conclusion, dry powder conveyors are essential equipment for any operation that handles dry powders and bulk materials. The working principles, which rely on pneumatic conveying, provide a reliable and efficient method for transporting materials. The features offered by manufacturers like Shandong HeadPowder Engineering Co., Ltd. ensure that these systems are robust, easy to maintain, and adaptable to various industrial requirements. Investing in high-quality dry powder conveyors can significantly enhance operational efficiency and product quality, making them a worthwhile addition to any industrial setup.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top