Glucose powder conveyors are essential equipment in the food and pharmaceutical industries, designed to efficiently transport glucose powder from one location to another. As a key component in processing facilities, these systems ensure reliable and consistent material handling, supporting production workflows with precision. The following sections delve into the working principle and key features of glucose powder conveyors, providing insights into how they operate and why they are preferred in industrial applications.
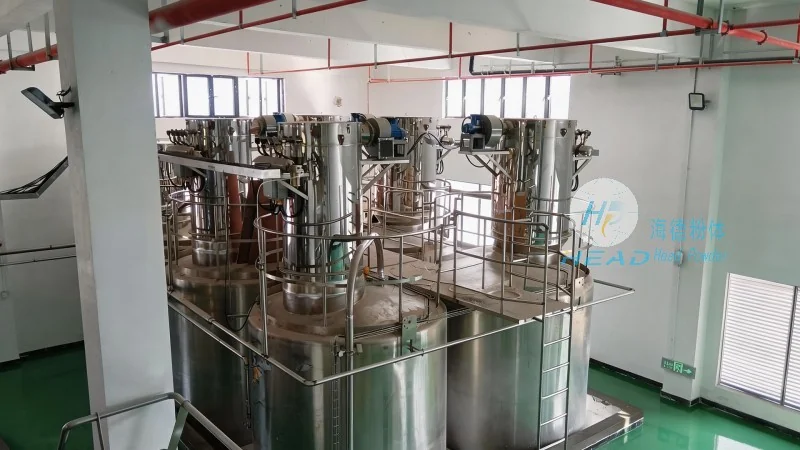
Glucose powder conveyors typically operate based on mechanical or pneumatic principles, depending on the specific design and application requirements. One common type is the screw conveyor, which utilizes a rotating helical screw to move powder through a closed tube. As the screw rotates, it pushes the glucose powder forward, leveraging the friction between the powder particles and the screw surface. This mechanism allows for gentle and continuous movement of the material, minimizing product degradation and ensuring uniform flow. Another variant may employ pneumatic conveying systems, where compressed air or gas is used to create a flow of air that carries the powder particles through a pipeline. This method is particularly effective for handling fine powders like glucose, as it reduces the risk of blockages and allows for long-distance transport with minimal energy consumption.
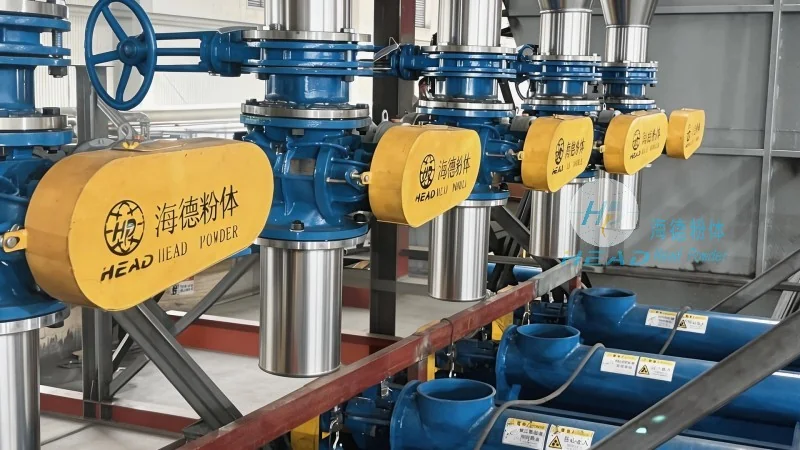
When evaluating glucose powder conveyors, several features stand out as critical for optimal performance. First, efficiency is a primary consideration, as these systems are designed to minimize energy usage while maximizing throughput. The mechanical design of screw conveyors, for instance, ensures that power is utilized effectively to move the powder, with minimal waste. Additionally, these conveyors are built to handle the unique properties of glucose powder, such as its fine particle size and potential for caking. Materials used in the construction, such as stainless steel or food-grade plastics, prevent contamination and ensure compliance with industry standards. Another notable feature is the adaptability of these systems, which can be customized to suit different production scales and operational environments. Whether for small-scale batch processing or large-scale continuous production, glucose powder conveyors can be adjusted to meet specific needs, including varying conveyor lengths, speeds, and discharge configurations.
Glucose powder conveyors find widespread use in various industries, including food processing, pharmaceutical manufacturing, and chemical production. In food processing, they are integral to the handling of glucose as an ingredient in beverages, baked goods, and other products. The gentle handling provided by these conveyors preserves the quality and flavor of the powder, ensuring that the final product meets consumer expectations. In pharmaceutical applications, the hygienic design and material choices of glucose powder conveyors are crucial, as they must adhere to strict regulatory standards for product purity and safety. The ability to maintain a clean and controlled environment reduces the risk of contamination, which is paramount in drug manufacturing. Furthermore, the consistent performance of these conveyors enhances overall production efficiency, reducing downtime and improving output quality. By integrating these systems into production lines, companies can achieve smoother workflows and better control over material movement, leading to cost savings and improved operational reliability.
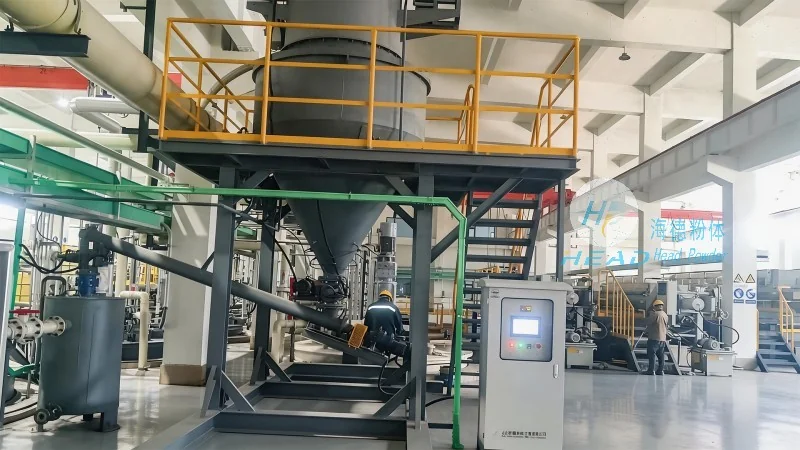
Glucose powder conveyors represent a vital technology for the efficient and reliable handling of glucose powder in industrial settings. Their working principles, which may involve mechanical or pneumatic mechanisms, are tailored to the specific characteristics of the material, ensuring minimal degradation and optimal flow. The key features of these conveyors, including efficiency, adaptability, and hygienic design, make them indispensable in various applications. As a leader in powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality glucose powder conveyors that meet the demands of modern production environments. With a focus on innovation and customer satisfaction, the company delivers solutions that enhance operational performance and support long-term success in the industry. Based in Shandong, China, HeadPowder continues to advance the technology of powder conveyors, contributing to the efficiency and reliability of global production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top