Efficient and reliable transportation of soda ash powder is crucial in various industrial applications, and the soda ash powder conveying system equipment from Shandong HeadPowder Engineering Co., Ltd. offers advanced solutions tailored to meet these demands. This article explores the working principle and key features of such systems, providing insights into their operational efficiency and design advantages.
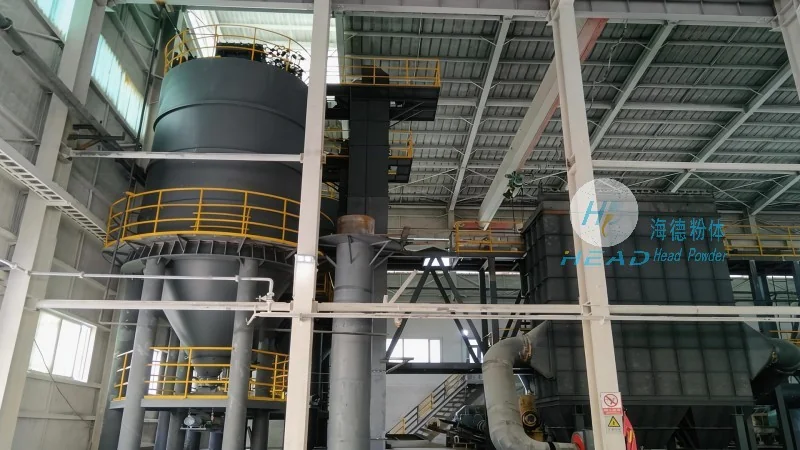
The soda ash powder conveying system typically operates on the principle of pneumatic or mechanical transport, depending on the specific requirements of the application. For pneumatic systems, the process involves the use of air pressure to move the powder through a network of pipes. A blower or compressor generates the necessary airflow, which carries the soda ash particles from the source to the destination. The system may include components such as a hopper, a feeder, and a control valve to regulate the flow rate and ensure consistent transport. Mechanical systems, on the other hand, utilize screw conveyors, belt conveyors, or bucket elevators to physically move the powder. These mechanisms rely on rotational motion to propel the material along the conveyor path, providing a reliable and low-maintenance option for certain industrial settings.
Shandong HeadPowder Engineering Co., Ltd. designs and manufactures soda ash powder conveying systems with several notable features that enhance performance and durability. One of the primary features is the robust construction, which is built to withstand the abrasive nature of soda ash powder and the demanding conditions of industrial environments. The equipment is often equipped with corrosion-resistant materials, such as stainless steel or special coatings, to prevent degradation over time and maintain long-term functionality. Additionally, the systems are designed for easy maintenance, with accessible components and modular designs that allow for quick repairs and replacements without extensive downtime.
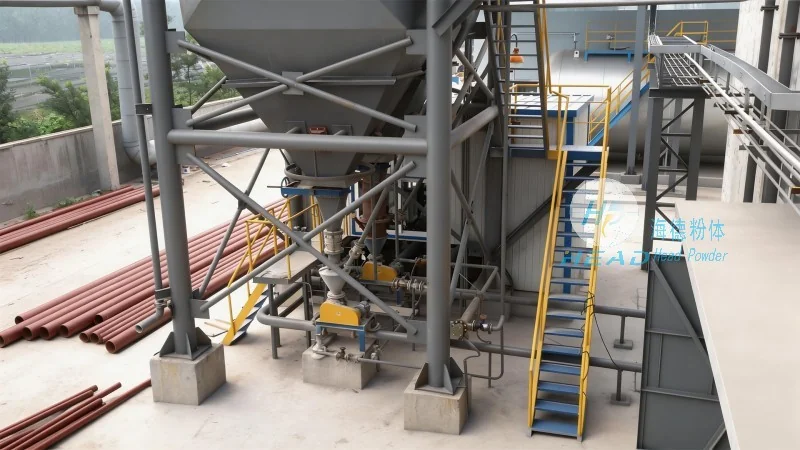
Another significant feature is the precise control capabilities of the conveying system. Advanced control systems, including variable frequency drives (VFDs) and sensors, enable operators to adjust the flow rate and pressure in real-time, ensuring optimal performance and preventing material buildup or blockages. This level of control is particularly important in applications where consistent product quality and process efficiency are critical. The systems also incorporate safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect both the equipment and personnel from potential hazards.
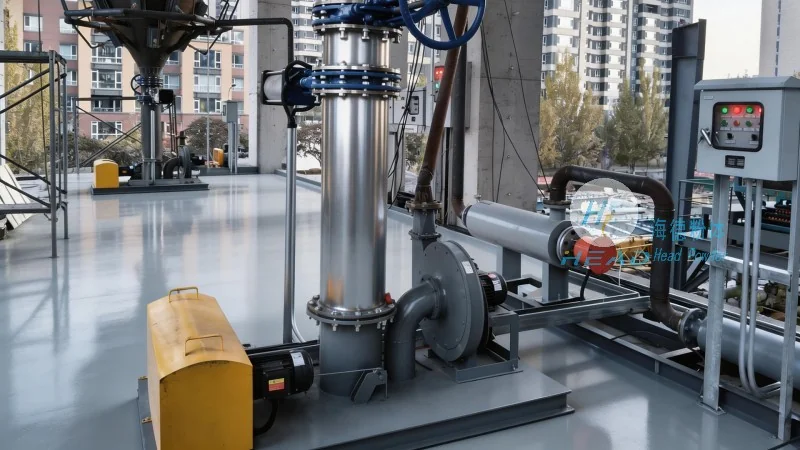
When selecting a soda ash powder conveying system, partnering with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. offers several advantages. The company has extensive experience in the industry, having developed and refined its systems to meet the specific needs of clients across various sectors, including chemical, food processing, and pharmaceutical industries. Their commitment to quality is evident in the rigorous testing and quality control processes applied to each piece of equipment, ensuring that every system meets or exceeds industry standards. Furthermore, the company provides comprehensive after-sales support, including installation, training, and maintenance services, to help clients maximize the lifespan and efficiency of their conveying systems.
Shandong HeadPowder Engineering Co., Ltd. is dedicated to delivering reliable and efficient soda ash powder conveying solutions that enhance operational productivity while minimizing downtime and maintenance costs. By leveraging advanced technology and a deep understanding of industrial requirements, the company continues to set the benchmark for quality in the field of powder handling equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top