

Working Principle and Features of Copper Oxide Material Handling
When it comes to the efficient and safe transportation of copper oxide materials, understanding the underlying working principles and distinctive features of the handling systems is crucial. This article provides a detailed exploration of how copper oxide material handling operates, highlighting key aspects that make it a reliable solution for industrial applications.

Working Principle of Copper Oxide Material Handling Systems
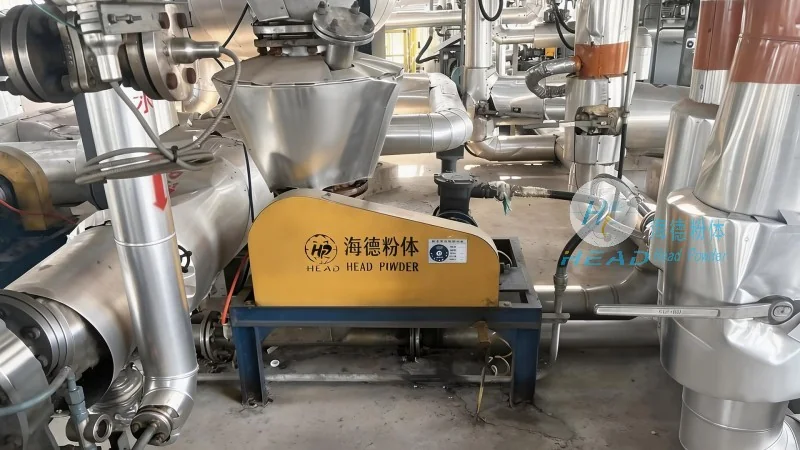
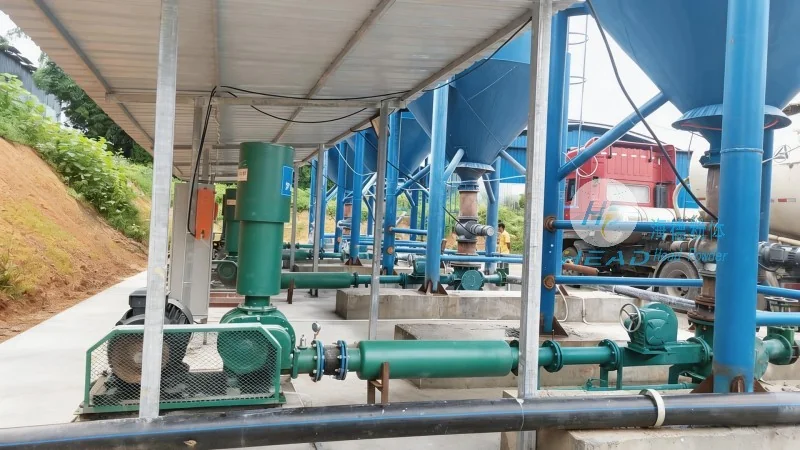
The working principle of copper oxide material handling systems typically revolves around specialized equipment designed to handle the unique properties of copper oxide. These systems often incorporate mechanisms such as conveyor belts, screw conveyors, or pneumatic transport systems, tailored to the physical characteristics of copper oxide, including its density, particle size, and potential reactivity. The process generally begins with the loading of copper oxide into a hopper or storage silo, where it is then transferred to the primary conveyor system. From there, the material moves through the handling infrastructure, often under controlled conditions to prevent dust generation or oxidation. The system may include components like feeders, chutes, and control valves to regulate the flow rate and direction of the copper oxide, ensuring a smooth and continuous operation. Advanced systems may also incorporate sensors and automation controls to monitor the material level, flow rate, and any potential blockages, enhancing operational efficiency and safety.
Key Features of Copper Oxide Material Handling Solutions
Effective copper oxide material handling solutions exhibit several notable features that contribute to their performance and reliability. One of the primary features is the ability to handle the material in a dust-free environment, which is essential for maintaining product quality and worker safety. This is often achieved through enclosed conveyor systems and dust suppression mechanisms, such as air filtration or water spray systems. Another critical feature is the system's adaptability to varying particle sizes and bulk densities of copper oxide, allowing it to accommodate different grades or forms of the material. The equipment is designed to minimize material degradation, ensuring that the copper oxide retains its intended properties throughout the handling process. Additionally, modern copper oxide handling systems prioritize energy efficiency, with optimized motor controls and reduced friction in moving parts, leading to lower operational costs. Safety features, including emergency stop buttons, overload protection, and material containment measures, are also integral to these systems, providing a secure working environment for operators. The integration of automation and real-time monitoring further enhances the system's performance, enabling predictive maintenance and quick response to operational issues.

Applications and Benefits in Industrial Settings
Copper oxide material handling systems find widespread application in various industrial sectors, including mining, chemical processing, and manufacturing. In mining operations, these systems are used to transport copper oxide from ore processing facilities to storage or processing units, ensuring a continuous supply of raw material. In chemical plants, they facilitate the handling of copper oxide during the production of copper compounds, such as copper sulfate or copper chloride, where precise material control is vital for product consistency. The benefits of using specialized copper oxide handling solutions extend beyond efficiency and safety; they also contribute to cost savings by reducing material loss, minimizing downtime due to equipment failure, and improving overall production throughput. The reliability of these systems, coupled with their ability to handle the challenging properties of copper oxide, makes them an indispensable part of modern industrial operations.
Conclusion and Company Overview
In conclusion, copper oxide material handling systems are sophisticated solutions that combine advanced engineering with practical design to address the unique challenges of transporting copper oxide. By understanding the working principles and key features of these systems, industries can optimize their material handling processes, enhance operational efficiency, and ensure a safe working environment. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and implementing customized copper oxide handling solutions tailored to the specific needs of clients. With a focus on innovation, quality, and customer satisfaction, HeadPowder delivers systems that meet the highest standards of performance and reliability, supporting the success of industrial operations worldwide.