

Working Principle and Features of Activated Carbon Material Handling Systems
Activated carbon material handling systems are essential components in industrial processes, particularly in applications involving the transportation and management of activated carbon. These systems are designed to ensure efficient and reliable movement of the material, which is crucial for maintaining optimal performance in various industrial operations. The following sections will delve into the working principles and key features of such systems, providing a comprehensive understanding of their functionality and benefits.
Working Principle of Activated Carbon Material Handling Systems
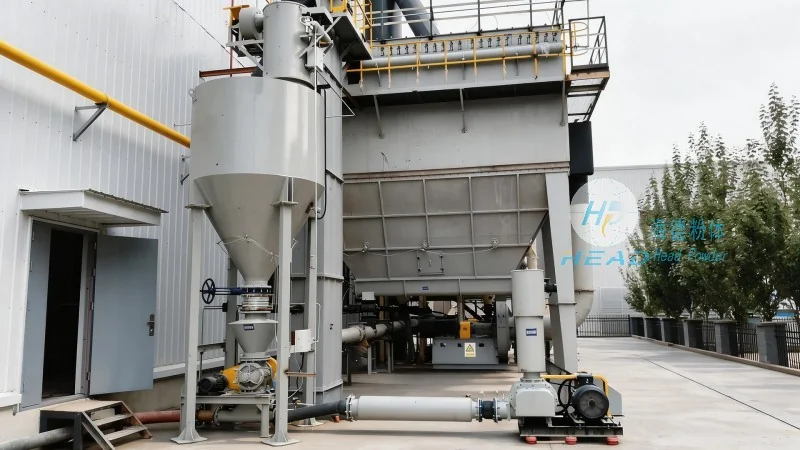
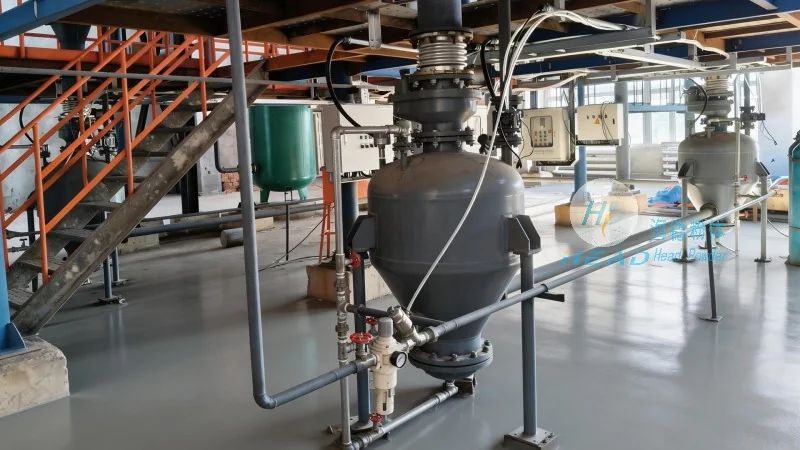
The working principle of activated carbon material handling systems typically involves several key steps to ensure the smooth and efficient transport of activated carbon. The process begins with the loading of activated carbon into a storage hopper or silo. From there, the material is transferred through a series of mechanisms, such as conveyor belts, screw conveyors, or pneumatic systems, to the desired destination. The system is equipped with sensors and control devices that monitor the flow rate and pressure, ensuring consistent and safe operation. This integrated approach allows for precise control over the material movement, minimizing the risk of blockages or spills. The design of these systems is tailored to handle the unique properties of activated carbon, including its granular structure and potential dust generation, which requires specialized equipment to manage effectively.
Key Features of Activated Carbon Material Handling Systems
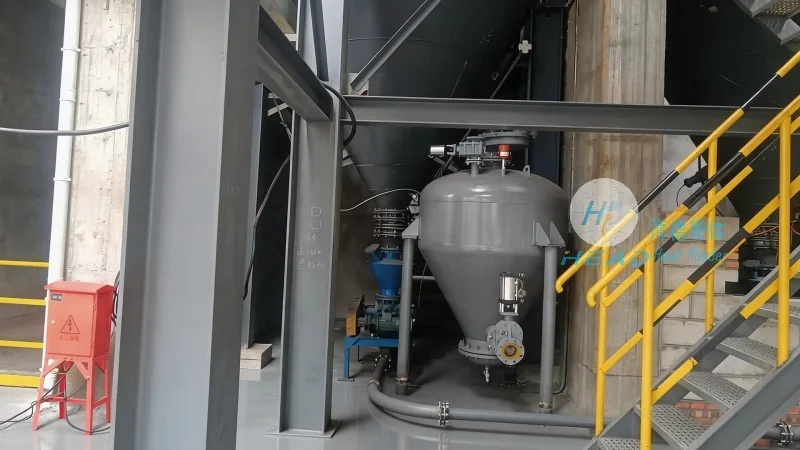
Activated carbon material handling systems are characterized by several key features that enhance their performance and reliability. One of the primary features is the use of dust control mechanisms, such as enclosed conveyor systems and dust collection units, to prevent the release of airborne particles and maintain a safe working environment. Another important feature is the integration of automated control systems, which allow for real-time monitoring and adjustment of the material flow. This automation not only improves operational efficiency but also reduces the need for manual intervention, thereby minimizing human error. Additionally, these systems are designed with durability and low maintenance in mind, utilizing high-quality materials and robust construction to withstand the demanding conditions of industrial environments. The ability to handle varying particle sizes and moisture content is also a critical feature, as activated carbon can have diverse physical properties depending on the production process. The systems are equipped with adjustable components, such as variable speed drives and adjustable hoppers, to accommodate these variations and ensure consistent performance.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
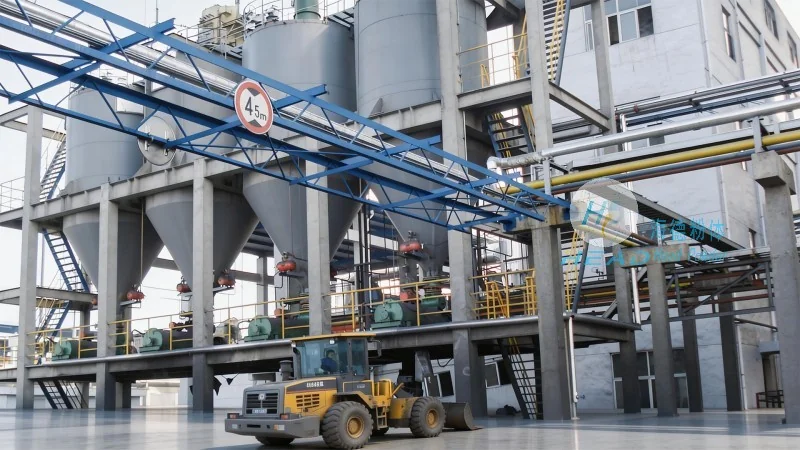
HeadPowder, a leading manufacturer in the field of material handling systems, specializes in providing customized solutions for activated carbon and other industrial materials. With a strong focus on quality and innovation, the company has established itself as a trusted partner for businesses requiring reliable and efficient material transport solutions. HeadPowder's facilities are located in Shandong, China, where the company leverages advanced technology and skilled expertise to develop and produce high-performance material handling systems. The company's commitment to customer satisfaction and product excellence is reflected in its comprehensive range of products and dedicated after-sales support. By choosing HeadPowder, clients can benefit from years of experience and a deep understanding of the industry's specific needs, ensuring that their material handling requirements are met with precision and reliability.