

Working Principle and Features of Desulfurization and Denitrification Agent Powder Pneumatic Conveyi
For industrial applications involving desulfurization and denitrification processes, the efficient handling of powder agents is critical. Pneumatic conveying systems, specifically designed for these specialized chemicals, offer a reliable solution. This article explores the working principle and key features of such equipment, highlighting how it enhances operational efficiency and safety in industrial settings.
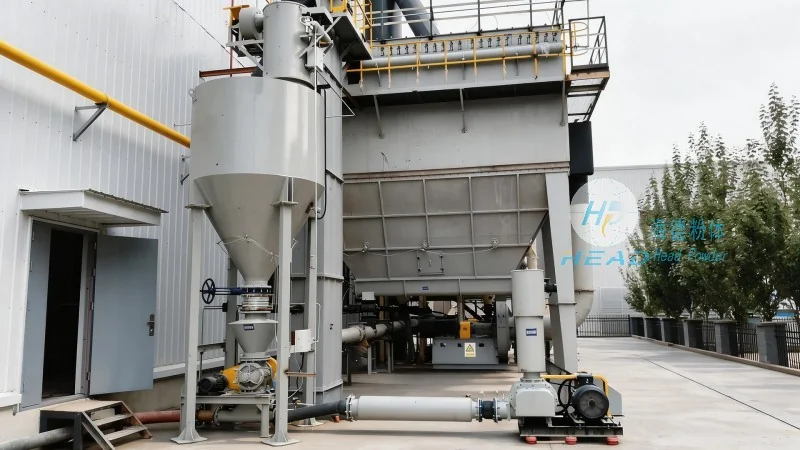
Introduction to Pneumatic Conveying Systems for Desulfurization and Denitrification Agents
Desulfurization and denitrification agents are essential components in modern industrial processes, particularly in power generation and chemical manufacturing. These powders require precise and safe handling to ensure optimal performance and environmental compliance. Pneumatic conveying equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., addresses these needs by providing a closed-loop system that minimizes dust exposure and maximizes material transport efficiency.
Working Principle of the Pneumatic Conveying Equipment
The core of the pneumatic conveying system lies in its ability to transport powder materials using compressed air. The process begins with the powder being fed into a hopper or silo. From there, the material is drawn into a pipeline by a vacuum or pressure differential created by an air compressor. The compressed air then propels the powder particles through the system, ensuring uniform flow and preventing clogging. The system typically includes components such as a blower, cyclone separator, and filter to manage air and material separation, ensuring that the powder is delivered to its destination without loss or contamination.
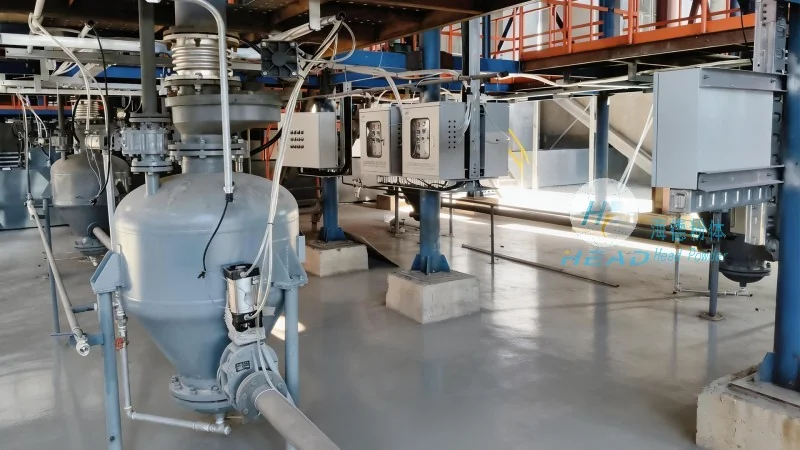
Key Features of the Equipment
Shandong HeadPowder Engineering Co., Ltd. designs pneumatic conveying systems with several distinct features that enhance performance and safety. Firstly, the equipment is constructed with high-quality materials resistant to corrosion and abrasion, which is crucial for handling corrosive desulfurization and denitrification agents. The system incorporates advanced control mechanisms that allow for precise regulation of air pressure and flow, ensuring consistent material transport rates. Additionally, the closed-loop design minimizes environmental impact by containing dust and preventing emissions, aligning with industrial safety and environmental regulations. The equipment also features easy maintenance components, such as replaceable filters and accessible piping, which reduce downtime and operational costs. Another notable feature is the integration of safety sensors that monitor system pressure and air quality, providing real-time alerts in case of anomalies and ensuring operator safety.
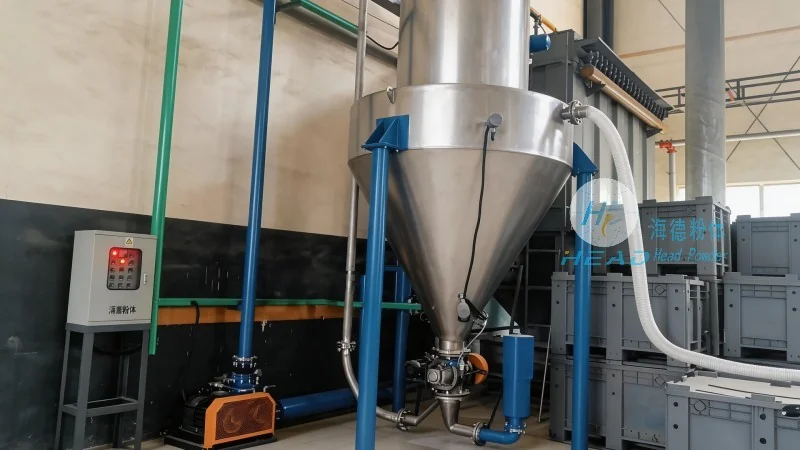
Benefits of Using Pneumatic Conveying for Desulfurization and Denitrification Agents
Implementing pneumatic conveying systems for desulfurization and denitrification agents offers several significant benefits. The primary advantage is improved operational efficiency, as the system allows for continuous, automated material transport without the need for manual handling. This reduces labor costs and minimizes the risk of human error. Additionally, the closed system enhances safety by preventing dust exposure, which is a major health hazard in powder handling environments. The equipment also contributes to cost savings through reduced material loss and lower maintenance requirements. Furthermore, the precise control over material flow ensures consistent product quality, which is vital for maintaining compliance with environmental standards and meeting customer specifications.
Conclusion
Pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and safe handling of desulfurization and denitrification agents. By understanding the working principle and leveraging the key features of these systems, industrial facilities can enhance their operational performance, improve safety standards, and reduce overall costs. As a leading manufacturer in China, HeadPowder continues to innovate in powder handling technology, providing tailored solutions that meet the evolving needs of the industry.