

Working Principle and Features of Coal Gangue Material Pneumatic Conveying Systems
Coal gangue, a byproduct generated during coal mining and processing, presents unique challenges in terms of handling and transportation. Its abrasive properties, variable particle size distribution, and potential for dust generation make traditional mechanical conveyors less effective. Pneumatic conveying systems emerge as a superior alternative, offering a dust-free, low-maintenance solution for transporting coal gangue from extraction sites to processing facilities or disposal areas. This article delves into the fundamental working principle and distinctive features of coal gangue pneumatic conveying systems, providing insights into their operational efficiency and industrial applicability.
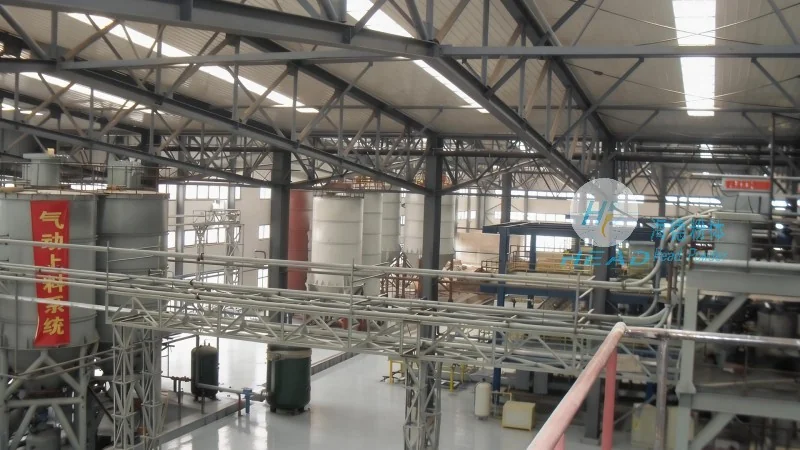
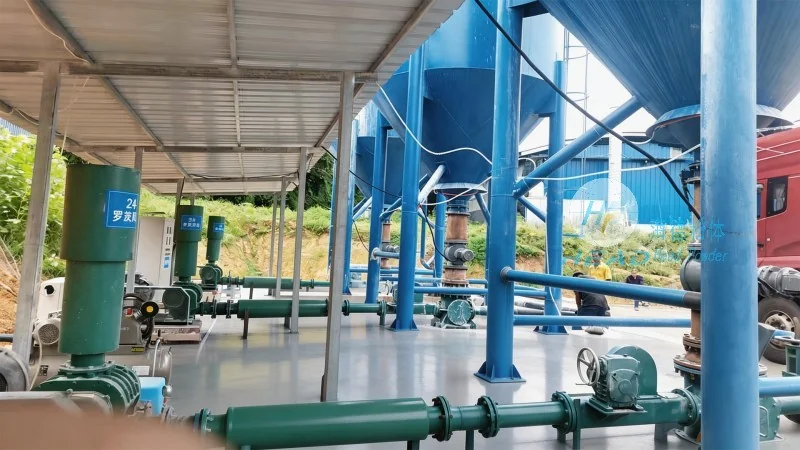
Working Principle of Coal Gangue Pneumatic Conveying Systems
The operation of coal gangue pneumatic conveying systems is based on the principle of fluidization and pneumatic transport. The system comprises several key components: a material hopper for storing the coal gangue, a feeder to control the flow rate of the material into the pipeline, a conveying pipeline where the material is propelled by compressed air, and a receiver to collect the material at the destination. The process initiates when the coal gangue is discharged from the hopper into the feeder. The feeder then introduces the material into the pipeline at a controlled rate. Compressed air, typically supplied by a blower or compressor, is introduced at the inlet of the pipeline. The high-velocity air flow creates a negative pressure within the pipeline, which draws the material particles into the air stream. As the material is entrained by the air, it travels through the pipeline to the receiver. The design of the pipeline, including bends, elbows, and expansion joints, is critical to maintaining the air velocity and preventing material deposition or blockages. The system ensures that the material is transported without direct contact with mechanical parts, minimizing wear and reducing the risk of material contamination.
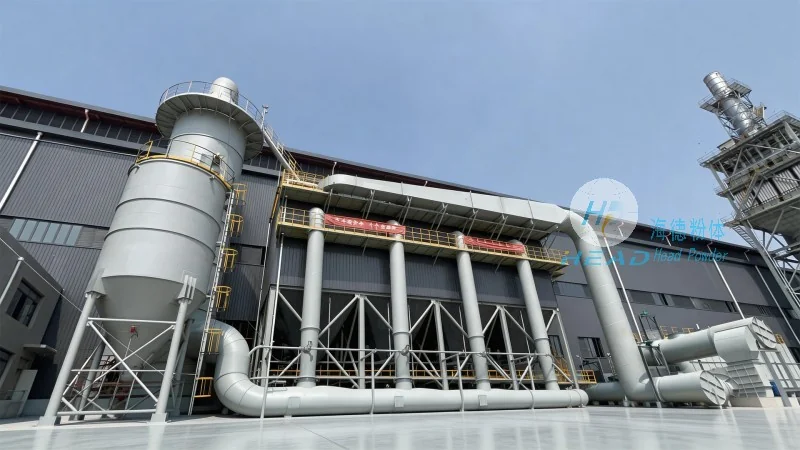
Key Features of Coal Gangue Pneumatic Conveying Systems
Coal gangue pneumatic conveying systems exhibit several advantages that make them ideal for industrial applications. Firstly, the systems provide a dust-free operation, which is crucial for maintaining environmental compliance and protecting equipment from dust accumulation. Unlike belt conveyors, which can generate significant dust, pneumatic systems contain the material within the pipeline, reducing the risk of airborne particles and improving workplace safety. Secondly, the systems offer high flexibility in terms of layout and installation. The pipeline can be easily routed around obstacles, and the system can be expanded or reconfigured to accommodate changes in production needs. This adaptability is particularly valuable in mining operations where the extraction site may shift or the processing facility may be repositioned. Thirdly, the systems are highly efficient in terms of energy consumption. By using compressed air to transport the material, the system minimizes energy waste compared to mechanical conveyors that rely on motor-driven components. Additionally, the systems are capable of handling a wide range of material characteristics, including different particle sizes, moisture contents, and abrasiveness levels. This versatility makes them suitable for various coal gangue compositions, from fine powders to coarse lumps.
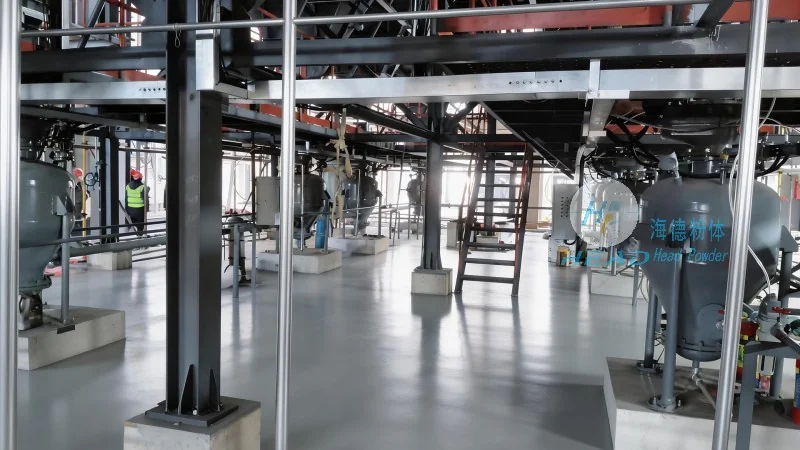
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer specializing in material handling equipment, with a focus on pneumatic conveying systems for the coal and mining industries. HeadPowder is headquartered in Shandong, China, and has established itself as a leader in providing customized solutions for bulk material transport. The company's expertise lies in the design and implementation of efficient, reliable, and low-maintenance systems that meet the specific requirements of industrial clients. With a strong commitment to quality and innovation, HeadPowder has built a reputation for delivering products that enhance operational efficiency and reduce costs for its customers. The company's team of engineers and technicians works closely with clients to understand their operational needs and develop tailored solutions that optimize material handling processes. HeadPowder's products are known for their durability, energy efficiency, and compliance with industry standards, making them a preferred choice for businesses in the coal and mining sectors.