

Principle and Working Scene Characteristics of Intelligent Tonne Bag Loading Station with Pneumatic
HeadPowder, a leading engineering firm based in Shandong, China, specializes in advanced material handling solutions. The intelligent tonne bag loading station with pneumatic conveying is a prime example of their innovative approach to industrial material processing. This system integrates cutting-edge technology to streamline the process of handling bulk materials from large tonne bags, making it an essential component for modern manufacturing and processing facilities.
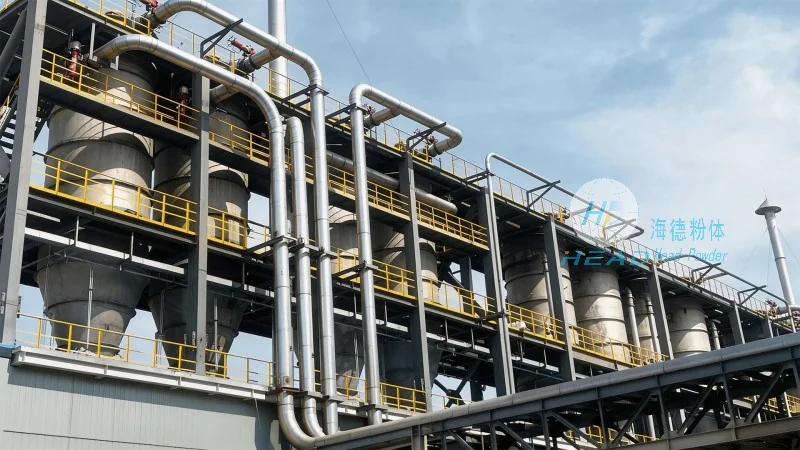
Understanding the Pneumatic Conveying Principle
The core of the intelligent tonne bag loading station lies in its pneumatic conveying system. This technology utilizes air pressure to transport bulk materials from the storage bags to the processing equipment. The process begins with the opening of the tonne bag, where the material is released into a hopper or a collection chamber. A blower or a vacuum pump then generates the necessary airflow to draw the material through a pipeline network. The system is designed to handle various materials, including powders, granules, and even fine particles, ensuring efficient and consistent material transfer. The pneumatic conveying principle minimizes the need for manual handling, reduces material loss, and enhances overall operational safety.
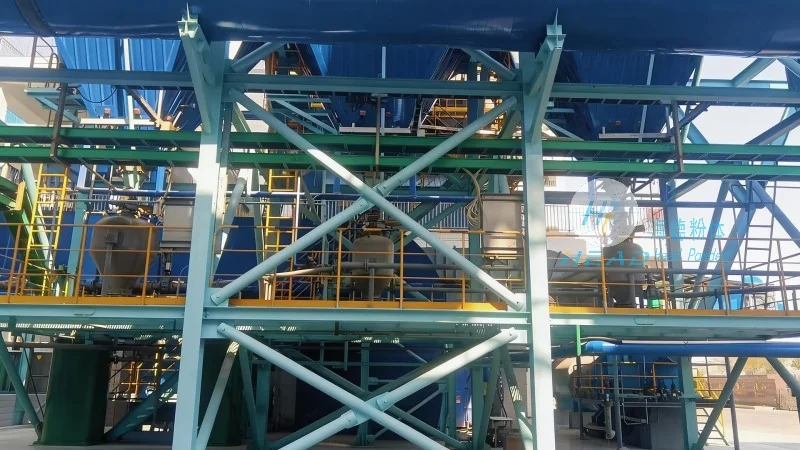
Key Components and Operational Mechanics
Several critical components work in tandem to ensure the smooth operation of the intelligent tonne bag loading station. The primary components include the tonne bag discharging mechanism, the airlock system, the conveying pipeline, and the material collection hopper. The discharging mechanism typically involves a bag opener that safely releases the material without spillage. The airlock system prevents backflow of air and material, maintaining a controlled environment. The conveying pipeline is often made of durable materials like stainless steel or PVC to withstand the abrasive nature of the materials being transported. The material collection hopper then stores the conveyed material before it is fed into the downstream processing equipment. The entire system operates automatically, with sensors and control panels monitoring the flow rate, pressure, and material level to ensure optimal performance.
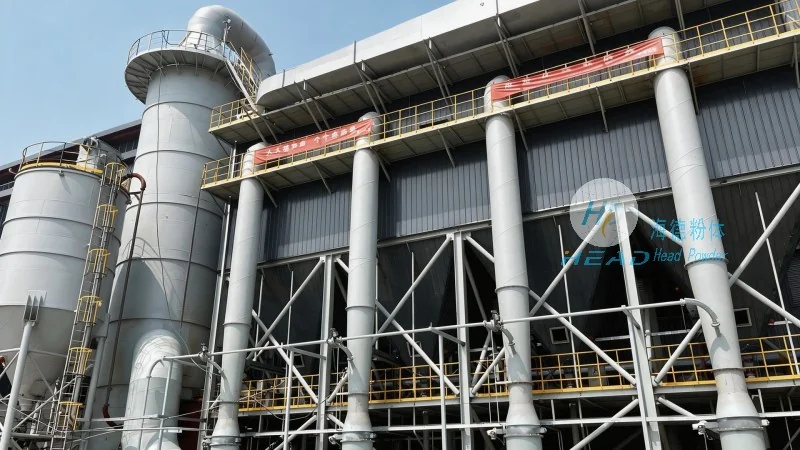
Working Scene Characteristics and Application Scenarios
The intelligent tonne bag loading station with pneumatic conveying is particularly suited for industrial environments where large volumes of bulk materials need to be processed efficiently. Common applications include the chemical, food, pharmaceutical, and mining industries. In these settings, the system is used to handle raw materials such as chemicals, powders, and minerals, feeding them into mixers, reactors, or other processing units. The working scene characteristics highlight the system's ability to handle high material throughput while maintaining low maintenance requirements. The automated nature of the system reduces labor costs and minimizes human exposure to potentially hazardous materials. Additionally, the system's modular design allows for easy integration into existing production lines, making it a versatile solution for various industrial needs.
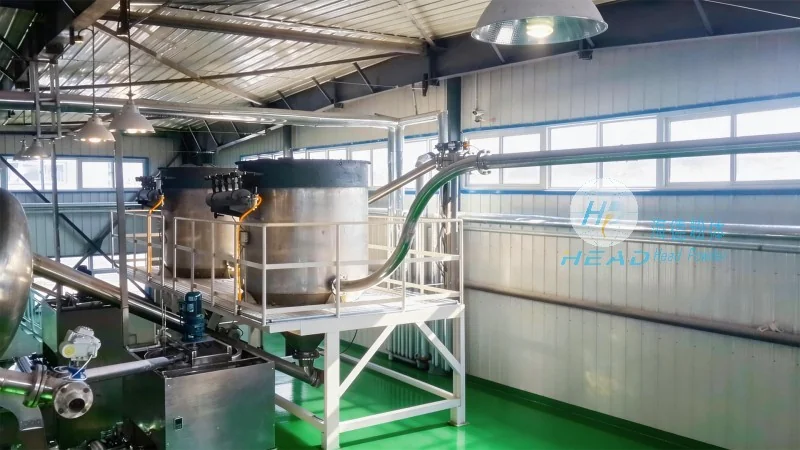
Advantages and Benefits in Real-World Operations
Implementing the intelligent tonne bag loading station with pneumatic conveying offers numerous advantages for industrial operations. One of the key benefits is the significant reduction in material handling time and labor costs. By automating the material transfer process, the system increases production efficiency and reduces downtime. The pneumatic conveying method also minimizes material contamination and loss, ensuring that the quality of the processed material remains consistent. Furthermore, the system's compact design and low noise operation make it suitable for use in various industrial settings, including those with strict environmental regulations. The advanced control systems provide real-time monitoring and data logging, enabling operators to optimize the system's performance and troubleshoot issues quickly. Overall, the intelligent tonne bag loading station enhances operational safety, improves material quality, and boosts overall productivity in industrial applications.