

Principles and Application Scenarios of Cereal Pneumatic Conveying System Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced pneumatic conveying systems tailored for the cereal processing industry. This article explores the fundamental principles underlying these systems and highlights the key operational characteristics and application scenarios that define their effectiveness in modern food processing operations.
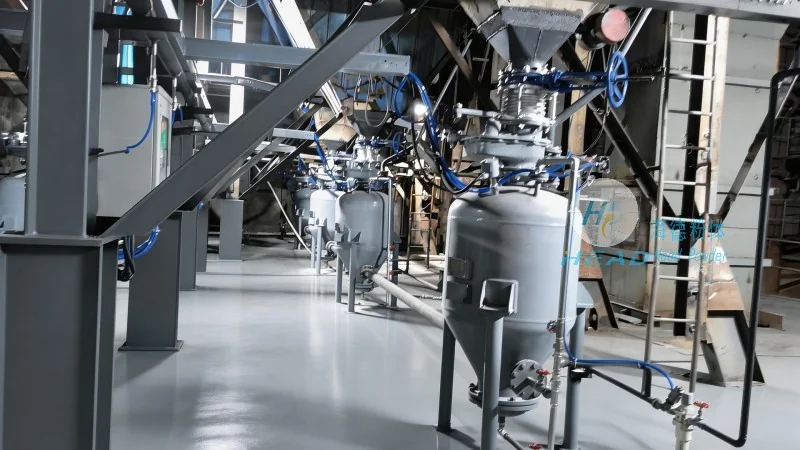
Understanding the Core Principles of Cereal Pneumatic Conveying Systems
The fundamental principle of a cereal pneumatic conveying system is the use of compressed air to transport bulk materials, such as cereals, from one location to another within a processing facility. This method, known as pneumatic conveying, offers a highly efficient and hygienic alternative to traditional mechanical conveying solutions. The system typically operates by creating a pressure differential between the inlet and outlet of the conveying line, which draws the material into the pipeline and propels it toward the destination. Key components of this system include a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the material at the end of the line. The selection of the appropriate conveying method—whether pressure or vacuum—depends on factors like the material's properties, the distance to be covered, and the desired flow rate.
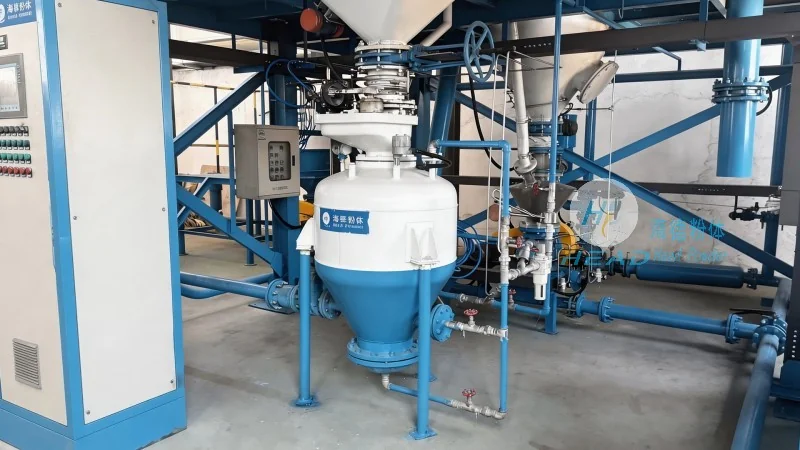
Key Operational Characteristics of Cereal Pneumatic Conveying Equipment
Efficiency and reliability are paramount in the design of cereal pneumatic conveying systems. These systems are engineered to handle a wide range of cereal types, including wheat, corn, oats, and rice, with minimal degradation of the product. The use of stainless steel and food-grade materials ensures compliance with hygiene standards, making them suitable for applications in food processing plants. The systems are also designed for easy maintenance, with components that can be easily accessed and cleaned, reducing downtime and operational costs. Additionally, modern systems incorporate advanced control technologies, such as variable frequency drives (VFDs), to optimize energy consumption and maintain consistent material flow rates. This results in improved process control and reduced energy costs over time.
Common Application Scenarios in the Cereal Processing Industry
Cereal pneumatic conveying systems are widely used in various stages of cereal processing, from raw material handling to finished product packaging. In the raw material reception area, these systems efficiently transport bulk cereals from storage silos or trucks into processing lines. During the milling or grinding process, they can convey ground cereals to storage bins or packaging machines. In the packaging stage, the systems are used to move finished cereal products from production lines to packaging lines, ensuring a seamless flow of goods. The versatility of these systems also makes them suitable for applications in blending different cereal types to create custom formulations, or for transferring materials between different processing units within a facility. Their ability to handle both dry and slightly moist cereals makes them adaptable to diverse production requirements.
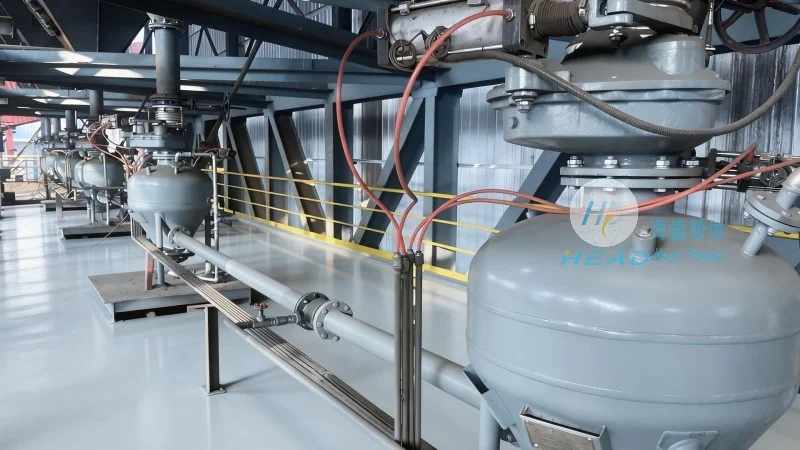
Advantages of Choosing HeadPowder's Cereal Pneumatic Conveying Solutions
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, offers a comprehensive range of cereal pneumatic conveying systems that are tailored to meet the specific needs of the food processing industry. Our systems are designed with a focus on durability, efficiency, and hygiene, ensuring that they can withstand the demands of continuous operation in a food processing environment. The company's expertise in material handling and pneumatic conveying technology allows for the development of customized solutions that address the unique challenges faced by each client. By selecting HeadPowder's equipment, businesses can benefit from improved operational efficiency, reduced maintenance costs, and enhanced product quality. The company's commitment to quality and customer satisfaction is reflected in its rigorous testing procedures and after-sales support services, providing clients with reliable and long-lasting solutions for their material handling needs.