

Principle and Working Scene Characteristics of Sodium Hexafluorophosphate Powder Conveying System Eq
HeadPowder, a leading provider in the field of powder handling technology, specializes in advanced solutions for the efficient and reliable transportation of sodium hexafluorophosphate. This article delves into the core principles and operational characteristics of the powder conveying systems designed specifically for this application, highlighting how these systems enhance process efficiency and safety in industrial settings.
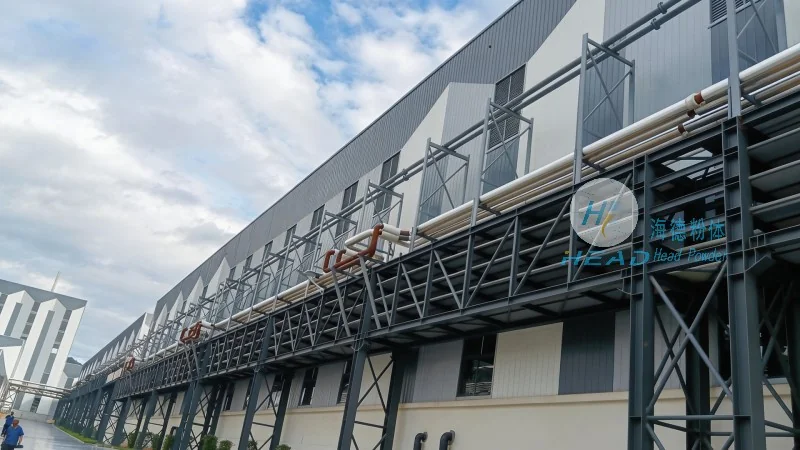
Company Profile and Expertise
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable enterprise based in Shandong, China. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner in the powder processing industry. The company's expertise lies in the design, manufacturing, and integration of sophisticated powder handling systems tailored to meet the unique demands of various industrial applications.
Introduction to Sodium Hexafluorophosphate Powder Conveying Systems
Sodium hexafluorophosphate (NaPF₆) is a critical chemical compound widely used in the production of lithium-ion batteries, pharmaceuticals, and other high-tech industries. The efficient and safe handling of this powder is paramount to maintaining product quality and operational safety. HeadPowder's powder conveying systems are engineered to address the specific challenges associated with transporting NaPF₆, including its hygroscopic nature, potential for static discharge, and the need for precise control over flow rates and particle distribution.
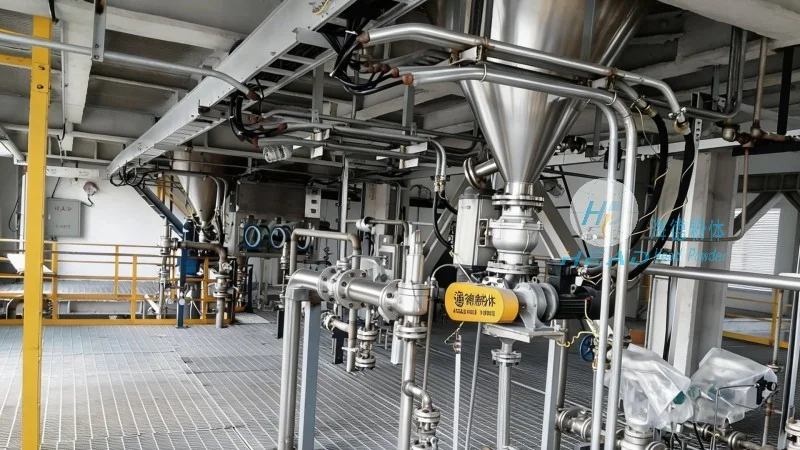
Principle of Operation: Key Components and Mechanisms
The core of the powder conveying system for sodium hexafluorophosphate involves several critical components working in concert to ensure smooth and controlled material transport. These components typically include a hopper for material storage, a feeder to regulate the flow of powder, a conveying mechanism (such as a screw conveyor or pneumatic system), and a control system to monitor and adjust operational parameters. The system operates on the principle of maintaining a consistent pressure and flow rate, preventing clogging and ensuring that the powder moves through the system without degradation or contamination.
Working Scene Characteristics: Efficiency and Safety in Industrial Applications
The working scene characteristics of these conveying systems are tailored to the specific requirements of industrial environments where sodium hexafluorophosphate is processed. Key features include:
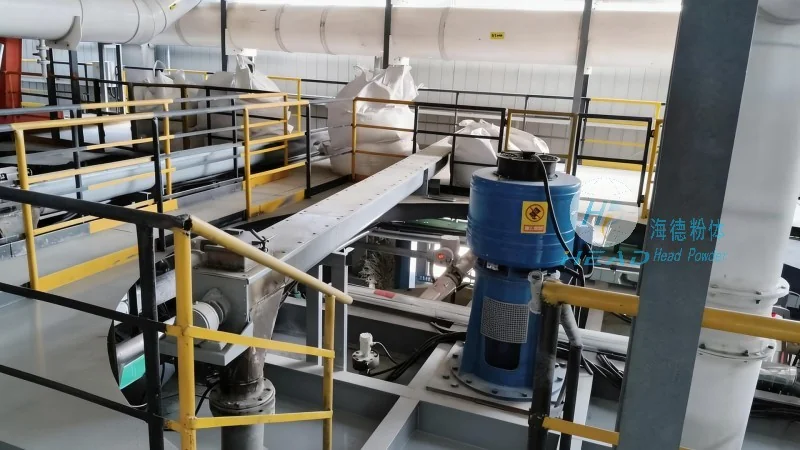
- Hygienic Design: Systems are constructed with materials that are resistant to corrosion and easy to clean, ensuring compliance with industry standards for pharmaceutical and battery manufacturing.
- Static Control: Integrated anti-static measures are implemented to prevent electrostatic discharge, which can be hazardous when handling fine powders.
- Flow Control: Advanced control algorithms and sensors allow for precise regulation of powder flow, minimizing variations and optimizing process efficiency.
- Space Efficiency: Compact and modular designs enable easy integration into existing production lines, reducing installation time and costs.
Application Scenarios: Enhancing Process Performance
HeadPowder's sodium hexafluorophosphate powder conveying systems are deployed in various industrial settings, including:
- Battery Manufacturing: In the production of lithium-ion batteries, the system ensures a steady supply of NaPF₆ to the mixing and coating stages, contributing to consistent battery performance and quality.
- Pharmaceutical Processing: For the formulation of pharmaceutical products, the system maintains the purity and integrity of the powder, adhering to stringent regulatory requirements.
- Chemical Synthesis: In chemical plants, the system facilitates the transport of NaPF₆ between reaction and separation stages, enhancing overall production throughput.
Conclusion: Advancing Industrial Efficiency with Specialized Solutions
HeadPowder's powder conveying systems for sodium hexafluorophosphate exemplify the company's commitment to delivering high-performance, reliable solutions that meet the evolving needs of modern industry. By integrating advanced technology with a deep understanding of powder handling challenges, these systems not only improve operational efficiency but also enhance safety and product quality. As a result, industries relying on sodium hexafluorophosphate can achieve greater productivity and competitiveness through the adoption of these specialized conveying solutions.