

Principles and Working Scene Characteristics of Pneumatic Conveying for Sorghum Distillers Grains Po
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design and implementation of advanced pneumatic conveying systems. With a focus on efficient material transport solutions, the company provides tailored services for various industrial applications, including the handling of sorghum distillers grains powder—a byproduct of the distillation process in the alcohol industry.
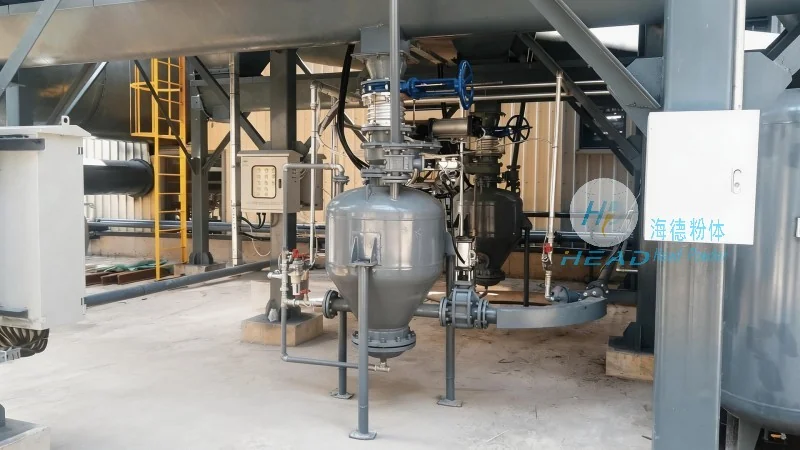
Sorghum distillers grains powder, commonly known as DDGS (Dried Distillers Grains with Solubles), is a valuable feed ingredient rich in protein and fiber. However, its handling requires specialized equipment due to its fine particle size and potential for dust generation. Pneumatic conveying offers a safe, efficient, and cost-effective method to transport this powder from storage silos to processing facilities, ensuring minimal product loss and contamination.
Pneumatic Conveying: The Core Principle
Pneumatic conveying utilizes compressed air or gas to transport bulk materials through a pipeline system. In the case of sorghum distillers grains powder, the system typically operates under positive pressure, where air is forced through the material to create a slurry that moves along the pipeline. This method eliminates the need for mechanical components like conveyor belts or buckets, reducing maintenance costs and improving operational reliability. The principle involves several key components: a hopper for material storage, a feeder to control the flow rate, a compressor to generate the air pressure, and a pipeline network to direct the material to its destination.
Working Scene Characteristics: Efficiency and Safety
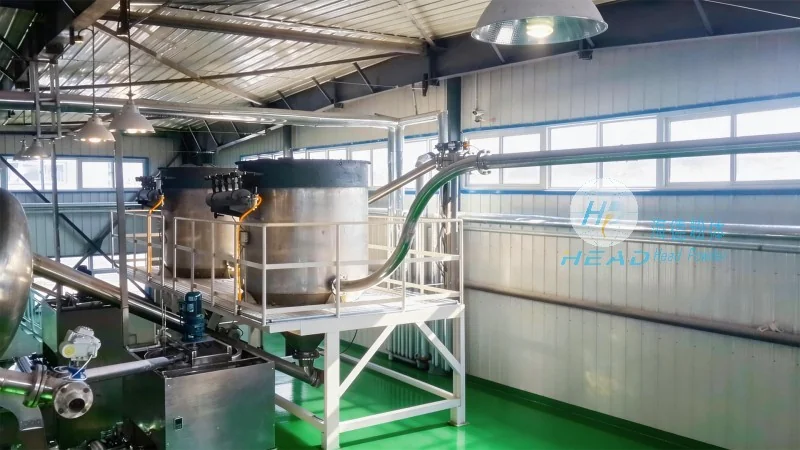
The application of pneumatic conveying for sorghum distillers grains powder is characterized by several distinct working scene features that enhance operational performance. First, the system’s ability to handle fine powders without clogging is critical, as DDGS particles can range from 100 to 500 microns in size. The design of the conveying system, including the use of flexible hoses or rigid pipes with appropriate diameters, ensures smooth material flow and prevents blockages. Second, the system’s dust control measures are essential for maintaining a safe working environment. By enclosing the entire conveying process, the system reduces airborne dust, which is a major health hazard in the feed industry. This is achieved through sealed hoppers, enclosed pipelines, and dust collection systems that capture any particles released during transport.
Customization and Scalability: Tailored Solutions for Diverse Needs
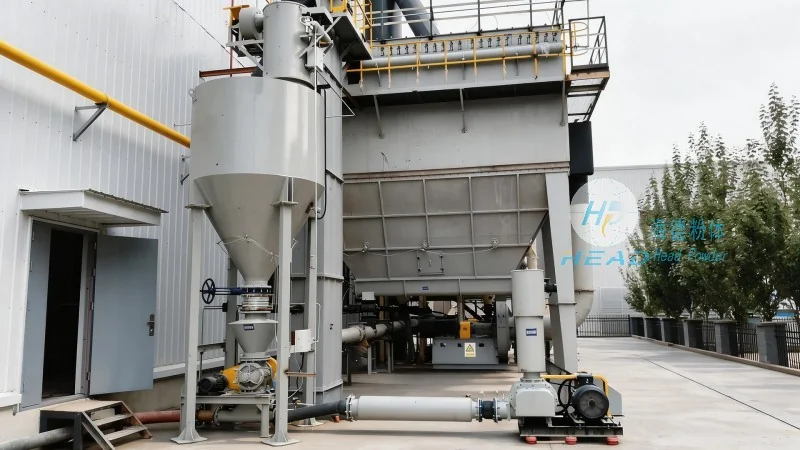
HeadPowder understands that each industrial facility has unique requirements for material handling. Therefore, the company offers customized pneumatic conveying solutions that can be scaled to meet the specific needs of clients. Whether a small-scale operation or a large industrial plant, the system can be designed to handle varying capacities, from low to high throughput. The customization includes selecting the appropriate air pressure, pipeline length, and component materials (such as stainless steel or food-grade plastics) to ensure compatibility with the sorghum distillers grains powder. Additionally, the system can be integrated with existing infrastructure, minimizing downtime and installation costs.
Advantages Over Traditional Methods
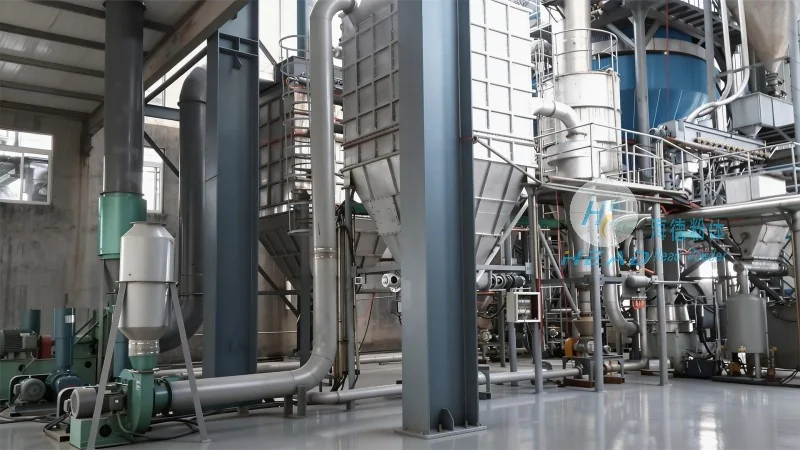
Compared to traditional handling methods like bucket elevators or screw conveyors, pneumatic conveying offers several advantages for sorghum distillers grains powder. The primary benefit is the reduction in product degradation due to less exposure to air and moisture. This is particularly important for a product like DDGS, which can lose nutritional value if exposed to the elements. Another advantage is the improved hygiene and sanitation, as the enclosed system prevents contamination from external sources. Furthermore, the system’s energy efficiency is higher than mechanical alternatives, as it uses less power to transport the same amount of material over longer distances. This results in lower operational costs and a smaller environmental footprint.
Conclusion: Enhancing Productivity and Safety
For industries dealing with sorghum distillers grains powder, pneumatic conveying is a superior choice for efficient and safe material transport. HeadPowder, with its expertise in powder handling technology, provides reliable and customized solutions that meet the specific needs of clients. By leveraging the principles of pneumatic conveying, companies can enhance their operational efficiency, reduce costs, and ensure a safe working environment. As a leading provider in China, HeadPowder continues to innovate and deliver high-quality systems that contribute to the success of its clients in the feed and alcohol industries.