

Operation Process and Working Principle of Bentonite Powder Conveying System
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier based in Shandong, China. The company specializes in the design, development, and production of advanced powder conveying systems, with a focus on bentonite powder handling solutions. HeadPowder's expertise lies in creating efficient and reliable systems that meet the demanding requirements of various industrial applications.
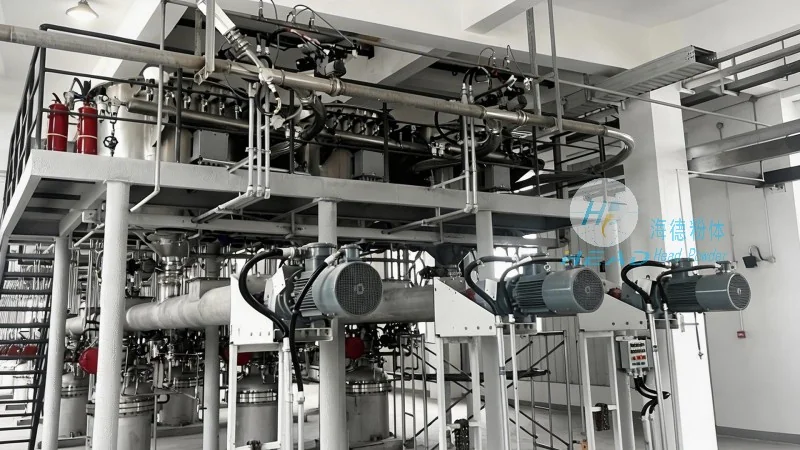
Overview of Bentonite Powder Conveying System
A bentonite powder conveying system is a specialized equipment designed to transport bentonite powder from a storage area to a processing or application point. Bentonite, a natural clay mineral, is widely used in industries such as drilling fluids, foundry, and cosmetics due to its unique properties like high swelling capacity and excellent thixotropy. The conveying system ensures the safe and efficient movement of this fine powder, which is crucial for maintaining product quality and operational efficiency.
Operation Process of the Bentonite Powder Conveying System
The operation of a bentonite powder conveying system typically involves several key steps to ensure smooth and continuous material handling. First, the bentonite powder is stored in a hopper or silo, where it is kept under controlled conditions to prevent caking or moisture absorption. The system then uses a combination of mechanical and pneumatic components to transport the powder. For example, a screw conveyor or a pneumatic conveyor may be employed, depending on the specific requirements of the application. The process begins with the powder being fed from the storage hopper into the conveyor inlet. The conveyor then moves the powder through a series of tubes or channels, using either rotational motion (in the case of screw conveyors) or air pressure (in pneumatic systems) to propel the material forward. Along the way, the system may include components like rotary valves, airlocks, and dust collectors to regulate the flow and maintain cleanliness. The final step involves delivering the bentonite powder to the target location, such as a mixing tank or a processing unit, where it can be further utilized. The entire process is controlled by a programmable logic controller (PLC) or a similar control system, which monitors the flow rate, pressure, and other parameters to ensure optimal performance and prevent any operational issues.
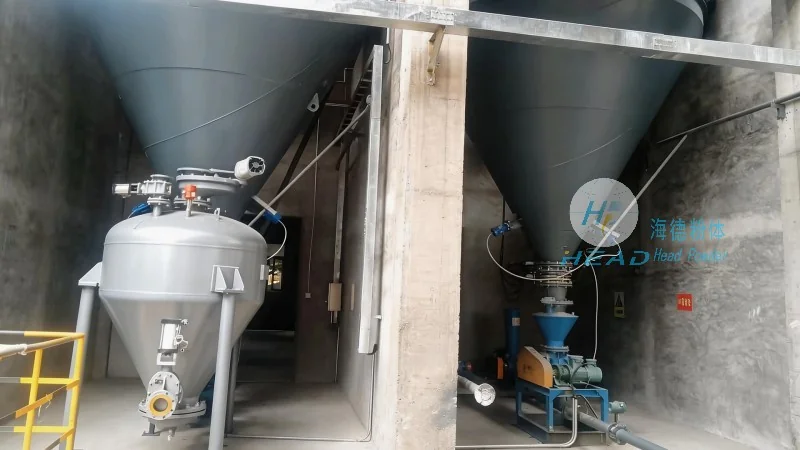
Working Principle of the Bentonite Powder Conveying System
The working principle of a bentonite powder conveying system is based on the physical properties of the material and the design of the conveying equipment. Bentonite powder is a fine, cohesive material that can be prone to caking and blockages if not handled properly. Therefore, the system is engineered to minimize these issues through careful design and operation. In a typical mechanical conveying system, a screw conveyor is used. The screw, which is made of durable materials like stainless steel or high-grade plastic, rotates within a trough or tube. As the screw rotates, it pushes the bentonite powder forward, similar to how a screw moves through a nut. The pitch and speed of the screw are carefully selected to ensure the powder is conveyed without excessive pressure, which could cause clogging. For pneumatic conveying systems, the principle involves using compressed air to create a flow of air and powder mixture. The bentonite powder is fed into a hopper, and then air is introduced, creating a slurry that is carried through the pipeline. The air pressure and velocity are controlled to maintain a stable flow and prevent particle separation or deposition. The system may also include cyclone separators or filters to separate the powder from the air at the discharge point, ensuring that the powder is collected efficiently and the air is cleaned before release. The control system plays a critical role in regulating the air flow, pressure, and powder feed rate, ensuring that the conveying process is smooth and consistent.
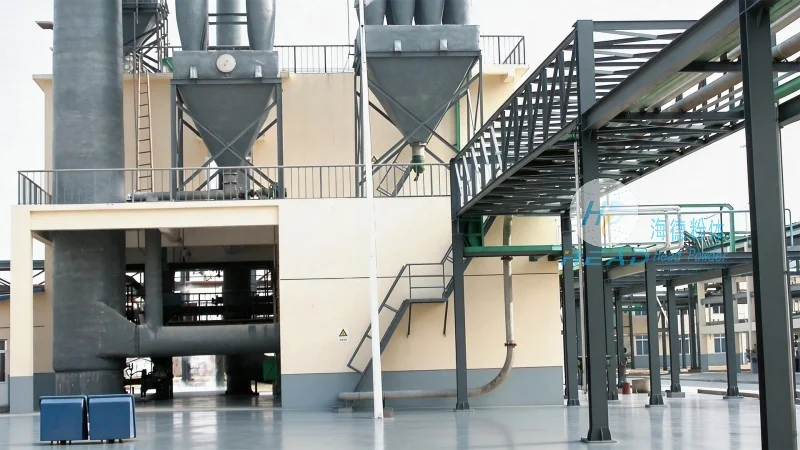
Technical Advantages of the System
HeadPowder's bentonite powder conveying system offers several technical advantages that make it suitable for various industrial applications. One of the key advantages is its high efficiency in material handling. The system can transport large quantities of bentonite powder at a consistent rate, reducing downtime and increasing overall productivity. The use of advanced materials and components ensures durability and long service life, minimizing maintenance costs and downtime. The system is also designed for low maintenance, with easy access to components for inspection and replacement. Additionally, the system is equipped with safety features such as overpressure relief valves and dust collection systems, ensuring safe operation and compliance with industrial safety standards. The modular design of the system allows for easy customization to meet specific customer requirements, such as different conveyor lengths, material capacities, or control interfaces. This flexibility makes the system adaptable to a wide range of applications, from small-scale laboratory use to large-scale industrial production.
Applications of Bentonite Powder Conveying System
The bentonite powder conveying system from HeadPowder is widely used in various industries where bentonite is a critical component. In the oil and gas industry, the system is used to transport bentonite powder for drilling fluid preparation, ensuring the fluid has the right viscosity and stability for drilling operations. In the foundry industry, the system is used to convey bentonite for mold and core making, improving the quality and consistency of the castings. In the cosmetics industry, the system is used to transport bentonite for the production of skincare and beauty products, maintaining the purity and quality of the final product. The system's ability to handle fine powders with minimal degradation or contamination makes it suitable for applications where product quality is paramount. Additionally, the system is used in environmental applications, such as waste treatment and soil stabilization, where bentonite is used to immobilize contaminants or improve soil properties. The versatility of the system allows it to be integrated into existing production lines or used as a standalone unit, depending on the specific needs of the customer.