

Inert Dust-Free Metering Powder Handling Equipment: Operation Process and Working Principle
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced inert dust-free metering powder handling equipment. This equipment is engineered to handle powders with high precision and minimal contamination, making it an essential solution for industries that demand strict quality control and environmental compliance.
Company Overview
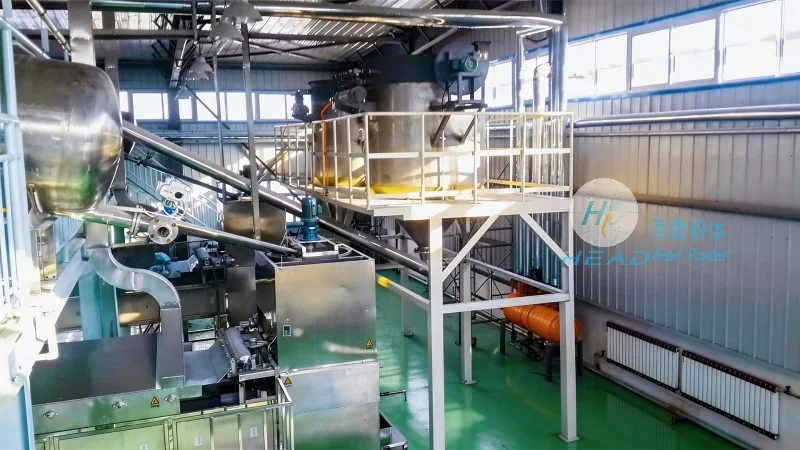
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing innovative powder handling solutions. With a strong focus on research and development, the company has established itself as a trusted partner in the industry. HeadPowder is committed to delivering high-quality equipment that meets the evolving needs of modern manufacturing processes. The company’s headquarters is located in Shandong, China, where it operates a state-of-the-art facility for product development and manufacturing.
Understanding the Operation Process of Inert Dust-Free Metering Equipment
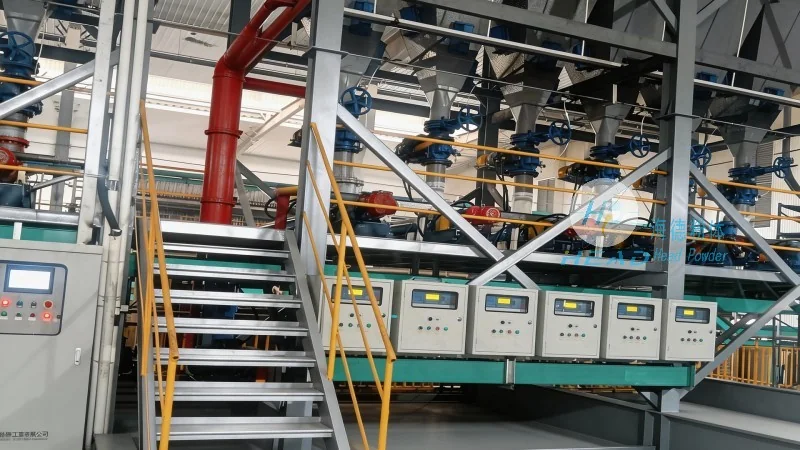
The operation process of inert dust-free metering powder handling equipment involves several key steps designed to ensure accurate and reliable powder transfer. The process begins with the preparation of the powder, which is typically stored in a sealed container to maintain its inert properties and prevent contamination. The equipment then uses a precise dosing mechanism to measure and dispense the required amount of powder. This mechanism often incorporates advanced sensors and control systems to adjust the flow rate in real-time, ensuring consistent and accurate delivery. The powder is then transported through a sealed, dust-free pipeline to the processing area, minimizing the risk of particle loss or environmental exposure.
Working Principle of the Equipment
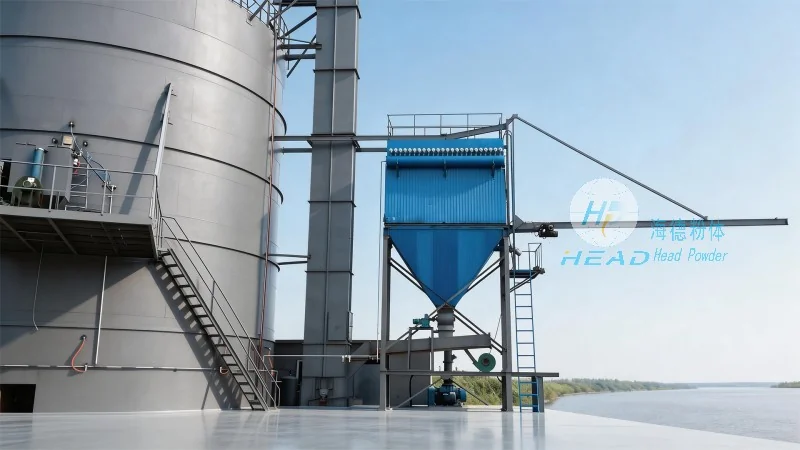
The working principle of inert dust-free metering powder handling equipment is centered on maintaining a controlled, contamination-free environment throughout the powder handling process. The equipment utilizes inert gases, such as nitrogen or argon, to create a protective atmosphere that prevents oxidation or moisture absorption of the powder. This inert environment is crucial for sensitive materials, as it preserves the powder’s properties and ensures product integrity. The metering system employs a combination of mechanical and electronic components to achieve precise control over the powder flow. For example, some models use a rotary valve or a gravimetric scale to measure the mass of the powder being dispensed, while others rely on volumetric or time-based dosing methods. The control system continuously monitors the process parameters, such as pressure, temperature, and flow rate, to maintain optimal operating conditions. This closed-loop control ensures that the equipment operates efficiently and reliably, reducing the risk of errors or product defects.
Key Features and Benefits
HeadPowder’s inert dust-free metering powder handling equipment offers several key features that enhance its performance and usability. One of the primary benefits is the ability to handle a wide range of powders, including those that are hygroscopic, reactive, or prone to caking. The equipment’s sealed design prevents cross-contamination and maintains the powder’s original characteristics. Additionally, the precise metering capability ensures that the correct amount of powder is delivered to the processing line, improving product consistency and reducing material waste. The equipment is also designed for easy maintenance and cleaning, with components that can be quickly disassembled and sanitized to meet stringent hygiene standards. This makes it suitable for industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity is paramount.
Application Examples
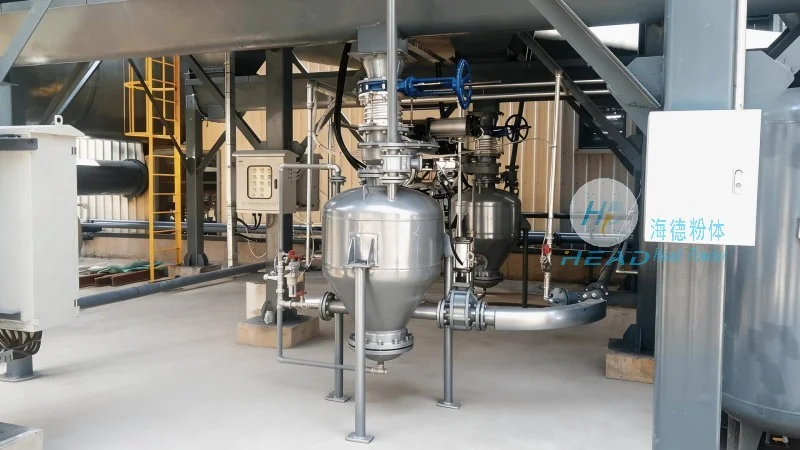
The applications of inert dust-free metering powder handling equipment are diverse and span multiple industries. In the pharmaceutical industry, the equipment is used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the final drug product meets strict quality and purity standards. In the food industry, it is employed to handle ingredients like sugar, flour, and spices, maintaining the product’s freshness and preventing contamination. The chemical industry also utilizes this equipment for handling reactive powders, such as catalysts and pigments, where precision dosing is critical for process efficiency. Overall, the equipment’s ability to maintain a dust-free and inert environment makes it an indispensable tool for any operation that requires high-purity powder handling.