

[Pneumatic Conveying in Bulk Stone Material Handling]
For industries dealing with bulk stone materials, efficient and reliable material handling is crucial. Pneumatic conveying systems offer a versatile solution that addresses the challenges of transporting aggregates like gravel, crushed stone, and other construction materials. This technology leverages air pressure to move solid particles through a pipeline, providing a dust-free, closed-loop operation that enhances safety and environmental compliance.
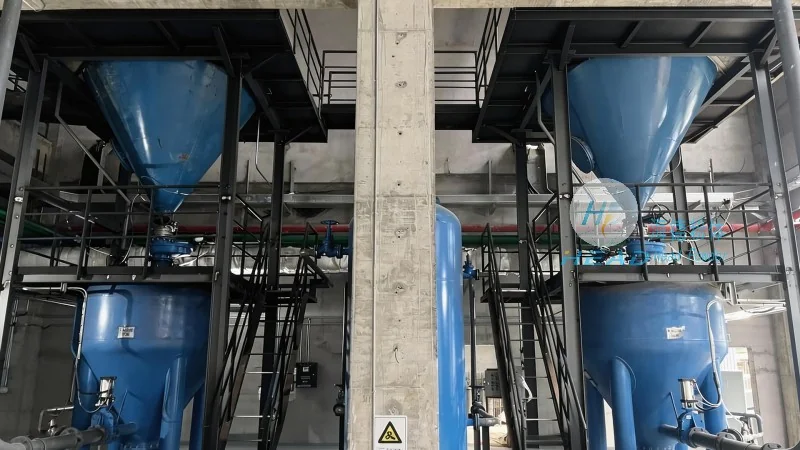
How Pneumatic Conveying Works in Stone Handling
Pneumatic conveying systems for stone materials typically operate by creating a pressure differential between the inlet and outlet of the conveying line. The system uses a blower or compressor to generate airflow, which draws or pushes the stone particles into the pipeline. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems are ideal for long-distance and high-capacity transport, while vacuum systems are better suited for shorter distances and more delicate materials. In stone handling applications, pressure systems are commonly used due to their ability to handle larger particles and higher volumes efficiently.
Key Benefits of Using Pneumatic Conveying for Stone Transport
Implementing pneumatic conveying for stone materials offers several advantages over traditional methods such as belt conveyors or bucket elevators. One of the primary benefits is the reduction of dust exposure, which is critical for maintaining a safe working environment and complying with environmental regulations. The closed-loop design of pneumatic systems also minimizes material loss and contamination, ensuring that the stone remains in its original state throughout the transport process. Additionally, these systems are highly adaptable, allowing for changes in material flow rates and destinations without significant modifications to the infrastructure. This flexibility makes them suitable for various applications, from quarry operations to construction sites and recycling facilities.
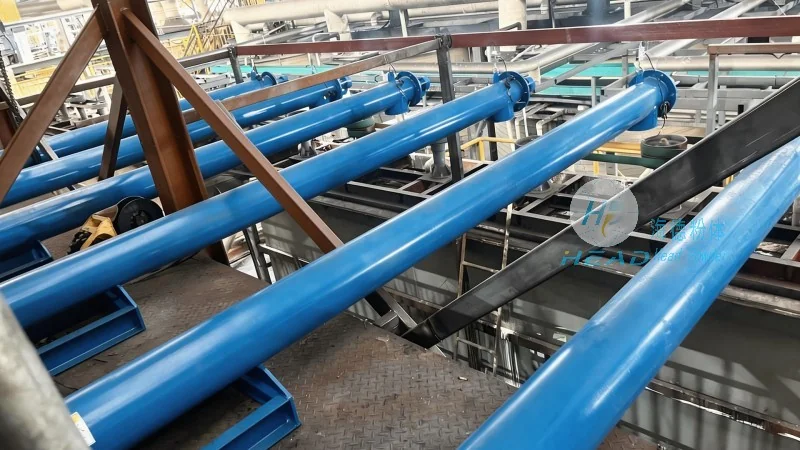
HeadPowder Engineering: Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of the stone industry. With years of experience in the field, the company has developed a comprehensive range of solutions that address the specific challenges of transporting bulk stone materials. HeadPowder's expertise lies in customizing systems to handle different particle sizes, moisture contents, and flow rates, ensuring optimal performance and efficiency. The company's team of engineers works closely with clients to understand their operational requirements and provide tailored solutions that meet their production goals.
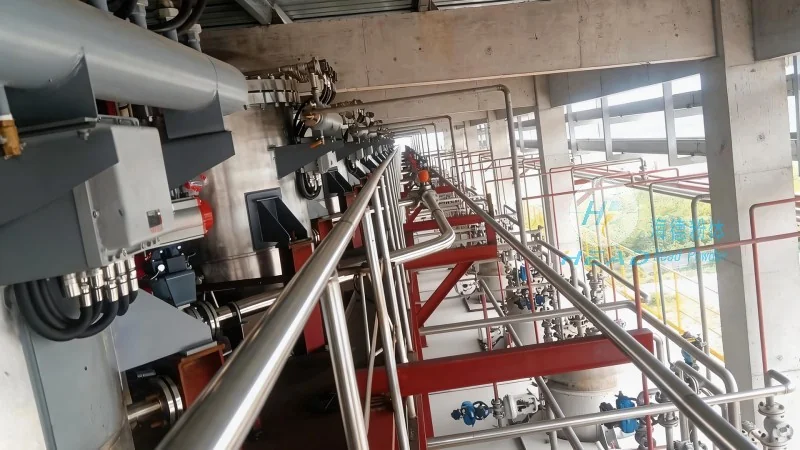
Customized Pneumatic Conveying Systems for Stone Handling
HeadPowder offers customized pneumatic conveying systems that are engineered to handle the demands of stone material transport. These systems can be designed for various applications, including quarry to processing plant transport, stockpile to loading areas, and even for recycling operations where stone is processed and reused. The company's solutions incorporate high-quality components, such as robust blower units, durable pipeline materials, and efficient separation equipment, ensuring long-term reliability and minimal maintenance. By leveraging advanced engineering and material science, HeadPowder's systems are built to withstand the harsh conditions often encountered in stone handling operations, such as high particle loads and abrasive environments.
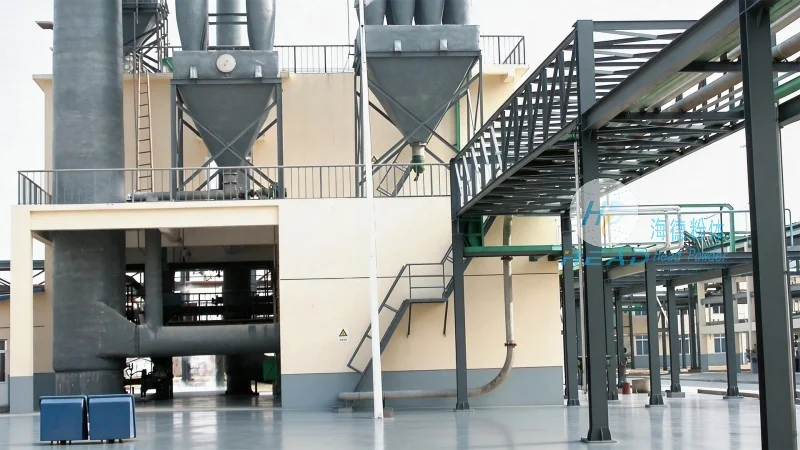
Enhancing Efficiency and Safety in Stone Material Handling
By adopting pneumatic conveying systems from HeadPowder, businesses in the stone industry can significantly enhance their operational efficiency and safety standards. The automated nature of these systems reduces the need for manual handling, minimizing the risk of workplace injuries and improving overall productivity. Additionally, the dust-free operation of pneumatic systems contributes to a healthier work environment, reducing respiratory issues and other health concerns associated with traditional material handling methods. HeadPowder's commitment to quality and innovation ensures that their systems not only meet current industry standards but also adapt to future technological advancements, providing long-term value to their clients.
Conclusion: The Future of Bulk Stone Transport with Pneumatic Conveying
As the construction and quarrying industries continue to evolve, the demand for efficient and sustainable material handling solutions remains high. Pneumatic conveying, with its ability to handle bulk stone materials with precision and reliability, is increasingly becoming the preferred choice for businesses seeking to optimize their operations. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this technology, providing expertly designed and manufactured pneumatic conveying systems that deliver superior performance and durability. By choosing HeadPowder's solutions, companies can ensure that their stone material transport processes are not only efficient but also safe, environmentally responsible, and adaptable to future industry needs.