

What is Fertilizer Granule Pneumatic Conveying? An Introduction to the Working Principle of Powder H
Understanding the mechanics of fertilizer granule pneumatic conveying is crucial for industries dealing with bulk powder handling. This process involves transporting granular materials like fertilizers through a pipeline using air or gas as the conveying medium. The technology has revolutionized the efficiency of material transport in agricultural and industrial sectors, offering a reliable alternative to traditional methods such as belt conveyors or bucket elevators.
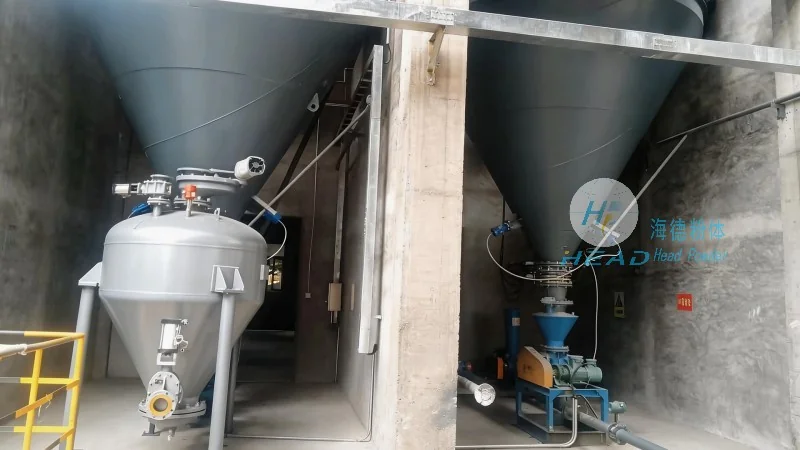
HeadPowder: A Leader in Powder Handling Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and manufacturing advanced pneumatic conveying systems tailored for the fertilizer industry. Our company, commonly known as HeadPowder, has established itself as a trusted partner for businesses seeking to optimize their material handling operations. With a strong presence in China, our headquarters are located in Shandong, where we leverage local expertise and resources to deliver high-quality solutions. Our commitment to innovation and customer satisfaction drives us to provide systems that meet the unique demands of fertilizer processing and distribution.
The Working Principle of Pneumatic Conveying Systems
Pneumatic conveying systems operate by creating a flow of air or gas within a pipeline to move granular materials. The process typically involves several key components: a feeding device to introduce the material into the system, a conveying line where the material is suspended and transported, and a collection or discharge unit to deliver the material to its destination. There are two primary types of pneumatic conveying: dilute phase and dense phase. Dilute phase systems use high-velocity air to transport materials in a dispersed state, while dense phase systems employ lower velocities and higher pressure to move material in a more concentrated form, reducing the risk of product degradation and pipeline blockages.
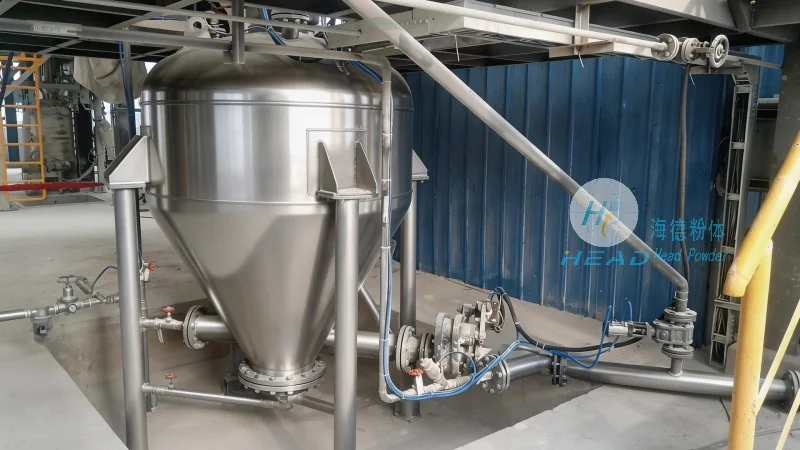
Key Components and Their Functions
Each component of a pneumatic conveying system plays a vital role in ensuring efficient and reliable operation. The feeding device, often a rotary valve or a star feeder, controls the flow rate of the fertilizer granules into the pipeline. This ensures a consistent and controlled introduction of material, preventing overloading or underloading of the system. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of fertilizer granules and the pressure of the conveying medium. The line may include bends, elbows, and other fittings that are carefully engineered to minimize pressure loss and maintain the flow of material. The collection or discharge unit, such as a cyclone separator or a rotary valve, separates the material from the air stream and directs it to the intended destination. In some systems, a filter or dust collector may be included to capture any fine particles and ensure environmental compliance.
Advantages of Pneumatic Conveying for Fertilizer Transport
Compared to traditional material handling methods, pneumatic conveying offers several advantages for fertilizer transport. One of the most significant benefits is the ability to transport materials over long distances without the need for multiple transfer points or intermediate storage. This reduces the risk of product contamination and loss, as the material remains enclosed within the pipeline. Additionally, pneumatic systems are highly flexible, allowing for changes in the layout or direction of the conveying line without major modifications. They also provide better control over the flow rate and pressure, enabling precise delivery of fertilizer to storage silos or processing facilities. Another key advantage is the reduced need for manual labor, as the system can operate continuously with minimal human intervention. This not only improves safety but also increases overall productivity and reduces operational costs.
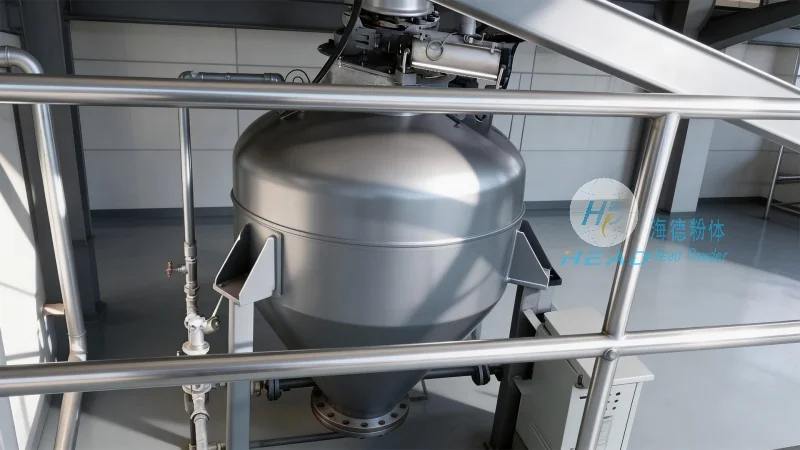
Applications in the Fertilizer Industry
Pneumatic conveying systems are widely used in various stages of fertilizer production and distribution. In the manufacturing process, they are used to transport raw materials such as urea, ammonium nitrate, and other granular compounds from storage silos to processing units. During packaging, the systems efficiently move finished fertilizer products from the production line to storage or shipping containers. In distribution centers, pneumatic conveying is employed to transfer bulk fertilizer to trucks or other delivery vehicles, ensuring timely and consistent supply to farms and agricultural businesses. The versatility of these systems makes them suitable for a wide range of fertilizer types, including nitrogen, phosphorus, and potassium (NPK) blends, as well as specialty fertilizers.
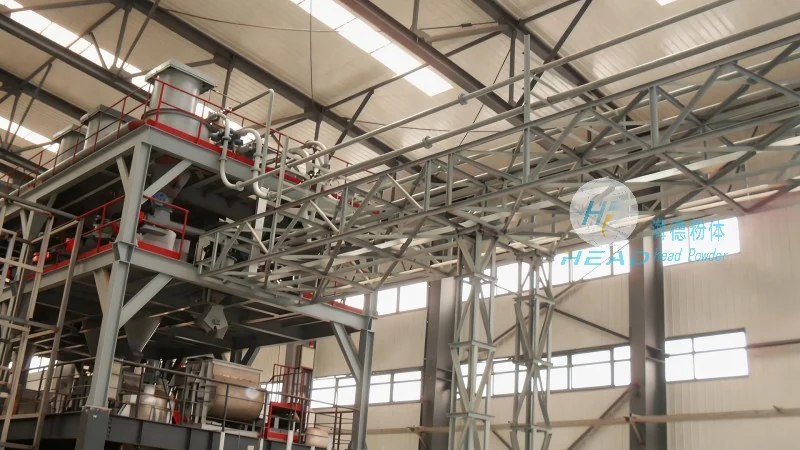
Ensuring Efficiency and Reliability
At HeadPowder, we understand that the success of a pneumatic conveying system depends on its efficiency and reliability. Our engineers design systems with a focus on minimizing energy consumption and maximizing material throughput. By optimizing the air velocity, pressure, and pipeline design, we ensure that the system operates at peak performance while reducing operational costs. Regular maintenance and quality control are also critical to maintaining the system's reliability. Our team provides comprehensive support, including installation, commissioning, and ongoing maintenance services, to ensure that our clients' systems run smoothly and efficiently. We also offer customized solutions to address specific challenges, such as handling abrasive materials or dealing with varying flow rates.
Conclusion
Fertilizer granule pneumatic conveying is a sophisticated and efficient method for transporting bulk materials in the agricultural industry. By leveraging the principles of pneumatic transport, businesses can improve their operational efficiency, reduce costs, and enhance product quality. At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing advanced powder handling solutions that meet the evolving needs of the fertilizer sector. Our expertise in designing and manufacturing pneumatic conveying systems ensures that our clients receive reliable and effective solutions tailored to their specific requirements. Whether you are a fertilizer manufacturer, distributor, or processor, HeadPowder is your partner in optimizing your material handling operations and achieving greater success in the industry.