

What is a Dry Gravel Material Handling System? And What Are Its Design Principles?
Dry gravel material handling systems are specialized equipment designed to transport loose, dry gravel or similar granular materials efficiently and safely. These systems are crucial in various industries, including construction, mining, and landscaping, where the movement of bulk materials is a common requirement. The primary goal of such systems is to minimize material degradation, reduce labor costs, and enhance operational efficiency by automating the handling process.
The Core Components and Operational Principles
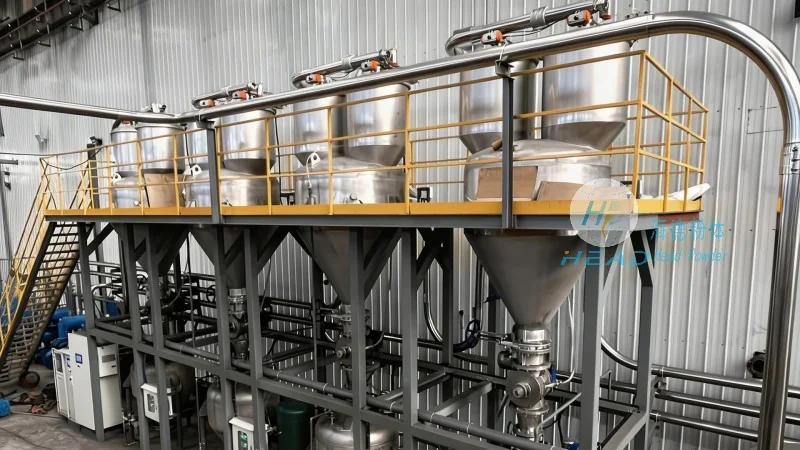
At the heart of a dry gravel material handling system are several key components that work in tandem to ensure smooth operation. The system typically includes a hopper or feed bin for material storage, a conveyor mechanism (such as a belt conveyor or screw conveyor) for transporting the material, and a discharge mechanism to release the material at the desired location. The design of each component is tailored to the specific characteristics of the gravel, such as particle size, moisture content, and bulk density. For instance, the hopper may be equipped with a vibratory feeder to ensure a consistent flow of material, preventing blockages and maintaining uniform conveyor speed.
Design Principles for Optimal Performance
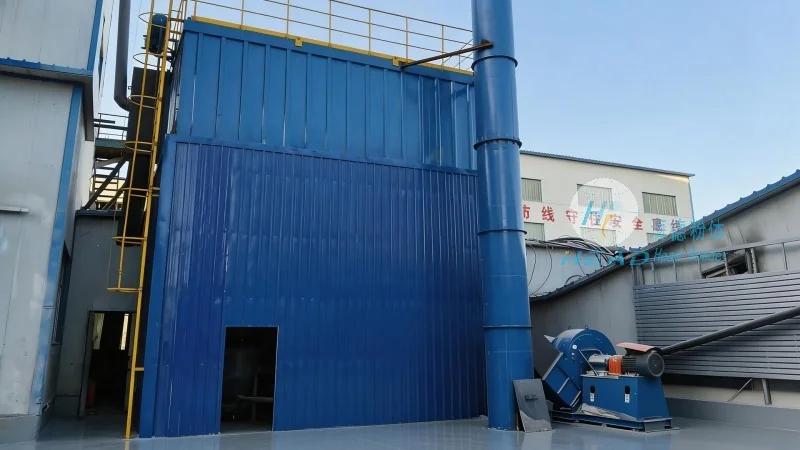
The design of a dry gravel material handling system follows several fundamental principles aimed at maximizing efficiency and minimizing operational issues. First, the system must be designed to handle the specific physical properties of the gravel, including its abrasiveness and potential for dust generation. Abrasive materials can cause wear on conveyor belts and other components, so materials like high-strength steel or polyurethane are often used for parts that come into direct contact with the gravel. Second, the system should be engineered to minimize material segregation, where larger or smaller particles separate during transport. This is achieved through proper hopper design and conveyor speed control, ensuring that all particles move at a consistent rate. Third, the system must incorporate dust control measures, as dry gravel can generate significant airborne dust, which poses health and safety risks. Common solutions include dust collection systems and enclosed conveyor sections.
Applications and Industry Impact
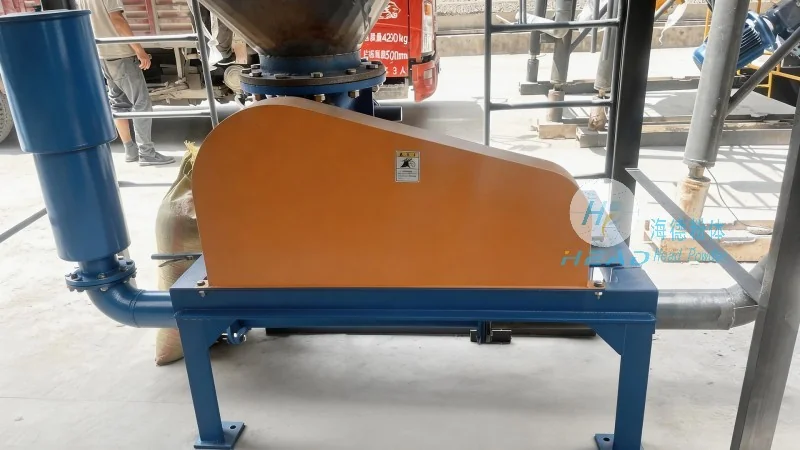
Dry gravel material handling systems are widely used in applications ranging from construction sites where gravel is used for base layers and drainage systems to mining operations where ore is processed and transported. In construction, these systems help streamline the process of moving large quantities of gravel, reducing the need for manual labor and minimizing the risk of accidents. In mining, they play a critical role in the extraction and processing of raw materials, ensuring that the material is handled safely and efficiently from the mine to the processing plant. The efficiency of these systems directly impacts project timelines and costs, making them an essential component of modern industrial operations.
Key Considerations for System Integration
When integrating a dry gravel material handling system into an existing workflow, several factors must be considered to ensure optimal performance. First, the system must be compatible with the existing infrastructure, including the layout of the facility and the power supply. This may require adjustments to the conveyor length or height to fit within the available space. Second, the system should be designed for easy maintenance and repair, as downtime can significantly impact productivity. Components such as bearings and conveyor belts should be easily accessible for inspection and replacement. Third, the system must comply with local safety regulations, particularly regarding dust control and material handling. This may involve installing safety guards and monitoring systems to prevent accidents and ensure compliance.
Conclusion: The Role of Shandong HeadPowder Engineering Co., Ltd.
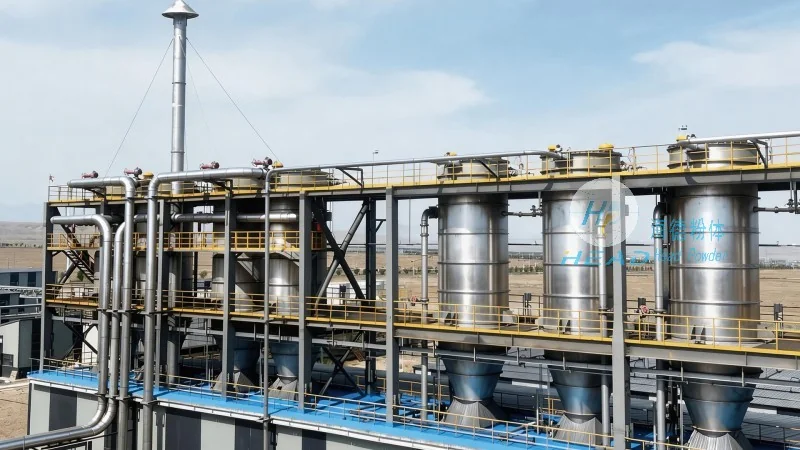
As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing dry gravel material handling systems tailored to the specific needs of various industries. With years of experience and a commitment to quality, headpowder has developed systems that meet the highest standards of efficiency, safety, and durability. By incorporating advanced design principles and using high-quality materials, their systems ensure reliable performance and minimal maintenance, making them a trusted choice for businesses in need of efficient gravel handling solutions. Based in Shandong, China, headpowder continues to innovate and improve its products to meet the evolving demands of the industry.