Calcined lime powder conveyors are critical equipment in industrial operations, especially for the handling and transportation of calcined lime—a vital material used across sectors like construction, chemical manufacturing, and environmental treatment. Grasping the working principle and key characteristics of these conveyors is essential for optimizing material flow and ensuring operational efficiency in industrial settings.
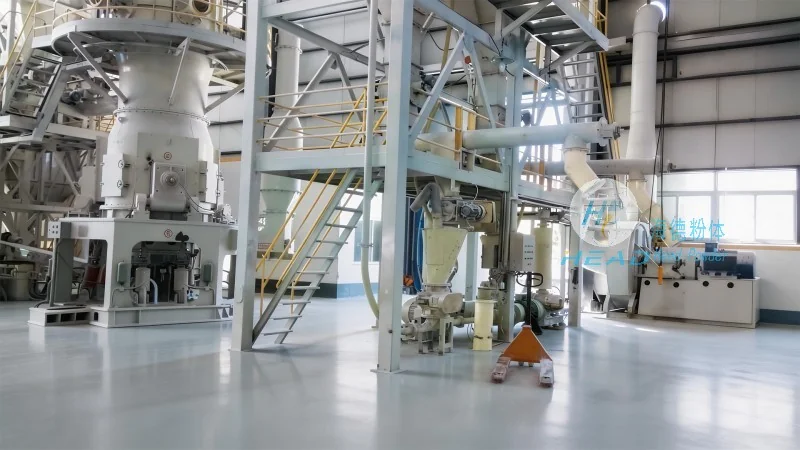
Calcined lime, also known as quicklime, is produced by heating limestone to high temperatures, resulting in a fine powder with high reactivity. The efficient transportation of this powder is crucial for maintaining production continuity and minimizing material loss. Calcined lime powder conveyors are engineered to handle this abrasive and reactive material while ensuring safe and reliable operation. The primary function of these systems is to move calcined lime from storage silos or processing units to downstream equipment such as reactors, mixers, or packaging units. This article explores the working principle and distinctive features of calcined lime powder conveyors, highlighting how they contribute to industrial productivity.
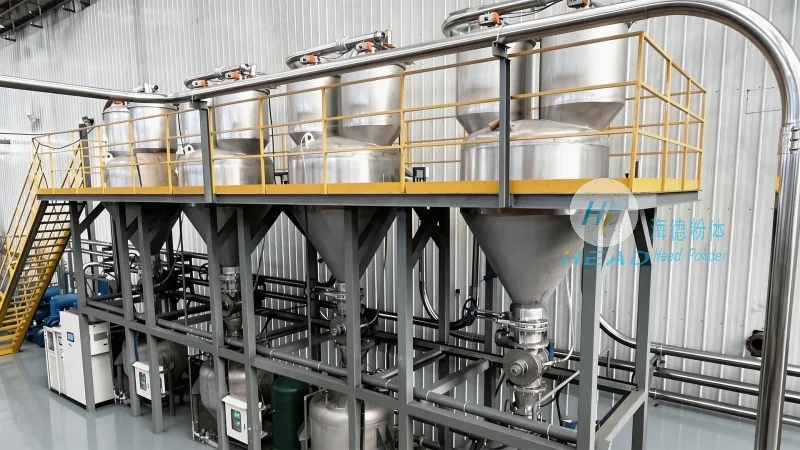
The working principle of calcined lime powder conveyors typically involves a combination of mechanical components that work in tandem to transport the material. The most common type is the pneumatic conveyor system, which utilizes compressed air to move the powder through a pipeline. In this system, the calcined lime is fed into a hopper or feeder, where it is then introduced into a pipeline. Compressed air is subsequently introduced into the pipeline, creating a flow that carries the powder particles forward. The velocity of the air and the size of the particles determine the efficiency of the transport. Another type is the mechanical conveyor, which employs a rotating screw or belt to move the material. This method is often used for shorter distances or when the material is less abrasive. The working principle of mechanical conveyors involves the rotation of a screw or belt, which pushes the powder along the conveyor path. Both systems are designed to handle the unique properties of calcined lime, such as its fine particle size and reactivity.
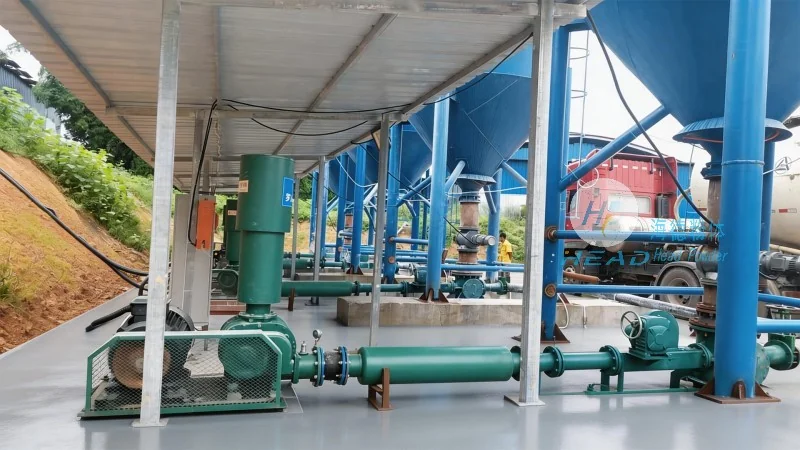
Calcined lime powder conveyors are equipped with several features that enhance their performance and reliability. One of the most important features is the material handling capability, which is tailored to the specific characteristics of calcined lime. These conveyors are designed to handle abrasive and reactive materials without causing damage to the equipment. The construction materials, such as stainless steel or corrosion-resistant alloys, are selected to withstand the chemical properties of calcined lime and prevent corrosion. Another key feature is the control system, which allows for precise regulation of the material flow. This system includes sensors and controls that monitor the pressure, flow rate, and temperature of the material, ensuring that the conveyor operates within safe and efficient parameters. The design also incorporates features for dust control and safety, such as explosion-proof components and dust collection systems. These features are essential for maintaining a safe working environment and complying with industrial safety regulations.
Calcined lime powder conveyors are widely utilized in various industries due to their ability to handle the unique properties of calcined lime. In the construction industry, these conveyors are used to transport calcined lime to concrete mixing plants, where it is used as a cement additive. In the chemical industry, they are used to transport calcined lime to reactors, where it is used in the production of calcium compounds. In the environmental industry, they are used to transport calcined lime to wastewater treatment plants, where it is used to neutralize acidic effluents. The benefits of using calcined lime powder conveyors include improved material flow, reduced material loss, and increased operational efficiency. These systems also help to minimize the risk of accidents and injuries by providing a safe and controlled environment for material handling.
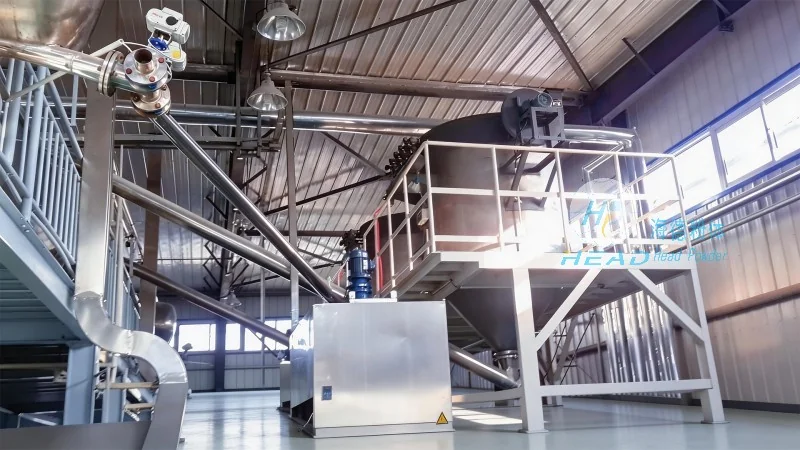
In conclusion, calcined lime powder conveyors are essential equipment for the efficient handling and transportation of calcined lime. The working principle of these systems involves the use of mechanical or pneumatic components to move the material through a pipeline or conveyor path. The key features of these conveyors include their ability to handle abrasive and reactive materials, precise control systems, and safety features. These features make calcined lime powder conveyors an ideal choice for various industrial applications. By understanding the working principle and features of these conveyors, industrial operators can optimize their material flow and ensure the smooth operation of their processes. The use of calcined lime powder conveyors contributes to increased productivity, reduced costs, and improved safety in industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top