Long-distance powder conveying systems are essential in various industrial applications, enabling the efficient and reliable transport of bulk powders over extended distances. These systems are designed to handle a wide range of materials, from fine powders to bulk solids, while maintaining high performance and operational safety. Understanding the working principle and key features of such equipment is crucial for selecting the right solution for specific industrial needs.
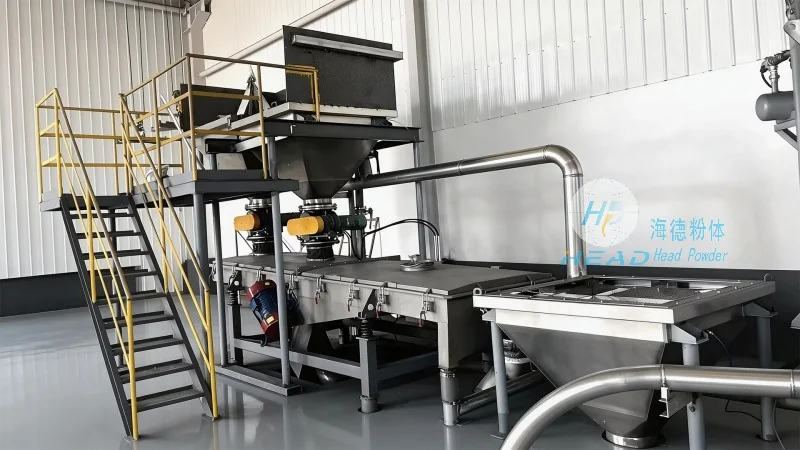
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and production of advanced powder conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to meet diverse client requirements. The company’s headquarters is located in Shandong, China, where state-of-the-art facilities and a team of experienced engineers ensure the delivery of high-performance equipment.
The core working principle of long-distance powder conveying systems involves the use of pressure differentials to move powders through a pipeline. There are primarily two types of systems based on this principle: positive pressure and negative pressure (or vacuum) systems. In positive pressure systems, a blower or compressor generates high-pressure air that forces the powder particles through the pipeline. The air and powder mixture is then separated at the discharge point, typically using a cyclone or filter. This method is suitable for conveying dry powders over long distances and is commonly used in industries such as cement, food, and chemical processing.
Negative pressure systems, on the other hand, create a vacuum in the pipeline to draw the powder from the source and transport it to the destination. The system uses a vacuum pump to maintain the low pressure, and the powder is carried by the air flow created by the vacuum. This approach is ideal for applications where dust control is critical, as it prevents the release of powders into the ambient air. The vacuum system is particularly effective for handling fine powders and materials that are prone to dusting.
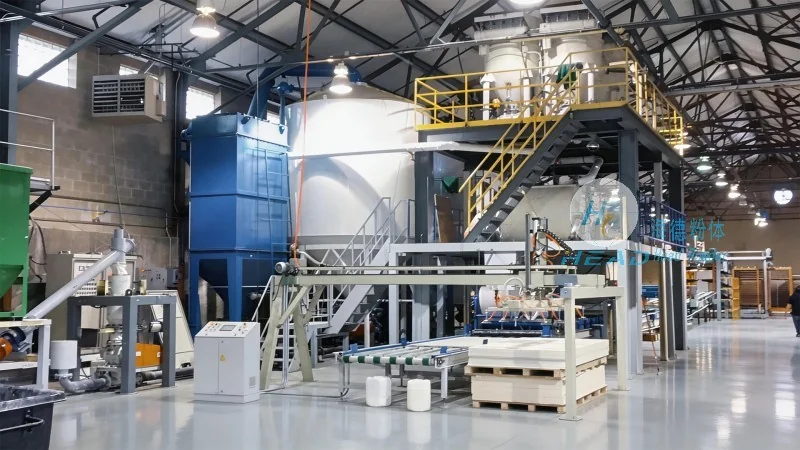
Long-distance powder conveying systems from Shandong HeadPowder Engineering Co., Ltd. are characterized by several key features that enhance their performance and reliability. One of the primary features is the high efficiency in material transport, which allows for significant reductions in labor costs and operational time compared to traditional methods like manual handling or bucket elevators. The systems are also designed for durability and low maintenance, ensuring long-term operational stability and minimal downtime.
Another important feature is the flexibility in material handling. The equipment can be adapted to transport various types of powders, including abrasive, corrosive, or temperature-sensitive materials, by selecting appropriate components such as special materials for the pipeline, seals, and valves. This adaptability makes the systems suitable for a wide range of industrial applications, from pharmaceuticals to mining.
Environmental considerations are also a critical feature of modern powder conveying systems. The equipment is designed to minimize dust emissions and ensure compliance with environmental regulations. Advanced filtration systems and sealed components help maintain a clean working environment, reducing the risk of respiratory issues for operators and minimizing the impact on the surrounding ecosystem.
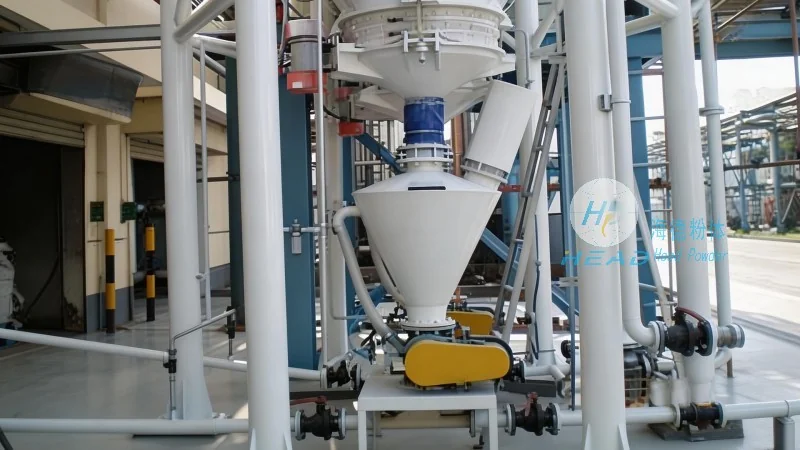
Implementing long-distance powder conveying systems offers numerous advantages for industrial operations. The most significant benefit is the improvement in operational efficiency, as the systems can transport large quantities of powders over long distances with minimal human intervention. This leads to increased productivity and reduced production costs. Additionally, the systems enhance safety by eliminating the need for manual handling of bulk materials, which reduces the risk of accidents and injuries.
Cost-effectiveness is another major advantage. While the initial investment in the equipment may be higher than traditional methods, the long-term savings in labor, material handling, and waste reduction make it a cost-effective solution. The systems also contribute to better process control, as they allow for precise control of the powder flow rate and pressure, ensuring consistent product quality.
Long-distance powder conveying systems are widely used in various industries, including cement production, food processing, chemical manufacturing, and mining. In the cement industry, these systems are used to transport raw materials and finished products over long distances within the plant. In the food industry, they are employed to convey ingredients such as flour, sugar, and spices, ensuring hygienic and efficient handling. The chemical industry utilizes these systems for transporting powders like fertilizers, pigments, and pharmaceuticals, where precise control and dust control are essential.
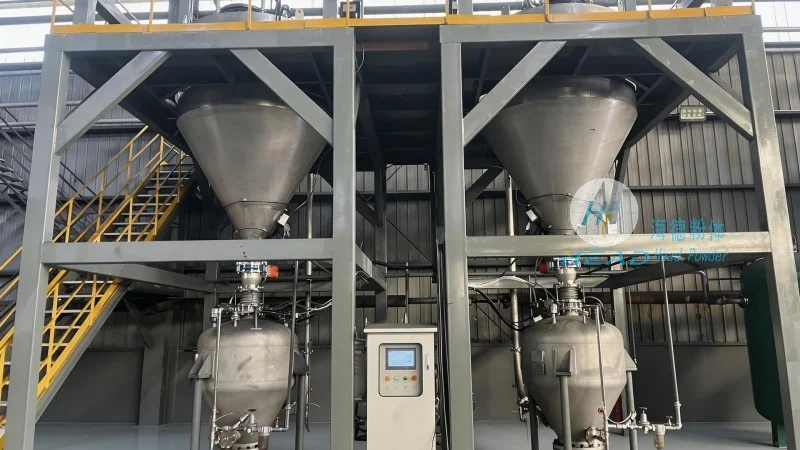
In the mining sector, long-distance powder conveying systems are used to transport ore and other bulk materials from mining sites to processing facilities. The systems are particularly beneficial in remote locations where traditional transport methods are impractical. The ability to handle abrasive and heavy materials makes them suitable for mining operations, contributing to improved productivity and reduced operational costs.
Shandong HeadPowder Engineering Co., Ltd. offers customized solutions to meet the specific needs of clients. The company works closely with customers to understand their operational requirements and design systems that are tailored to their processes. This includes selecting the appropriate type of conveying system (positive or negative pressure), pipeline materials, and accessories. The company also provides comprehensive after-sales support, including installation, training, and maintenance services, ensuring that clients can maximize the performance and lifespan of their equipment.
The commitment to quality and customer satisfaction is evident in the company’s approach to product development and service. By leveraging advanced technology and a team of experienced engineers, Shandong HeadPowder Engineering Co., Ltd. continues to provide reliable and efficient long-distance powder conveying systems that meet the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top