

Principle and Working Scene Characteristics of a Calcined Ash Material Pneumatic Conveying System
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for calcined ash materials. Our systems are engineered to meet the unique challenges of transporting high-temperature, abrasive, and often dusty calcined ash, ensuring efficient and reliable material handling in industrial applications.
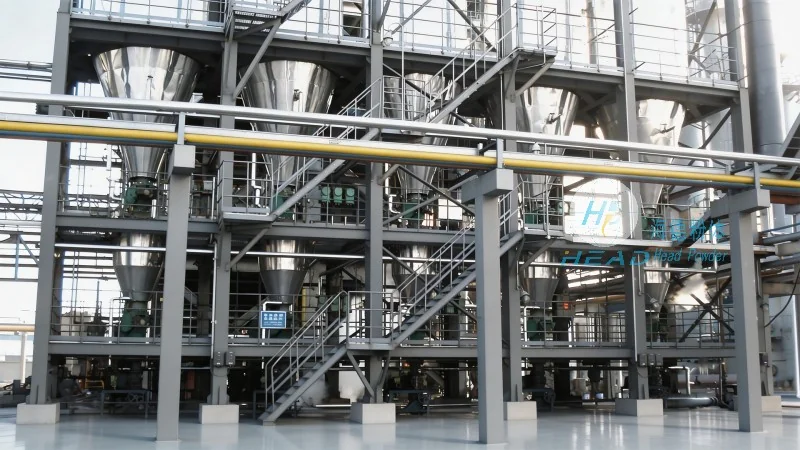
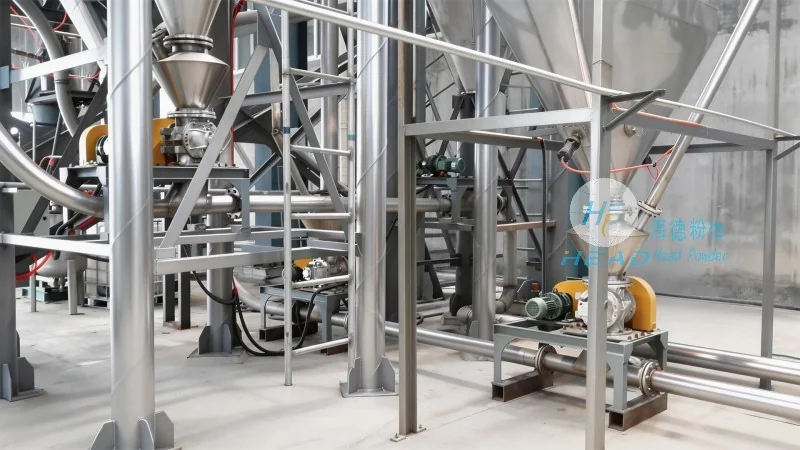
System Principle: The Core Technology Behind Efficient Material Transport
The pneumatic conveying system for calcined ash operates on the fundamental principle of using compressed air to transport bulk materials through a pipeline network. This technology, also known as pneumatic transport, involves the creation of a low-pressure or high-pressure air stream that propels the calcined ash particles through the system. The system typically comprises a series of components, including a material feeder, a conveying line, a separation unit, and a dust collection system. The material feeder ensures a consistent flow of calcined ash into the system, while the conveying line transports the material to the desired destination. The separation unit, often a cyclone or a baghouse, separates the material from the air stream, allowing for the collection of the calcined ash and the release of clean air back into the environment. This process minimizes material loss and ensures compliance with environmental regulations.
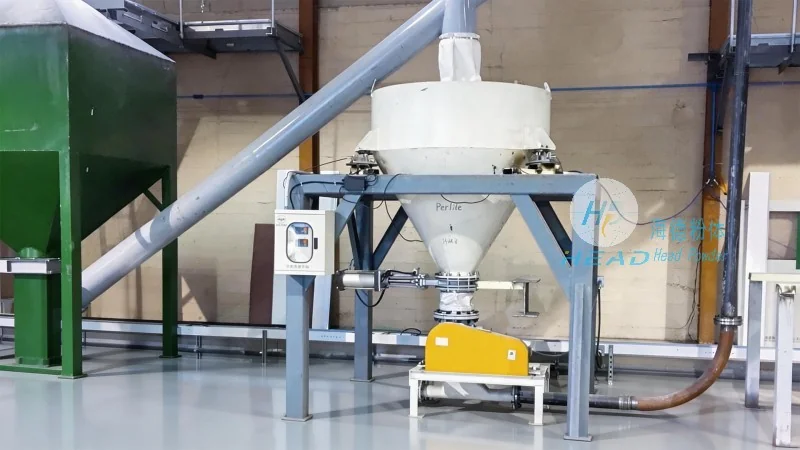
Working Scene Characteristics: Tailored Solutions for Diverse Industrial Needs
HeadPowder's calcined ash pneumatic conveying systems are designed to address the specific characteristics of calcined ash, which is a byproduct of the calcination process used in industries such as cement, steel, and power generation. Calcined ash is known for its high temperature, abrasive nature, and tendency to generate dust, making traditional material handling methods inefficient and potentially hazardous. Our systems are engineered to handle these challenges effectively. For instance, the system's components are constructed from corrosion-resistant and heat-resistant materials to withstand the high temperatures and abrasive properties of calcined ash. The design also incorporates features to minimize dust generation and ensure safe operation, such as sealed feeders and efficient dust collection systems. Additionally, the system's flexibility allows for adaptation to various working scenarios, including long-distance transport, vertical and horizontal conveying, and integration with existing industrial processes. This adaptability makes our systems suitable for a wide range of applications, from small-scale processing facilities to large-scale industrial plants.
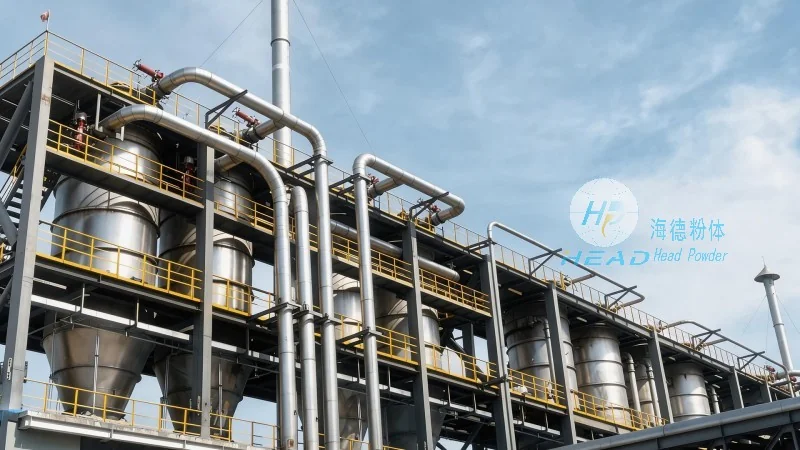
Product Introduction: Advanced Pneumatic Conveying Solutions for Calcined Ash
HeadPowder offers a comprehensive range of pneumatic conveying systems specifically designed for calcined ash materials. Our products are characterized by their high efficiency, reliability, and durability, making them ideal for demanding industrial environments. The system includes a material feeder that can handle high-temperature calcined ash, ensuring consistent material flow. The conveying line is constructed from high-quality materials that can withstand the abrasive nature of the material, reducing wear and tear and extending the system's lifespan. The separation unit is designed to effectively separate the calcined ash from the air stream, minimizing material loss and ensuring clean air discharge. Additionally, the system incorporates advanced control systems that allow for real-time monitoring and adjustment of the conveying process, enhancing operational efficiency and reducing downtime. Our calcined ash pneumatic conveying systems are fully compliant with international safety and environmental standards, providing customers with a reliable and sustainable solution for material handling.