

Principle and Working Scene Characteristics of Dusty Material Pneumatic Conveying Systems
HeadPowder, a leading provider in the field, specializes in the design and implementation of pneumatic conveying systems for handling dusty materials. These systems are engineered to efficiently transport bulk materials through a pipeline using air or other gas as the conveying medium. The core principle involves creating a flow of air that lifts and propels the material particles, ensuring smooth and reliable material transfer across various industrial applications.
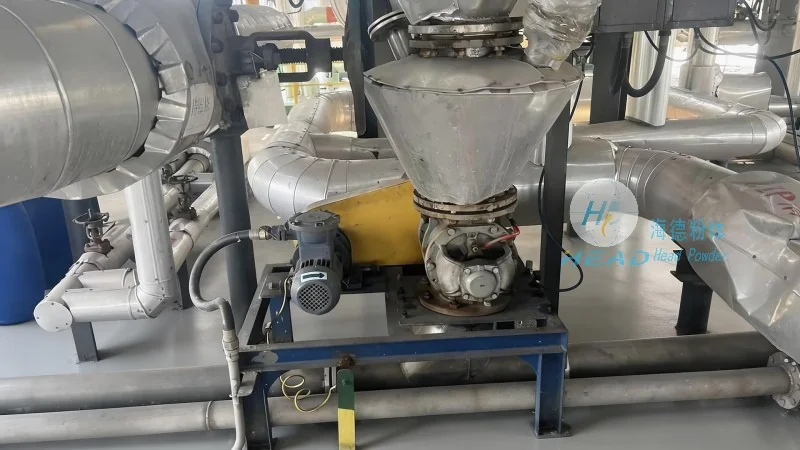
Key Principles of Pneumatic Conveying Technology
The fundamental principle of pneumatic conveying lies in the interaction between the material and the conveying air. By generating sufficient air velocity within the pipeline, the system can overcome the gravitational force acting on the material particles. This is achieved through either pressure or vacuum systems, depending on the specific requirements of the application. The pressure system uses compressed air to push the material forward, while the vacuum system draws the material into the pipeline using a suction mechanism. Both methods are designed to maintain a consistent flow rate and prevent material degradation or blockages.
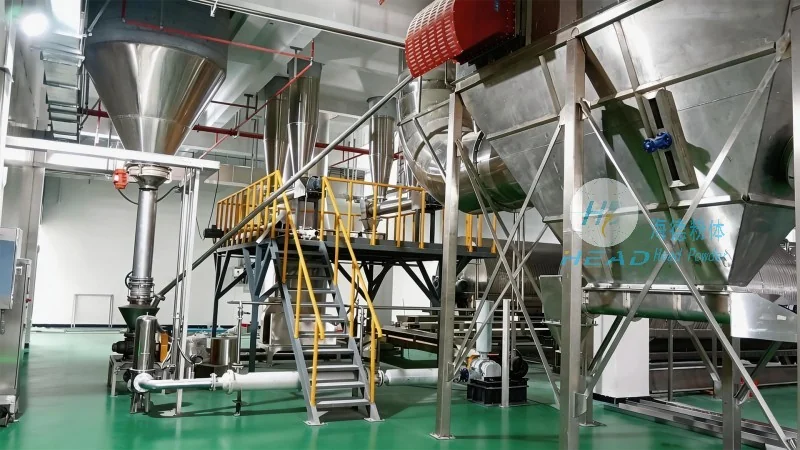
Working Scene Characteristics and Application Scenarios
The working scene characteristics of dusty material pneumatic conveying systems are tailored to meet the diverse needs of industrial environments. These systems are commonly employed in sectors such as mining, construction, food processing, and chemical manufacturing, where the handling of fine or abrasive materials is essential. The key characteristics include high efficiency in material transport, minimal maintenance requirements, and the ability to handle materials over long distances without the need for intermediate storage or transfer points.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, with its headquarters in Shandong, China, is a reputable company dedicated to providing advanced pneumatic conveying solutions. The company leverages years of industry experience to design customized systems that align with the specific operational needs of clients. By focusing on innovation and quality, HeadPowder ensures that its products meet the highest standards of performance and reliability, making them suitable for both new installations and system upgrades.
Technical Advantages and Operational Benefits
One of the primary advantages of pneumatic conveying systems is their ability to handle a wide range of materials, including powders, granules, and fine particles. This versatility makes them ideal for applications where traditional conveyor systems may be less effective or even impractical. Additionally, these systems offer significant operational benefits, such as reduced labor costs, improved safety by minimizing manual handling of materials, and enhanced process control through precise flow regulation. The systems are also designed to be energy-efficient, with optimized air usage that reduces operational expenses over time.
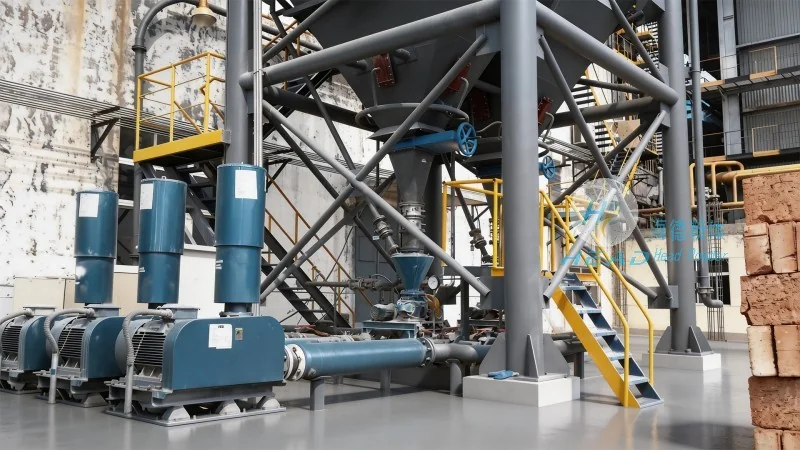
Customization and Integration Capabilities
HeadPowder understands that each industrial operation has unique requirements. Therefore, the company offers comprehensive customization options to ensure that the pneumatic conveying system integrates seamlessly with existing infrastructure and production processes. This includes the selection of appropriate pipeline materials, air pressure levels, and control systems tailored to the specific material characteristics and operational conditions. The company’s engineering team works closely with clients to assess their needs, develop tailored solutions, and provide ongoing support to ensure optimal system performance.