High-pressure bin pumps are a critical component in modern powder handling and material transport systems, designed to efficiently move bulk powders over long distances with high reliability. This article delves into the working principle and key features of the high-pressure bin pump powder conveying system, highlighting its applications and benefits in industrial settings.
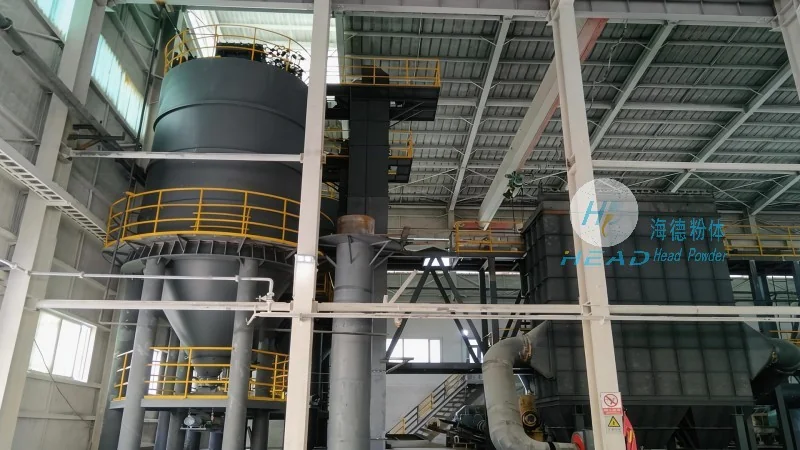
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and supply of advanced powder handling equipment. The high-pressure bin pump system is a core product line that addresses the challenges of transporting fine and cohesive powders, such as cement, coal, and chemical powders, with precision and efficiency. This system combines robust engineering with innovative technology to ensure consistent performance in demanding industrial environments.
The high-pressure bin pump operates on a positive displacement principle, utilizing a reciprocating piston or plunger mechanism to create high-pressure pulses that force the powder through a pipeline. The system typically consists of a hopper for material storage, a pump unit that generates the pressure, and a discharge valve that controls the flow. When the pump piston moves, it creates a vacuum in the hopper, drawing the powder into the pump chamber. As the piston returns, it compresses the powder, increasing the pressure and forcing it through the discharge line to the destination point. This cyclic motion ensures continuous and controlled powder transport, even for materials with low flowability or high moisture content.
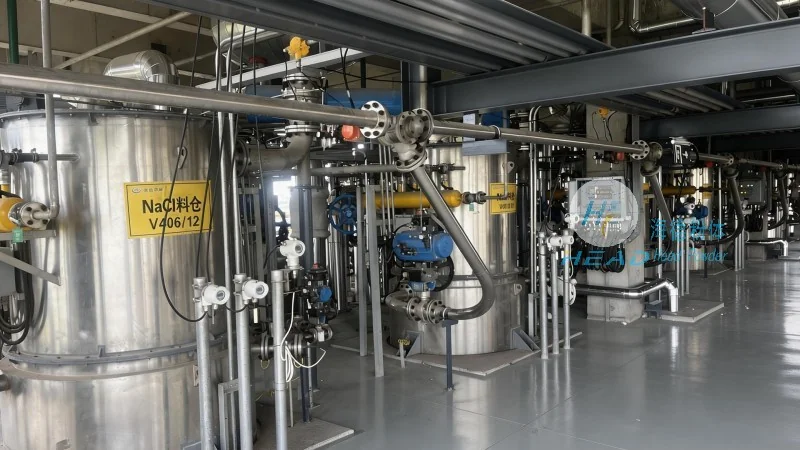
The high-pressure bin pump system from Shandong HeadPowder Engineering Co., Ltd. is characterized by several distinctive features that enhance its performance and usability. Firstly, it offers high conveying efficiency, capable of transporting powders at rates ranging from several tons per hour to over 100 tons per hour, depending on the system configuration. The system is also designed for long-distance transport, with the ability to cover distances of up to several kilometers without significant pressure loss. Another notable feature is its adaptability to various powder types, including fine, cohesive, and abrasive materials, thanks to the adjustable pump parameters and wear-resistant components. The system incorporates advanced control systems that allow for real-time monitoring of pressure, flow rate, and material level, ensuring optimal operation and minimizing downtime. Additionally, the design emphasizes safety and reliability, with built-in pressure relief valves and overload protection mechanisms to prevent equipment damage and ensure operator safety.
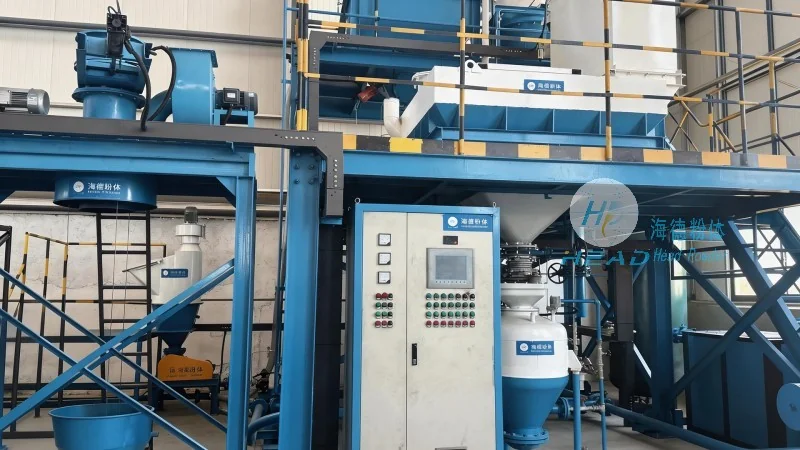
The high-pressure bin pump powder conveying system is widely used in industries such as cement production, coal handling, chemical processing, and food processing. In cement plants, it efficiently transports raw materials and finished products, reducing the need for manual handling and improving production throughput. In coal-fired power plants, the system ensures reliable coal delivery to boilers, enhancing energy generation efficiency. The system's ability to handle abrasive and corrosive materials makes it suitable for chemical processing facilities, where material compatibility is critical. The benefits of this system include increased productivity, reduced labor costs, improved material quality control, and enhanced safety in industrial operations. By leveraging the high-pressure bin pump technology, industries can achieve more efficient and sustainable powder handling solutions.
Shandong HeadPowder Engineering Co., Ltd. provides high-quality high-pressure bin pump powder conveying systems that combine advanced engineering with reliable performance. The system's working principle, based on positive displacement and high-pressure pulses, ensures efficient and consistent powder transport. Its key features, including high conveying efficiency, long-distance capability, adaptability to various materials, and advanced control systems, make it an ideal solution for industrial applications. With its headquarters in China, the company continues to innovate and deliver cutting-edge powder handling solutions to meet the evolving needs of global industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top