Stone and coal powder conveyors are essential equipment in the material handling industry, designed to efficiently transport bulk materials such as stone, coal powder, and other fine or granular substances. This article will explore the working principle and key features of these conveyors, providing a comprehensive understanding of their functionality and advantages.
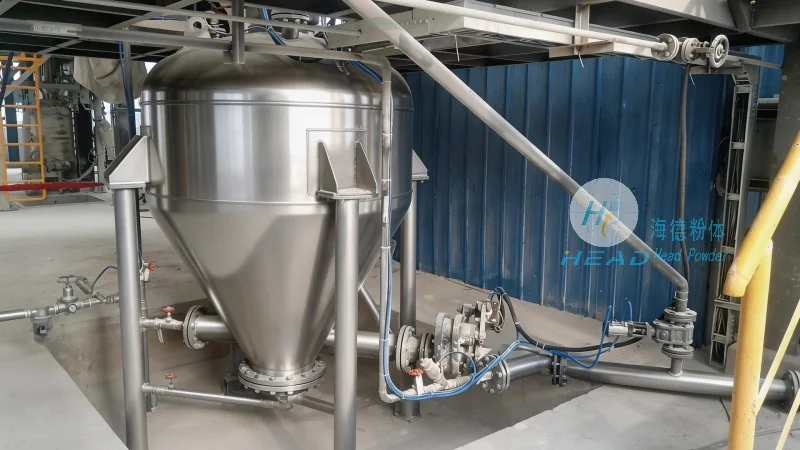
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of high-quality stone and coal powder conveying systems. Our conveyors are engineered to meet the diverse needs of industrial applications, ensuring reliable and efficient material transport. The following sections will delve into the operational mechanics and distinctive characteristics of these critical pieces of equipment.
The working principle of stone and coal powder conveyors typically involves a continuous belt or screw mechanism that moves materials from a loading point to a discharge point. The conveyor system consists of several key components, including a drive system, a conveyor belt or screw, a frame, and a control panel. When the system is activated, the drive motor powers the conveyor, causing the belt or screw to rotate. As the material is fed onto the conveyor, it is carried along the path by the moving surface, ensuring smooth and consistent transport. This mechanism allows for the efficient handling of bulk materials, reducing the need for manual labor and minimizing material loss.
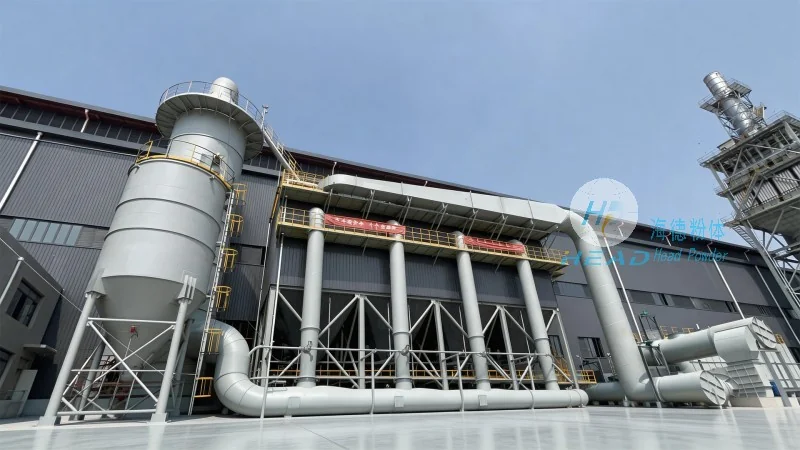
Stone and coal powder conveyors from HeadPowder are equipped with several features that enhance their performance and usability. One of the primary features is the adjustable speed control, which allows operators to modify the conveyor speed based on the material type and processing requirements. This flexibility ensures optimal material handling and prevents overloading or underloading of the system. Additionally, the conveyors are designed with durable materials, such as stainless steel or high-strength plastics, to withstand the abrasive nature of stone and coal powder, extending their service life and reducing maintenance costs.
Another notable feature is the integrated safety system, which includes emergency stop buttons and overload protection mechanisms. These features enhance workplace safety by preventing accidents and protecting the equipment from damage. The conveyors also feature easy-to-clean surfaces and modular components, facilitating maintenance and cleaning processes. Furthermore, the design allows for easy integration with other industrial equipment, such as crushers, screens, and storage silos, creating a seamless material handling workflow.
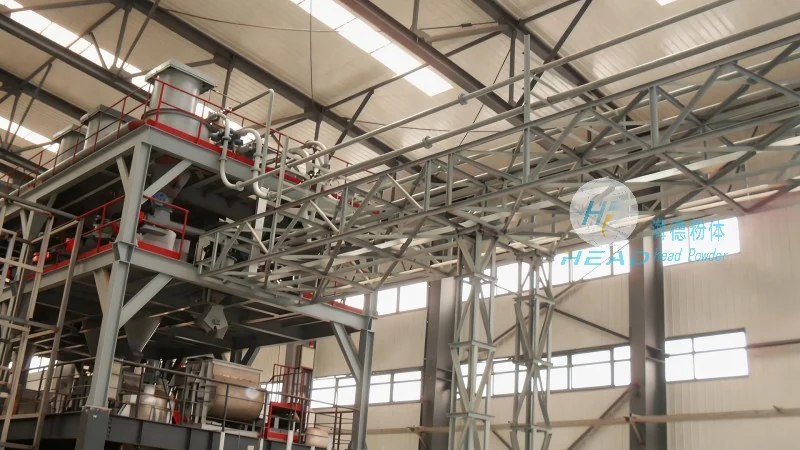
Stone and coal powder conveyors are widely used in various industries, including mining, power generation, and construction. In the mining industry, these conveyors are used to transport raw materials from mines to processing facilities, improving operational efficiency and reducing transportation costs. In power plants, they play a crucial role in transporting coal to boilers, ensuring a steady supply of fuel for energy production. In construction, they are utilized to move aggregates and other construction materials to job sites, supporting the construction process. The benefits of using these conveyors include increased productivity, reduced labor costs, improved material quality, and enhanced safety in the workplace.
Stone and coal powder conveyors are indispensable equipment in the material handling sector, offering efficient and reliable solutions for transporting bulk materials. HeadPowder, with its expertise and commitment to quality, provides top-tier conveyors that combine advanced technology with robust design. By understanding the working principle and features of these conveyors, industries can make informed decisions to enhance their material handling processes and achieve greater operational efficiency. For more information about our stone and coal powder conveying systems, please contact us at our headquarters in Shandong, China.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top