

Operation Process and Working Principle of Activated Carbon Powder Pneumatic Conveying System
The activated carbon powder pneumatic conveying system is a specialized industrial equipment designed for the efficient and safe transportation of activated carbon powder. This system is widely used in various industries such as water treatment, air purification, and chemical processing, where the reliable and low-loss transfer of activated carbon powder is crucial. The system operates by using compressed air to move the powder through a pipeline network, ensuring minimal product degradation and contamination. As a key component in many industrial processes, understanding its operation process and working principle is essential for optimizing performance and maintaining system efficiency.
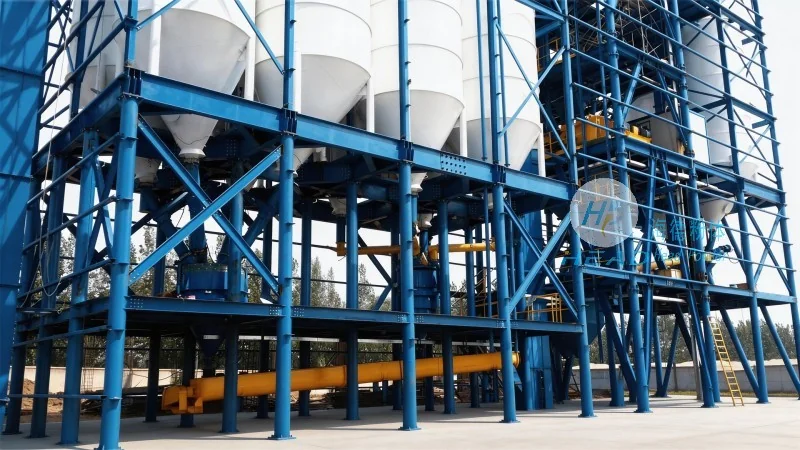
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced pneumatic conveying systems, with a strong focus on activated carbon powder handling solutions. The company is headquartered in Shandong, China, and has established itself as a trusted partner for businesses seeking high-quality, reliable equipment for their material handling needs. With years of experience in the industry, HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems that meet the specific requirements of different applications, ensuring optimal performance and durability. The company's commitment to quality and innovation has made it a preferred choice for clients worldwide.
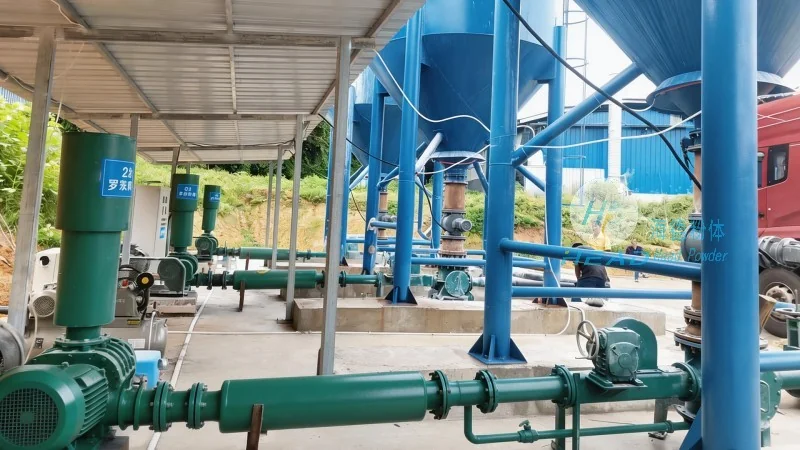
Key Components of the Pneumatic Conveying System
The activated carbon powder pneumatic conveying system consists of several key components that work together to ensure efficient operation. These components include the hopper, which stores the activated carbon powder; the feeder, which controls the flow of powder into the system; the air compressor, which provides the necessary compressed air; the pipeline network, which transports the powder from the source to the destination; and the receiver, which collects the powder at the end of the line. Each component plays a critical role in the overall system performance, and proper maintenance and operation are essential to ensure smooth and continuous operation.
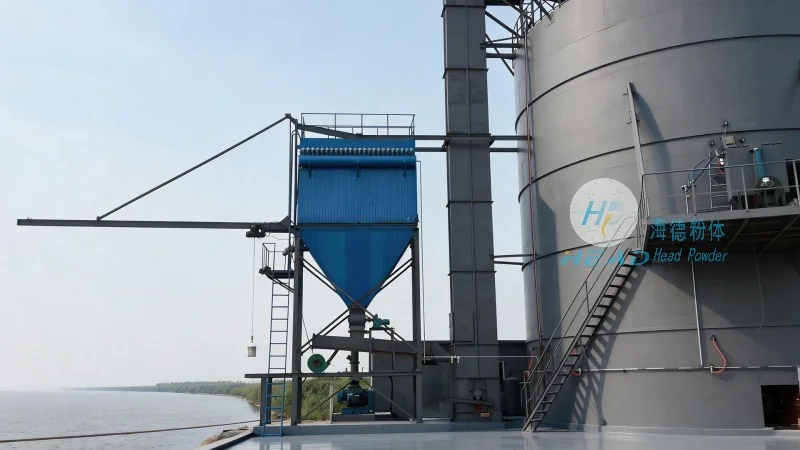
Operation Process of the Pneumatic Conveying System
The operation process of the activated carbon powder pneumatic conveying system begins with the loading of activated carbon powder into the hopper. The feeder then regulates the flow of powder, ensuring a consistent and controlled rate of material discharge. The air compressor generates compressed air, which is then introduced into the pipeline system. As the compressed air flows through the pipeline, it creates a pressure differential that lifts the activated carbon powder and propels it through the system. The powder is carried along the pipeline by the air stream, reaching the receiver where it is collected. The system operates continuously, with the air compressor maintaining the necessary pressure to keep the powder in motion. The entire process is automated, with sensors and controls monitoring the system parameters to ensure optimal performance and prevent any potential issues.
Working Principle of the Pneumatic Conveying System
The working principle of the activated carbon powder pneumatic conveying system is based on the principle of fluidization and pneumatic transport. The system uses compressed air to create a fluidized bed of activated carbon powder in the hopper, which allows the powder to flow freely and be discharged by the feeder. The compressed air then enters the pipeline, where it creates a high-velocity air stream that entrains the powder particles and transports them to the receiver. The key to the system's efficiency is the balance between the air flow rate and the powder flow rate, which must be carefully controlled to prevent excessive pressure drop or material degradation. The system operates under positive pressure, which helps to maintain the integrity of the powder and prevent contamination from external sources. By understanding the working principle of the system, operators can optimize the system parameters to achieve the best possible performance and minimize energy consumption.
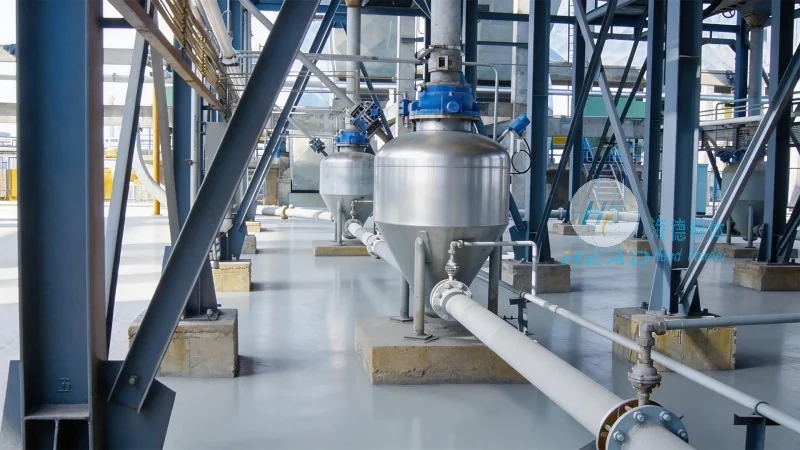
Benefits and Applications of the Pneumatic Conveying System
The activated carbon powder pneumatic conveying system offers several benefits that make it an ideal choice for many industrial applications. One of the main benefits is its ability to transport activated carbon powder efficiently and with minimal product loss. The system also reduces the risk of dust contamination and improves safety in the workplace. Additionally, the system is flexible and can be customized to meet the specific needs of different applications, making it suitable for a wide range of industries. The system is commonly used in water treatment plants for the transportation of activated carbon for filtration processes, in air purification systems for the handling of activated carbon for odor control, and in chemical processing plants for the transfer of activated carbon for various chemical reactions. The benefits of the system include increased productivity, reduced labor costs, and improved product quality.