Introduction to Automatic Tonne Bag Feeding Pneumatic Conveying Equipment: Structure and Working Pri
Automatic tonne bag feeding pneumatic conveying equipment is a specialized industrial device designed to efficiently handle bulk materials from large bulk bags (tonne bags) into processing systems. This equipment is widely used in various industries such as food, chemical, pharmaceutical, and mining, where reliable and hygienic material transfer is critical. The system integrates advanced automation and pneumatic technology to streamline the material handling process, reducing manual labor and enhancing operational efficiency.
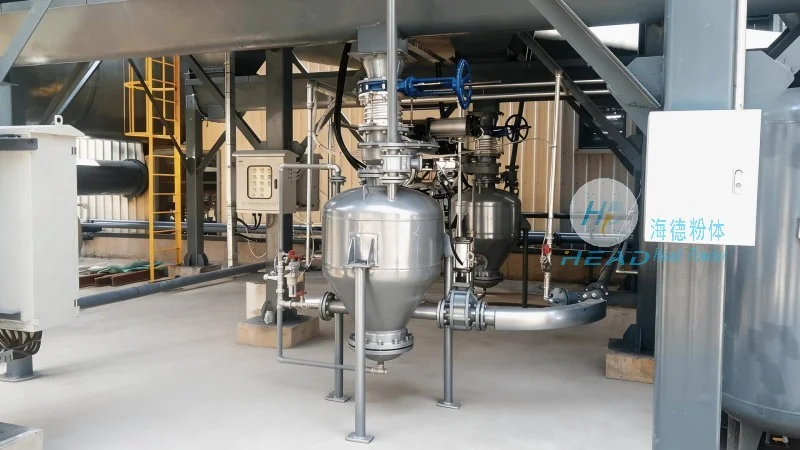
Key Components and Structure of the Equipment
The automatic tonne bag feeding pneumatic conveying system typically consists of several core components that work in concert to achieve seamless material transfer. The primary components include the bulk bag discharger, the pneumatic conveying line, the material receiver, and the control system. The bulk bag discharger is responsible for opening the tonne bag and releasing the material into the conveying line. This component often features a hopper or a feeding chute that connects directly to the pneumatic system. The pneumatic conveying line, which may be a positive or negative pressure system, transports the material from the discharger to the receiver. The material receiver, such as a silo or a storage tank, collects the conveyed material. The control system, which can be automated or semi-automated, manages the entire process, including bag opening, material discharge, and system shutdown. Each component is engineered to ensure durability, reliability, and compatibility with a wide range of bulk materials, including powders, granules, and fine particles.
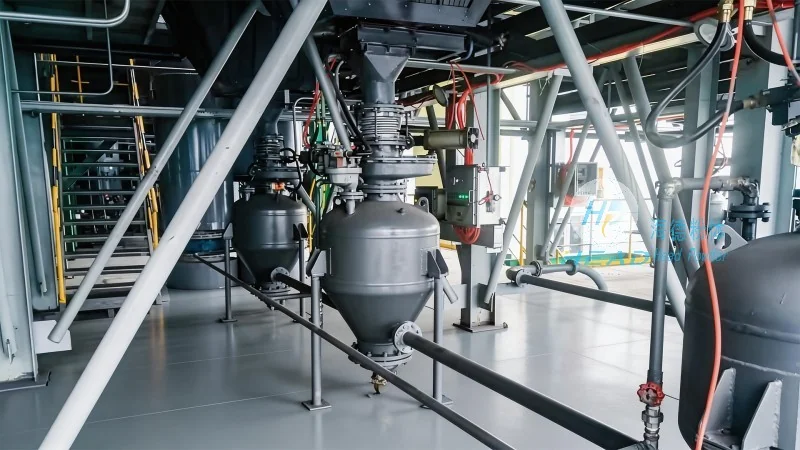
Working Principle of the Pneumatic Conveying Process
The operation of the automatic tonne bag feeding pneumatic conveying equipment is based on the principles of pneumatic transport, which involves the use of air to move material through a pipeline. The system can operate under either positive pressure or negative pressure, depending on the specific application and material characteristics. In a positive pressure system, air is blown into the conveying line, creating a pressure higher than the ambient air, which forces the material to move. In a negative pressure system, air is drawn out of the line, creating a vacuum that pulls the material. The bulk bag discharger plays a crucial role by providing a controlled flow of material into the conveying line. The material is first discharged from the tonne bag into the hopper, where it is then drawn into the conveying line by the air flow. The air velocity and pressure are carefully controlled to prevent material degradation, blockages, or excessive wear on the system components. The control system monitors the flow rate, pressure, and other parameters to ensure optimal performance and safety. This integrated approach ensures that the material is transferred efficiently and safely from the tonne bag to the processing equipment.
Advantages and Applications in Industrial Settings
The automatic tonne bag feeding pneumatic conveying equipment offers several advantages that make it a preferred choice for industrial material handling. One of the key benefits is its ability to handle large volumes of material from tonne bags, which are commonly used for bulk storage and transportation. This reduces the need for manual handling of heavy bags, minimizing the risk of injury and improving workplace safety. The system also enhances operational efficiency by automating the material transfer process, reducing downtime and labor costs. Additionally, the equipment is designed to be hygienic and clean, making it suitable for industries where product contamination is a concern, such as food and pharmaceuticals. The pneumatic conveying system can be easily integrated with existing processing lines, providing a seamless transition from material receipt to processing. The equipment is also versatile, capable of handling a wide range of materials, including powders, granules, and fine particles, with minimal modifications. In the food industry, for example, the system can be used to transfer ingredients like flour, sugar, or spices from bulk bags into production lines. In the chemical industry, it can handle raw materials such as powders or granules for manufacturing processes. The mining industry also benefits from this equipment, as it can efficiently transport ore or other minerals from storage bags to processing equipment. Overall, the automatic tonne bag feeding pneumatic conveying equipment provides a reliable and efficient solution for bulk material handling, improving productivity and reducing operational costs.
Company Information and Technical Support
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling equipment, specializes in the design, manufacturing, and supply of automatic tonne bag feeding pneumatic conveying systems. The company, commonly known as headpowder, is based in Shandong, China, and has a strong reputation for producing high-quality, reliable equipment tailored to the needs of various industries. The company's products are engineered with advanced technology and robust materials to ensure durability and long-term performance. HeadPowder provides comprehensive technical support and after-sales service to its customers, including installation assistance, maintenance guidance, and troubleshooting. The company also offers customization options to meet specific customer requirements, such as different material handling capacities, bag sizes, or integration with existing systems. With a focus on quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. is committed to delivering innovative and efficient material handling solutions that enhance industrial productivity and safety.