

Pneumatic Conveying Technology for Carbon Black Powder: Principles, Applications, and Development Trends
HeadPowder, a leading enterprise in the field of carbon black powder handling and processing, specializes in advanced pneumatic conveying solutions tailored for the efficient and reliable transport of carbon black powder. With a strong presence in Shandong, China, the company has established itself as a trusted provider of industrial conveying systems designed to meet the unique demands of the carbon black industry.
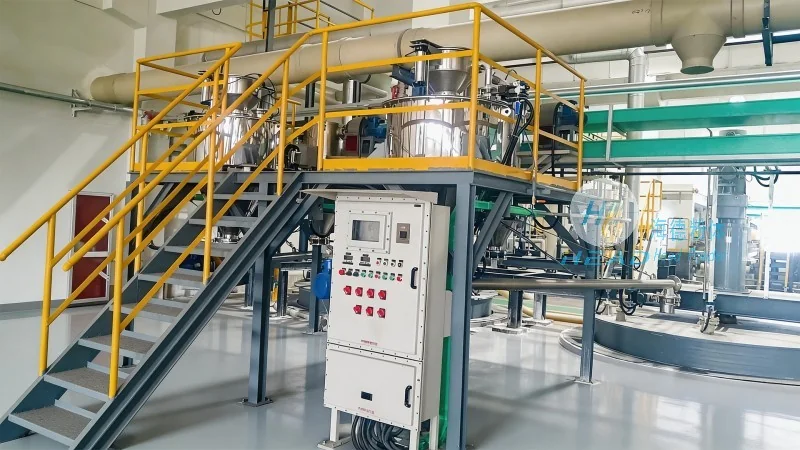
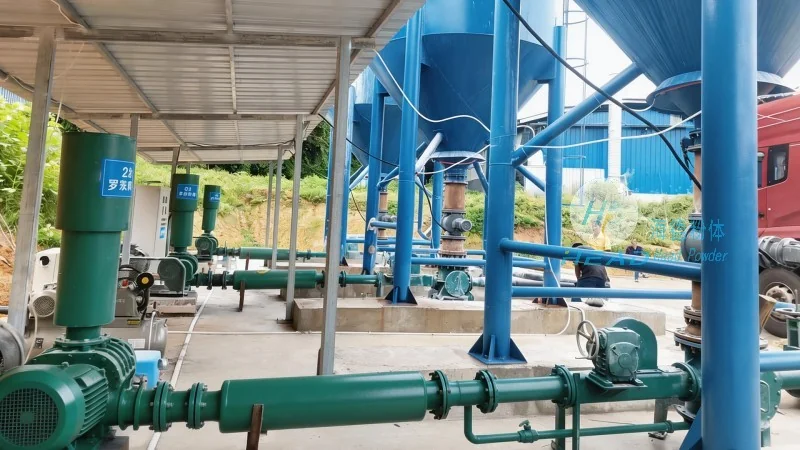
Understanding Pneumatic Conveying for Carbon Black Powder
Pneumatic conveying technology involves the use of air or gas to transport bulk materials like carbon black powder through a pipeline system. This method offers several advantages over traditional mechanical conveying, including reduced material degradation, lower maintenance requirements, and the ability to handle materials in a closed system, minimizing dust emissions and environmental impact. The core principle of pneumatic conveying is the creation of a pressure differential that propels the powder through the pipeline, ensuring smooth and consistent flow.
Key Principles of Carbon Black Powder Pneumatic Conveying
The effectiveness of carbon black powder pneumatic conveying relies on several fundamental principles. First, the selection of the appropriate conveying system type—such as pressure or vacuum systems—depends on factors like the distance, material characteristics, and desired flow rate. Pressure systems use compressed air to push the material, while vacuum systems draw it using a vacuum pump. Another critical principle is the design of the pipeline and components, including the use of appropriate pipe diameters, bends, and filters to prevent blockages and ensure consistent performance. The choice of air velocity is also crucial; it must be high enough to maintain the powder in suspension but low enough to avoid excessive wear on the system components.
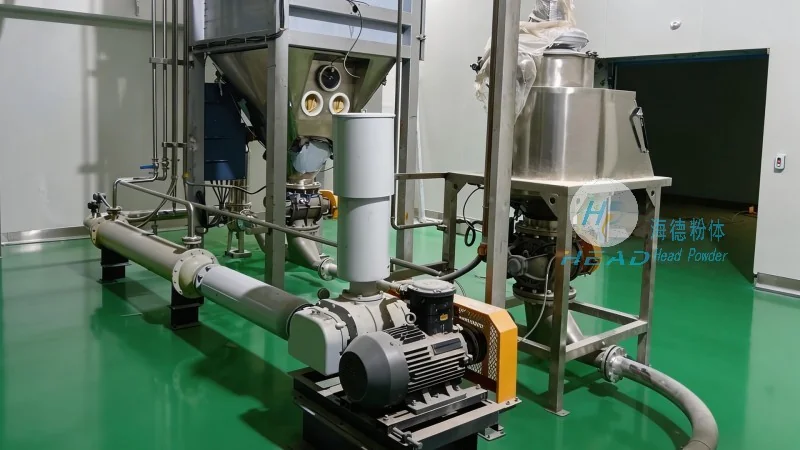
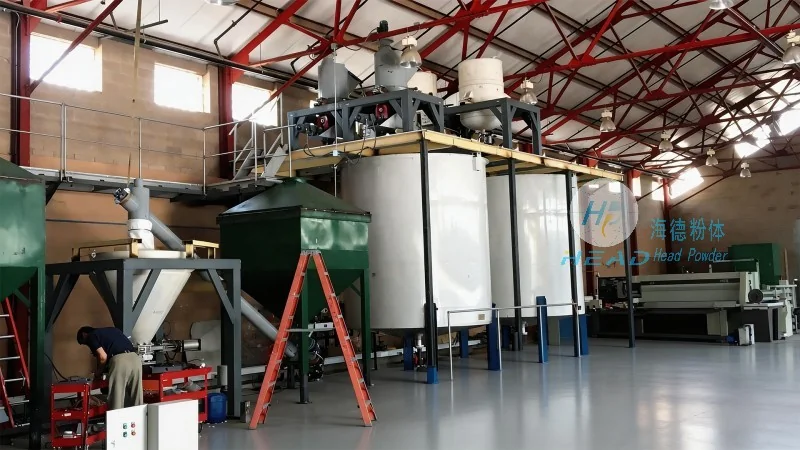
Applications of Pneumatic Conveying in Carbon Black Processing
Carbon black powder pneumatic conveying is widely used across various stages of the carbon black production and processing chain. In manufacturing facilities, it is employed to transport raw carbon black from storage silos to processing units, ensuring a continuous supply without interruptions. During the mixing and compounding stages, pneumatic conveying systems efficiently deliver carbon black to mixing equipment, maintaining precise dosage and preventing contamination. Additionally, in applications involving downstream processing, such as pelletizing or packaging, the technology ensures that carbon black is transferred to packaging units with minimal loss and maximum efficiency. The versatility of pneumatic conveying makes it suitable for both small-scale and large-scale operations, adapting to the varying needs of different industrial settings.