

Rice Technical Parameters and Conveying System Process
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced rice processing technologies. The company's core focus is on optimizing the entire rice production chain, from field to mill, by integrating precise technical parameters with efficient conveying systems. This approach ensures that every stage of rice handling, from harvesting to final product packaging, operates at peak efficiency and minimal energy consumption.
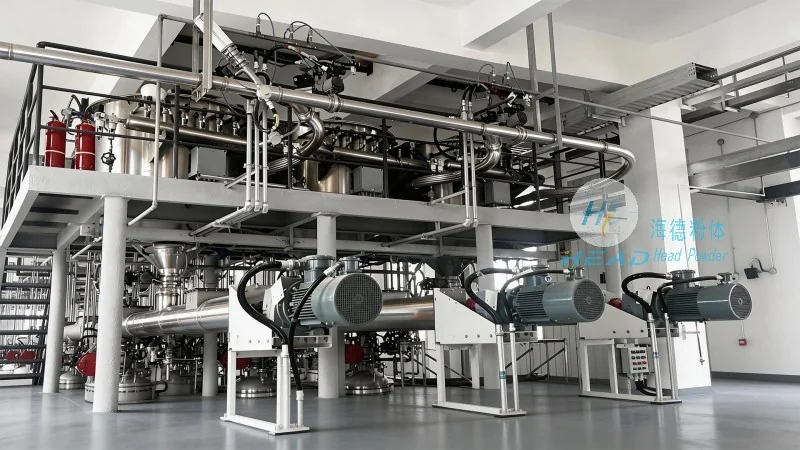
The conveying system is a critical component of modern rice processing facilities. It must handle various types of rice, including paddy, husked rice, and milled white rice, while maintaining consistent flow rates and preventing material loss. HeadPowder engineers have developed specialized conveyor designs that incorporate adjustable speed controls, material separation mechanisms, and durable construction materials to withstand the rigors of continuous operation. These systems are engineered to minimize downtime and maximize throughput, which are essential for maintaining profitability in the competitive rice market.
Technical parameters play a pivotal role in the performance of rice conveying systems. Key parameters include grain size distribution, moisture content, and bulk density, all of which directly impact the system's efficiency. HeadPowder employs advanced measurement and control technologies to monitor these parameters in real-time. For instance, sensors are integrated into the conveyor to detect changes in grain size or moisture levels, triggering automatic adjustments to the conveyor speed or feeding rate. This dynamic control ensures that the system operates within optimal conditions, preventing issues such as blockages or material degradation.
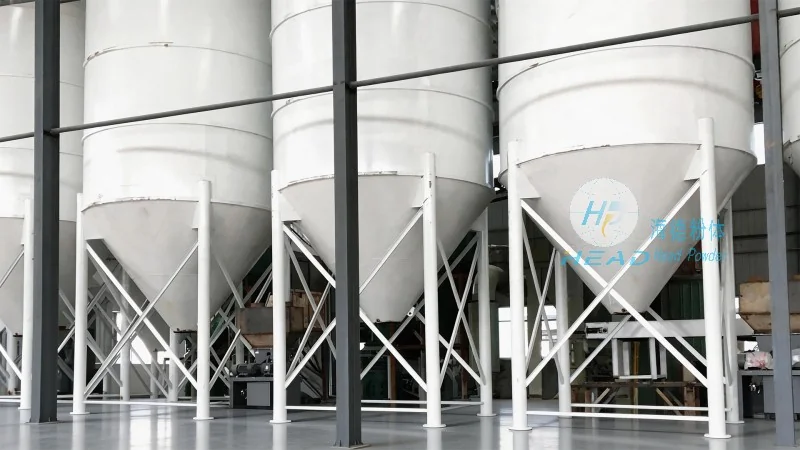
Another critical technical parameter is the system's energy efficiency. Modern rice processing facilities are under increasing pressure to reduce operational costs and environmental impact. HeadPowder's conveying systems are designed with energy-saving features, such as variable frequency drives (VFDs) that adjust motor speed based on the load. This not only reduces electricity consumption but also extends the lifespan of the motor and other components. The company also incorporates energy recovery systems in some designs, where excess energy from the conveyor is recycled to power other parts of the processing plant.
The design of the conveying system also considers the physical properties of rice. For example, paddy rice is typically more fragile and prone to breakage than milled rice. HeadPowder's engineers have developed specialized conveyor belts and troughs with gentle curves and low friction surfaces to minimize grain damage. This is particularly important for premium rice varieties, where maintaining grain integrity is crucial for market value. The system also includes cleaning mechanisms to remove debris and foreign materials that could contaminate the rice, ensuring product quality and compliance with industry standards.
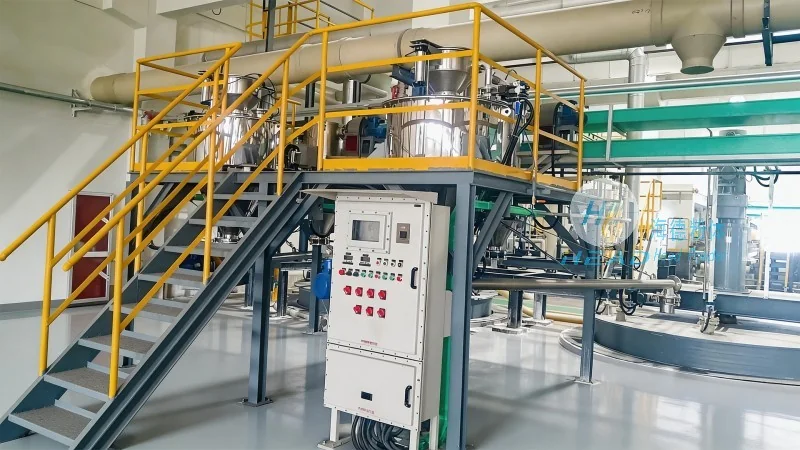
Integration with other processing equipment is another key aspect of the conveying system's design. HeadPowder's solutions are engineered to seamlessly connect with rice milling machines, storage silos, and packaging lines. This integration allows for a smooth flow of materials throughout the production process, reducing manual handling and the risk of human error. The system's control panel provides operators with real-time data on production rates, material levels, and system performance, enabling quick decision-making and troubleshooting.
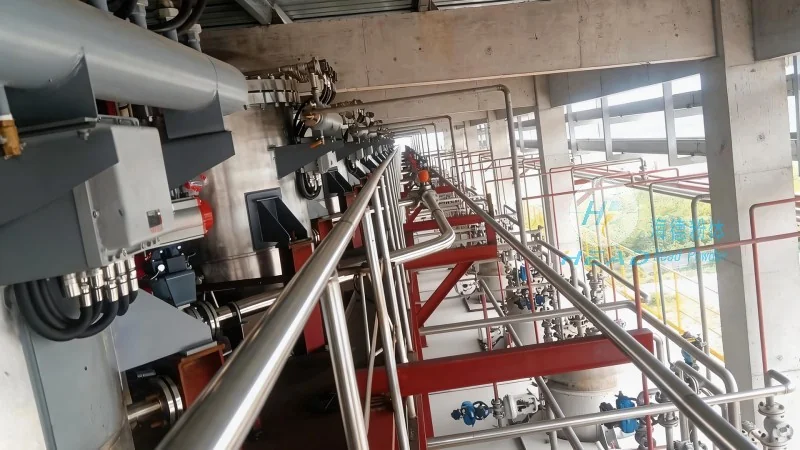
HeadPowder's commitment to innovation is evident in its approach to conveying system technology. The company continuously researches and develops new materials and designs to improve system performance. For example, recent advancements include the use of food-grade stainless steel in conveyor components, which enhances hygiene and durability. Additionally, the company has adopted digitalization and IoT (Internet of Things) technologies to enhance system monitoring and predictive maintenance. Sensors and data analytics are used to predict potential equipment failures, allowing for proactive maintenance and minimizing unplanned downtime.
In conclusion, the combination of precise technical parameters and advanced conveying systems is essential for efficient rice processing. HeadPowder's expertise in this field ensures that rice producers can optimize their operations, reduce costs, and maintain high product quality. By focusing on the specific needs of the rice industry, the company provides tailored solutions that meet the demands of modern rice processing facilities.