

What is a dust-free unpacking material conveyor line? What are its design principles?
Understanding the dust-free unpacking material conveyor line is crucial for industries that require stringent contamination control, such as pharmaceuticals, food processing, and electronics manufacturing. This specialized equipment is designed to transport bulk materials from packaging containers into processing or storage areas without introducing contaminants. The following sections will explore the fundamental aspects of this technology, including its design principles and practical applications.
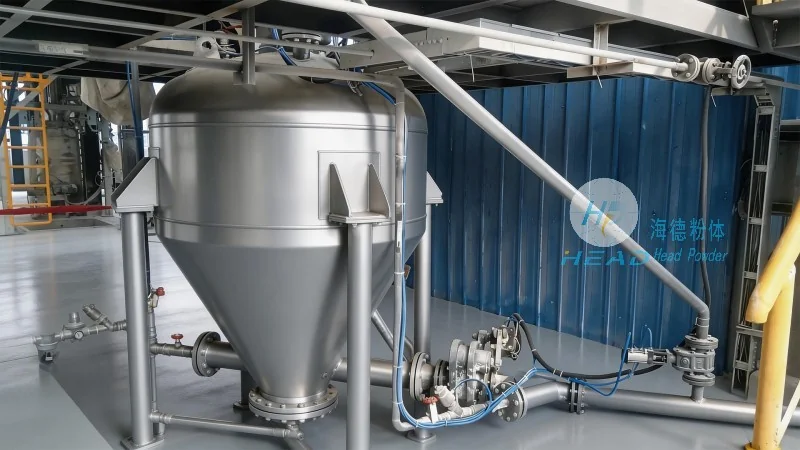
Introduction to Dust-Free Unpacking Material Conveyor Lines
A dust-free unpacking material conveyor line is a sophisticated system engineered to transport bulk materials from packaging containers into processing or storage areas without introducing contaminants. The primary goal is to ensure that the materials remain free from dust, particles, or other pollutants throughout the handling process. This is achieved through a combination of advanced mechanical components, filtration systems, and enclosed structures that create a controlled environment. The system typically includes components like hopper feeders, conveyor belts or rollers, dust collection units, and air filtration systems, all integrated to work in harmony to maintain a cleanroom-like atmosphere.
Key Design Principles of the Dust-Free Conveyor Line
The design of a dust-free unpacking material conveyor line is governed by several critical principles aimed at minimizing contamination and maximizing efficiency. First, the system must incorporate robust sealing mechanisms to prevent external dust from entering and internal dust from escaping. This often involves using airtight enclosures, gaskets, and sealed joints that create a negative pressure or positive pressure environment, depending on the application. Second, the material handling components are designed to minimize friction and particle generation. For example, smooth, non-porous surfaces on conveyor belts and rollers reduce the risk of dust shedding, while adjustable feed mechanisms ensure consistent material flow without causing excessive vibration or abrasion.
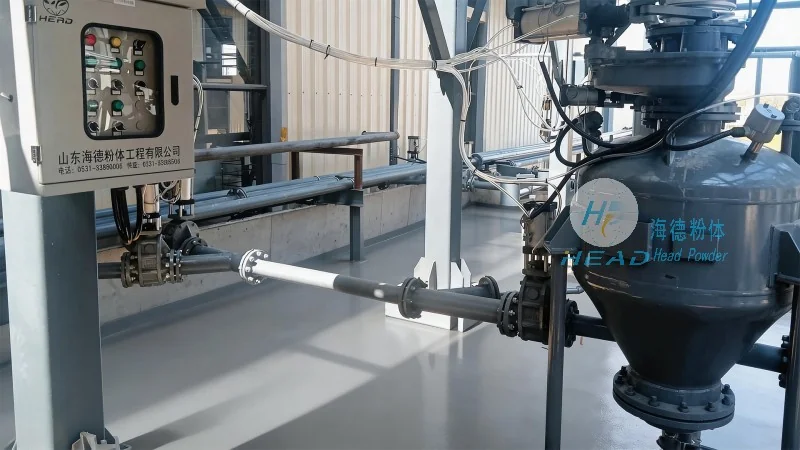
Third, advanced filtration and air purification systems are integral to the design. These systems typically include high-efficiency particulate air (HEPA) filters or similar technologies that capture and remove airborne particles before they can contaminate the workspace or product. The air is often recirculated within the enclosure, filtered, and then reintroduced, maintaining a consistent clean air quality. Additionally, the conveyor line may be equipped with dust collection hoppers or vacuum systems that capture any dust generated during the unpacking process, preventing it from dispersing into the environment.
Components and Functionality of the Conveyor Line
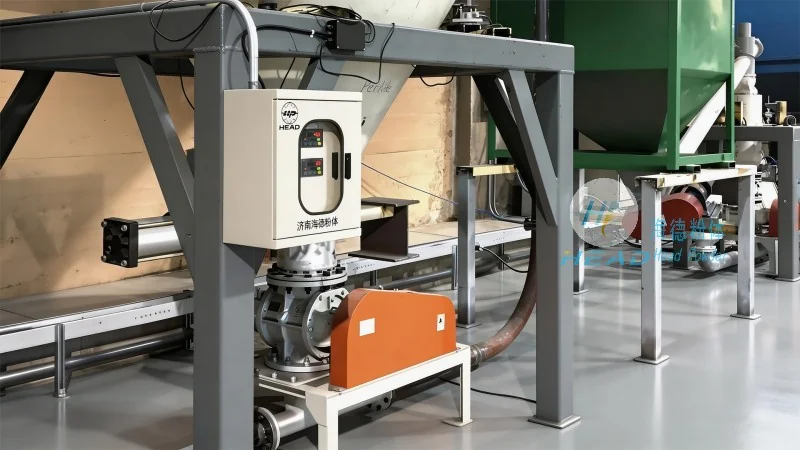
The functionality of a dust-free unpacking material conveyor line relies on a series of interconnected components, each playing a vital role in the overall operation. The initial stage involves the hopper or container where the bulk material is stored. This container is usually equipped with a lid or cover that seals tightly to prevent dust from escaping. The material is then transferred to a feeder, which may be a rotary valve, screw conveyor, or vibratory feeder, depending on the material's characteristics. The feeder regulates the flow of material into the conveyor system, ensuring a consistent and controlled feed rate.
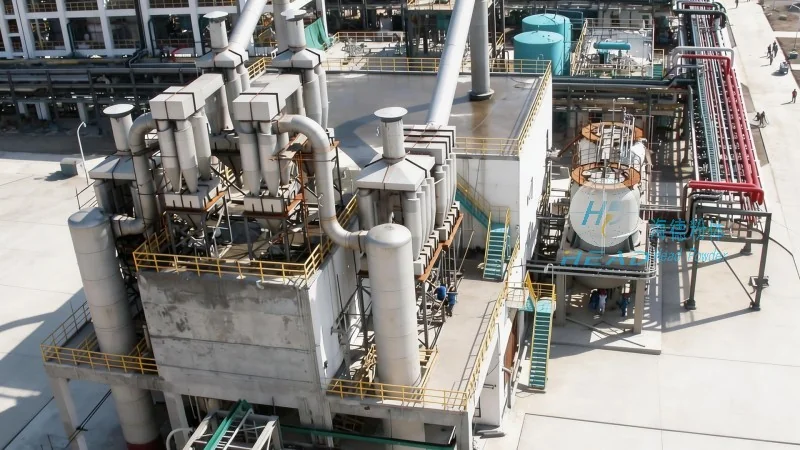
The conveyor itself is a central component, often enclosed within a metal or plastic housing to maintain the clean environment. It may use belt conveyors, roller conveyors, or chain conveyors, selected based on the material's size, weight, and required speed. The conveyor system is designed to move the material smoothly from the feeder to the discharge point, where it is either transferred to another processing unit or stored in a container. Throughout this process, the system continuously monitors and controls the air quality within the enclosure, adjusting filtration or ventilation as needed to maintain optimal conditions.
Applications and Benefits in Industrial Settings
Dust-free unpacking material conveyor lines are widely used in industries where product purity is paramount. In the pharmaceutical industry, for example, these systems ensure that raw materials are handled without introducing contaminants that could affect the efficacy or safety of the final drug product. In food processing, they maintain the hygiene standards required by regulatory bodies, preventing cross-contamination and ensuring that food products remain free from dust or foreign particles. Similarly, in electronics manufacturing, the system protects sensitive components from dust and static electricity, which could damage delicate circuits or components.
The benefits of implementing such a conveyor line extend beyond contamination control. By streamlining the material handling process, these systems improve operational efficiency and reduce labor costs associated with manual unpacking. They also enhance workplace safety by minimizing the risk of dust-related respiratory issues or other health hazards. Furthermore, the enclosed design reduces the need for extensive cleaning and maintenance, as the system is self-contained and less prone to external contamination.
Conclusion and Company Information
In conclusion, a dust-free unpacking material conveyor line is a critical piece of equipment for industries demanding high levels of cleanliness and product integrity. Its design, based on principles of containment, filtration, and controlled airflow, ensures that bulk materials are handled efficiently while maintaining an ultra-clean environment. For businesses seeking to enhance their material handling processes and meet stringent industry standards, investing in such a system can provide significant benefits in terms of quality control, efficiency, and safety.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of advanced material handling systems, including dust-free unpacking conveyor lines. With a focus on innovation and precision engineering, the company provides customized solutions tailored to the specific needs of various industries. Headquartered in Shandong, China, HeadPowder Engineering leverages years of experience and cutting-edge technology to deliver reliable and efficient equipment that meets the highest standards of performance and cleanliness. Whether for pharmaceutical, food, or electronics applications, their dust-free conveyor lines are engineered to deliver superior results and contribute to the success of their clients' operations.