

[WOKING PRINCIPLE AND FEATURES OF PNEUMATIC CONVEYING IN DUST EXTRACTION STATIONS]
HeadPowder, a leading manufacturer in the field of dust extraction and material handling systems, specializes in providing advanced solutions for industrial applications. This article delves into the working principle and key features of pneumatic conveying systems integrated within dust extraction stations, highlighting their efficiency and reliability in modern industrial operations.
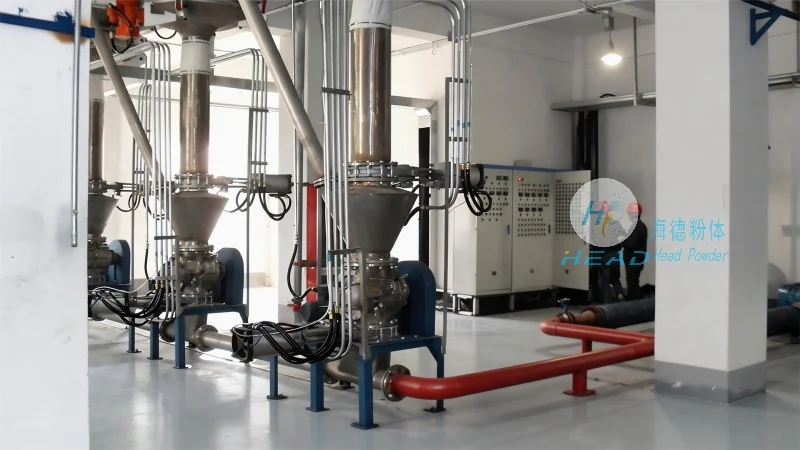
Understanding Pneumatic Conveying in Dust Extraction Stations
Pneumatic conveying is a method used to transport bulk materials through a pipeline using air or other gases. In dust extraction stations, this technology is crucial for efficiently removing airborne particles and transporting them to designated collection points. The system typically consists of a dust collector, a conveying pipeline, a fan or blower, and a material discharge unit. The working principle involves the fan creating a negative pressure (suction) or positive pressure (blowing) within the pipeline, which draws or pushes the dust-laden air and particles through the system.
Key Working Principle Components
The core components of a pneumatic conveying system in a dust extraction station include the dust collector, which captures airborne particles, and the conveying pipeline that transports the material. The fan or blower provides the necessary air flow to move the particles. The system operates by creating a pressure differential: when the fan operates in suction mode, it draws air and particles from the extraction point into the pipeline, while in blowing mode, it pushes material from a storage hopper into the pipeline. The material is then transported to a collection bin or silo, where it is stored for further processing or disposal.
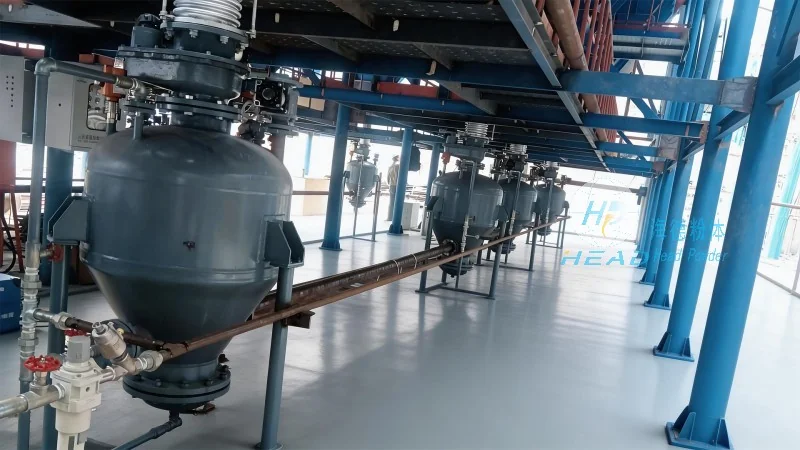
Advantages of Pneumatic Conveying Systems
Pneumatic conveying systems offer several advantages that make them ideal for dust extraction applications. One of the primary benefits is their ability to handle a wide range of materials, from fine powders to bulk solids, without the need for mechanical components like belts or buckets. This reduces maintenance costs and increases system reliability. Additionally, the system can be designed to operate in a closed loop, minimizing dust emissions and ensuring compliance with environmental regulations. The flexibility of the system allows for easy integration with existing dust extraction equipment, enhancing overall operational efficiency.
Key Features and Operational Benefits
HeadPowder's pneumatic conveying solutions are designed with several key features that enhance performance and user experience. The systems are equipped with advanced control panels that allow for precise regulation of air flow and pressure, ensuring optimal material transport. The use of high-quality materials for the pipeline and components ensures durability and resistance to corrosion, which is essential for long-term operation in industrial environments. Another notable feature is the system's ability to handle varying material properties, such as moisture content or particle size, without compromising performance. This adaptability makes the system suitable for diverse industrial applications, from pharmaceuticals to food processing.
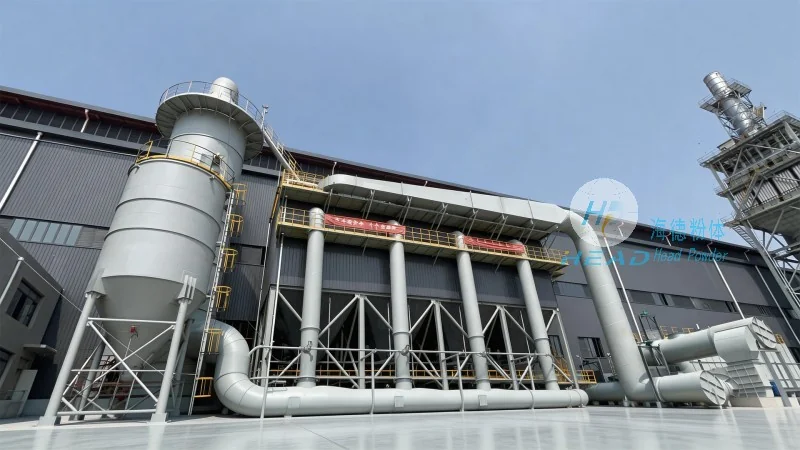
Efficiency and Environmental Impact
The efficiency of pneumatic conveying systems in dust extraction stations is a significant factor in their widespread adoption. By effectively capturing and transporting dust particles, these systems reduce the risk of contamination and improve workplace safety. The closed-loop design minimizes dust emissions, contributing to a cleaner working environment and compliance with environmental standards. Furthermore, the energy efficiency of modern pneumatic conveying systems, particularly those using high-efficiency fans and optimized pipeline designs, reduces operational costs and environmental impact. HeadPowder's commitment to using advanced technology ensures that their systems deliver superior performance while meeting the highest environmental and safety standards.
Conclusion
Pneumatic conveying systems in dust extraction stations are a critical component of modern industrial material handling and dust control. With their efficient operation, flexibility, and environmental benefits, these systems provide a reliable solution for managing dust and transporting materials. HeadPowder, with its expertise in engineering and manufacturing, continues to deliver high-quality pneumatic conveying solutions that meet the evolving needs of industrial applications. By understanding the working principle and features of these systems, industries can make informed decisions to enhance their operational efficiency and compliance with regulatory requirements.