Copper sulfate powder conveying systems operate on principles designed to efficiently handle the unique properties of copper sulfate, a common chemical used in agriculture, water treatment, and industrial processes. The core of the conveying process involves the movement of fine powder particles from a source to a destination, often utilizing mechanical or pneumatic methods. For copper sulfate, which has a relatively high density and can be prone to agglomeration under certain conditions, specialized equipment is employed to ensure consistent and reliable transport. The working principle typically begins with the loading of the powder into a hopper or storage silo. From there, the material is fed into a conveyor system, which may include screw conveyors, belt conveyors, or more advanced pneumatic systems. In pneumatic conveying, compressed air is used to create a flow that carries the powder particles through a pipeline, ensuring that even fine particles are transported without clogging. This method is particularly effective for copper sulfate because it minimizes the risk of dust generation and provides a controlled environment for handling the material. The system is designed to maintain a consistent flow rate, which is crucial for maintaining the quality of the powder and preventing degradation. Additionally, the conveying process may incorporate features such as vibration or agitation to break up any agglomerates, ensuring that the powder remains in a free-flowing state throughout the transport. The control system of the conveying equipment monitors parameters like pressure, flow rate, and temperature to optimize performance and prevent issues such as blockages or overloading. This automated control ensures that the copper sulfate is delivered to the processing or storage location with minimal loss and maximum efficiency.
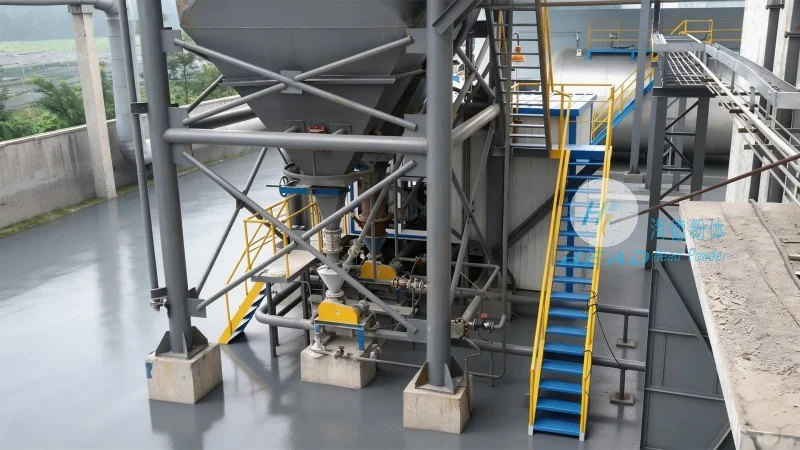
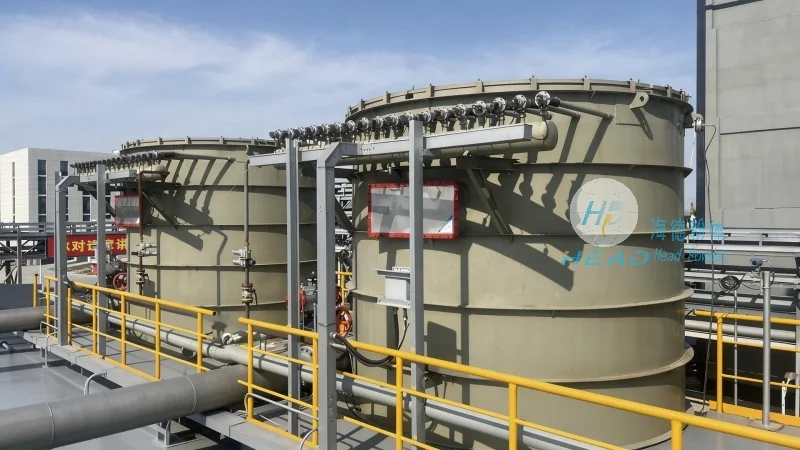
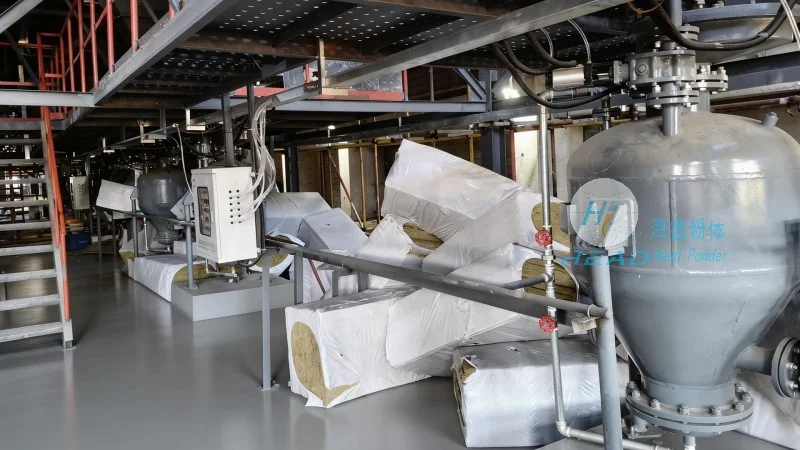
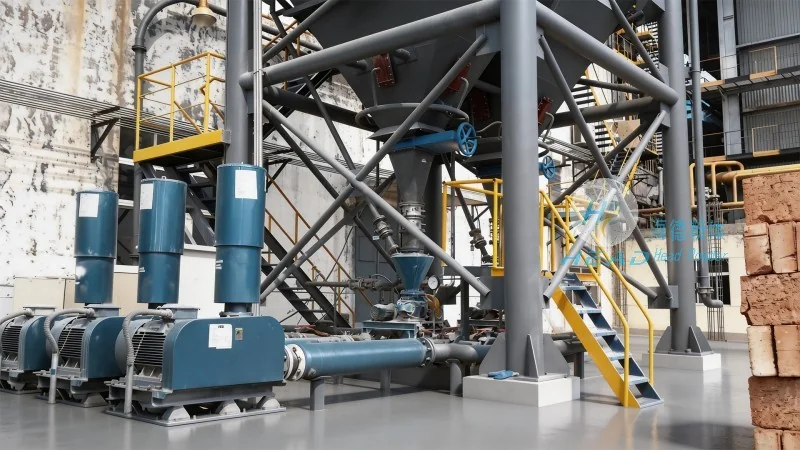
The characteristics of copper sulfate powder conveying systems are tailored to address the specific challenges associated with handling this material. One of the primary characteristics is the emphasis on dust control, as copper sulfate is a fine powder that can generate significant airborne dust, which poses health and safety risks. Advanced systems incorporate dust collection and filtration mechanisms to capture particles and return them to the conveying line, ensuring a clean and safe operation. Another important characteristic is the ability to handle varying particle sizes and moisture content. Copper sulfate powders can have a wide range of particle distributions, and the conveying system must be capable of accommodating these variations without compromising performance. This is achieved through adjustable feed mechanisms and flexible pipeline designs that can adapt to different flow conditions. The systems also prioritize energy efficiency, as the transport of powder can be energy-intensive, especially in large-scale operations. By optimizing the air pressure and flow rates, the conveying process minimizes energy consumption while maintaining the required throughput. Additionally, the systems are designed for durability and low maintenance, as they are exposed to abrasive materials and corrosive environments. High-quality materials, such as stainless steel or specialized coatings, are used to prevent wear and corrosion, ensuring a long service life. Safety features are also integral to the design, including emergency shut-off valves, pressure relief systems, and monitoring sensors that alert operators to any anomalies. These features contribute to a reliable and safe operation, reducing downtime and ensuring compliance with industrial safety standards. The flexibility of the conveying systems is another notable characteristic, as they can be integrated with existing production lines or adapted for new applications. This adaptability allows companies to scale their operations or modify their processes without significant investment in new equipment. Overall, the characteristics of copper sulfate powder conveying systems reflect a balance between efficiency, safety, and durability, making them suitable for a wide range of industrial applications.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized powder handling solutions, including copper sulfate powder conveying systems. With a focus on innovation and customer-centric design, the company has established itself as a trusted partner in the chemical processing industry. HeadPowder's expertise lies in understanding the unique challenges of handling fine powders like copper sulfate, and their solutions are tailored to meet the specific needs of each client. The company's facilities are located in Shandong, China, where they leverage advanced manufacturing capabilities and a skilled workforce to develop high-quality equipment. Their team of engineers and technicians work closely with clients to assess their operational requirements and design customized conveying systems that optimize performance and reduce costs. HeadPowder's commitment to quality is evident in their adherence to international standards and rigorous testing protocols. Each product undergoes thorough testing to ensure compliance with safety and performance criteria before being deployed in the field. The company also provides comprehensive after-sales support, including maintenance services, spare parts availability, and technical assistance, to ensure that clients can maintain the reliability of their conveying systems over the long term. By combining technical expertise with a customer-focused approach, Shandong HeadPowder Engineering Co., Ltd. delivers solutions that enhance productivity and safety in copper sulfate processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top