

Principle and Working Scene Characteristics of Bicarbonate Powder Pneumatic Conveying System
Bicarbonate powder pneumatic conveying systems represent a sophisticated method for transporting dry powders, such as sodium bicarbonate, through a pressurized or vacuum-driven air stream. This technology is widely utilized across various industries due to its efficiency, flexibility, and ability to handle fine powders without the need for mechanical components that might cause contamination or wear. The system's design and operational principles are tailored to meet the specific demands of material handling in industrial settings.
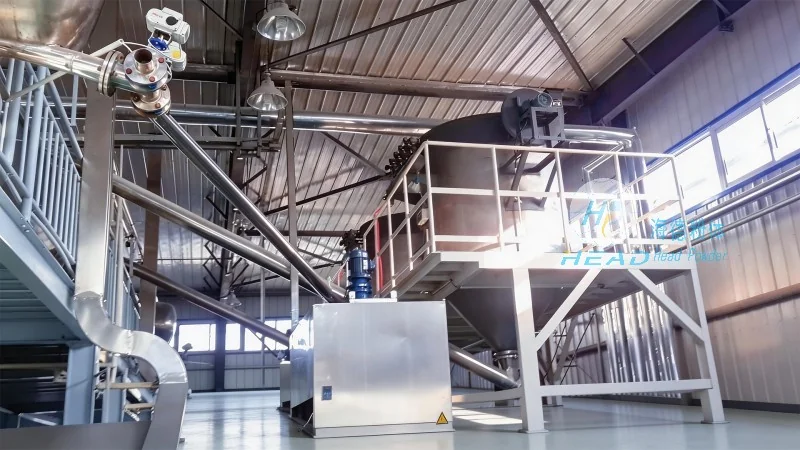
Working Principle of Bicarbonate Powder Pneumatic Conveying Systems
The core mechanism of a bicarbonate powder pneumatic conveying system involves the use of air or gas to transport the powder particles through a pipeline. There are two primary types of pneumatic conveying systems: pressure and vacuum. In a pressure system, the conveying air is supplied from a blower or compressor at a higher pressure than the ambient environment, pushing the powder through the pipeline. Conversely, a vacuum system uses a vacuum pump to create a negative pressure that draws the powder into the pipeline. For sodium bicarbonate, which is a fine, light powder, the pressure system is often preferred as it can maintain consistent flow rates and prevent particle segregation. The system typically includes components like a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The air flow is regulated to ensure the powder particles are suspended and transported efficiently without clogging or degradation.
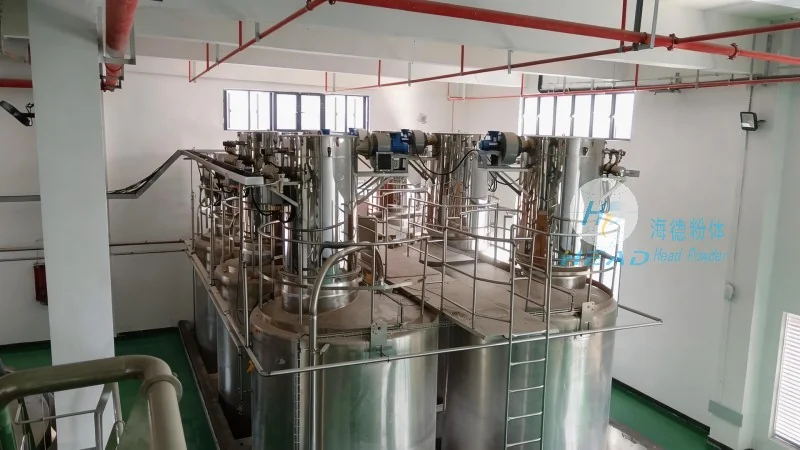
Key Working Scene Characteristics of Bicarbonate Powder Pneumatic Conveying Systems
The working scene characteristics of bicarbonate powder pneumatic conveying systems are defined by several critical factors that influence their performance and applicability. First, the system's ability to handle fine powders with low bulk density is a significant advantage. Sodium bicarbonate, being a light and fine powder, requires a conveying system that can maintain particle integrity and prevent agglomeration during transport. The design of the conveying line, including the use of smooth, non-stick surfaces and appropriate pipe diameters, is crucial to minimize friction and ensure consistent flow. Second, the system's adaptability to different operational environments is essential. In industrial settings, these systems are often integrated into larger production lines, requiring seamless coordination with other equipment like mixers, reactors, and packaging machines. The flexibility of pneumatic conveying allows for easy integration and reconfiguration of the system to accommodate changes in production volume or material types. Third, the system's efficiency in terms of energy consumption and material recovery is a key consideration. Modern pneumatic conveying systems are designed to optimize air usage, reducing energy costs while maximizing the recovery of the conveyed material. This is particularly important for valuable materials like sodium bicarbonate, where minimizing loss is critical to operational economics. Additionally, the system's ability to handle dust and maintain air quality is vital for compliance with environmental regulations and workplace safety standards. The use of filtration and dust collection systems in the conveying line helps to control particulate emissions and protect the surrounding environment and personnel.
Application Scenarios and Industry Integration
Bicarbonate powder pneumatic conveying systems are widely applied in various industries where sodium bicarbonate is a key raw material. In the food and beverage industry, these systems are used for transporting bicarbonate into production lines for baking, soft drink manufacturing, and other processes. The systems ensure that the powder is delivered in a clean, controlled manner, maintaining product quality and safety standards. In the chemical industry, the systems are employed in the production of baking soda, where the material is conveyed from storage to processing equipment like mixers and reactors. The ability to handle fine powders without contamination is critical in chemical applications, as any impurities can affect the final product's properties. In the pharmaceutical industry, the systems are used for the transport of bicarbonate in pharmaceutical manufacturing, where strict hygiene and contamination control are mandatory. The systems are often designed with sterile components and enclosed conveying lines to meet these stringent requirements. Furthermore, in the agricultural sector, bicarbonate is used as a fertilizer or soil amendment, and pneumatic conveying systems facilitate its distribution from storage to application equipment. The systems' portability and ease of use make them suitable for on-site agricultural operations. Overall, the working scene characteristics of these systems are tailored to the specific needs of each industry, ensuring efficient and reliable material handling.
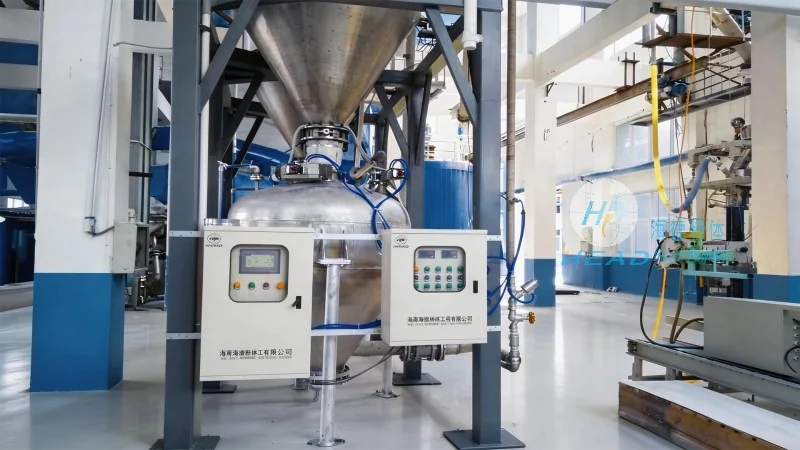
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for powder handling systems, including bicarbonate powder pneumatic conveying systems. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner in the development and implementation of advanced material handling technologies. The company's expertise lies in designing customized pneumatic conveying systems that meet the unique requirements of clients across various industries. With a focus on innovation and quality, HeadPowder employs a team of experienced engineers and technicians who work closely with clients to understand their operational challenges and provide tailored solutions. The company's facilities in Shandong are equipped with state-of-the-art equipment and testing capabilities, allowing for the development and testing of new systems before deployment. HeadPowder's commitment to customer satisfaction and operational excellence has earned it a reputation as a reliable supplier in the industry. By leveraging its technical expertise and industry knowledge, HeadPowder continues to deliver high-performance pneumatic conveying systems that enhance the efficiency and productivity of its clients' operations.