High-pressure bin pump pneumatic conveying systems represent a sophisticated technology in material handling, designed to efficiently transport bulk materials over long distances with minimal operational complexity. This article provides an overview of the system's structure and operational principles, highlighting its key components and how they work together to ensure reliable and efficient material transport.
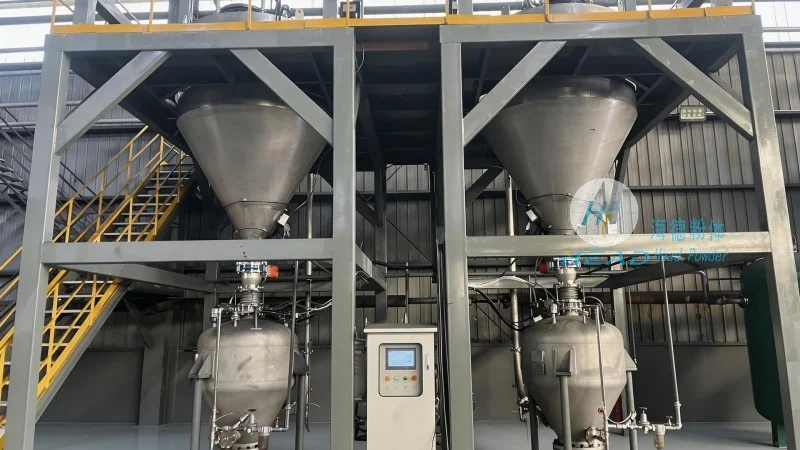
At the core of high-pressure bin pump systems is the bin pump, a critical component that acts as the primary transport mechanism. The system typically includes a storage bin or hopper where bulk materials are stored, a pump unit that generates the necessary pressure to move the material, and a conveying pipeline that delivers the material to the destination point. This configuration allows for continuous or batch operation, depending on the application requirements.
The high-pressure bin pump system comprises several essential parts, each playing a vital role in the overall operation. The storage bin or hopper is where raw materials are loaded, providing a consistent feed to the pump. The bin pump itself is a positive displacement pump that generates high-pressure air or gas to create a vacuum or pressure differential, enabling the material to be conveyed through the pipeline. The conveying pipeline, often made of durable materials like stainless steel or PVC, ensures the material is transported without degradation. Additionally, the system may include a control panel for monitoring and adjusting pressure, flow rate, and other operational parameters to maintain optimal performance.
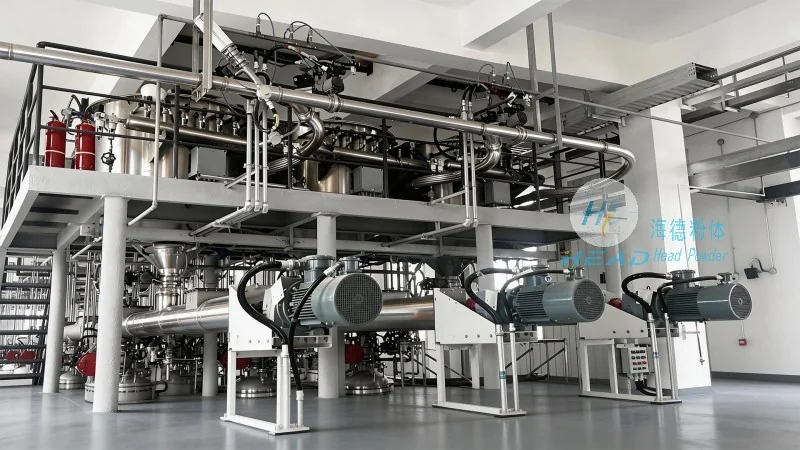
The operation of a high-pressure bin pump system is based on the principles of pneumatic conveying, where materials are suspended in a carrier gas (usually air) and transported through a pipeline. The pump generates high-pressure air, which creates a pressure difference between the inlet and outlet of the system. As the air flows through the pipeline, it pulls the material from the storage bin into the conveying line. The material is then carried to the discharge point, where the pressure is reduced, allowing the material to be deposited. The system can operate in either positive pressure or negative pressure modes, depending on the specific application and material characteristics.
High-pressure bin pump systems offer several advantages over traditional material handling methods. They provide a dust-free and enclosed transport process, which is crucial for materials that are dusty or have health hazards. The system is also capable of handling a wide range of materials, including powders, granules, and even some bulk solids. The ability to transport materials over long distances without the need for intermediate storage or handling points makes it an efficient solution for industrial applications. Furthermore, the system is relatively easy to install and maintain, with minimal downtime required for routine checks or repairs.

High-pressure bin pump pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, they are used to transport ingredients like flour, sugar, and spices, ensuring a hygienic and efficient process. In the pharmaceutical industry, the enclosed system helps maintain product purity and prevent contamination. The chemical industry utilizes these systems for handling powders and granules, such as fertilizers and pigments, while the mining industry uses them to transport raw materials from storage bins to processing facilities.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality material handling equipment, including high-pressure bin pump pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians dedicated to developing and manufacturing reliable and efficient equipment. HeadPowder's products are designed to meet the specific needs of various industries, ensuring optimal performance and durability. The company adheres to strict quality control standards, ensuring that each product meets or exceeds industry specifications. With a commitment to excellence, HeadPowder continues to provide top-tier solutions for material handling challenges worldwide.
 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China
telephone
WeChatconsult
top