

What is an Automatic Powder Bulk Bag Unloading Pneumatic Conveying System? And What Are Its Design P
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for material handling, particularly the automatic powder bulk bag unloading pneumatic conveying system. This system is engineered to streamline the process of handling bulk powders from sealed bags, converting them into a transportable form for further processing or distribution.
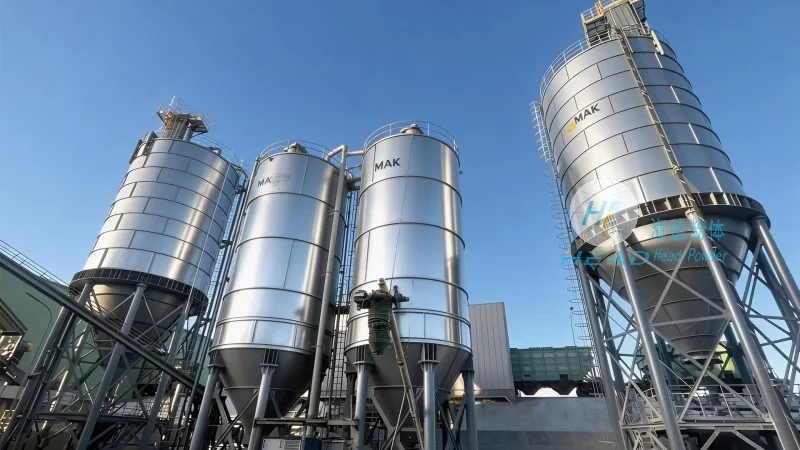
Understanding the Automatic Powder Bulk Bag Unloading Pneumatic Conveying System
The automatic powder bulk bag unloading pneumatic conveying system is a sophisticated piece of equipment designed to efficiently transfer powders from bulk bags (also known as FIBCs or flexible intermediate bulk containers) into a processing facility or storage area. The system eliminates the need for manual handling, which can be labor-intensive, time-consuming, and potentially hazardous. By automating the unloading and conveying process, it enhances operational efficiency and reduces the risk of material contamination or spills.
Key Components and Functionality
The system typically consists of several key components that work in tandem to achieve seamless operation. The primary components include the bulk bag discharger, the pneumatic conveying pipeline, the air compressor, and the dust collection system. The bulk bag discharger is responsible for opening the top of the bag and allowing the powder to flow out into the system. The pneumatic conveying pipeline uses compressed air to transport the powder from the discharger to the desired destination, such as a silo, hopper, or processing unit. The air compressor provides the necessary pressure to move the powder through the pipeline, while the dust collection system ensures that any airborne particles are captured and filtered, maintaining a clean and safe working environment.
Design Principles of the Pneumatic Conveying System
The design of the automatic powder bulk bag unloading pneumatic conveying system is based on several fundamental principles that ensure optimal performance and reliability. One of the core principles is the use of positive pressure or negative pressure (or a combination of both) to move the powder through the system. Positive pressure systems use an air compressor to force air and powder through the pipeline, while negative pressure systems create a vacuum to draw the powder into the system. The choice between these systems depends on factors such as the material being handled, the distance to be conveyed, and the desired flow rate.
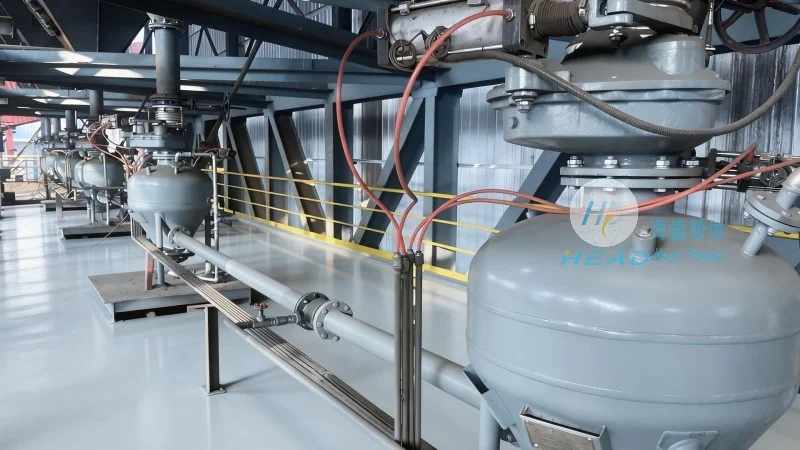
Another critical design principle is the selection of appropriate pipeline materials and diameters. The pipeline must be constructed from materials that are compatible with the powder being conveyed, such as stainless steel or plastic, to prevent corrosion or material buildup. The diameter of the pipeline is also crucial, as it determines the flow rate and pressure drop. Proper sizing ensures that the system operates efficiently without excessive energy consumption or pressure loss.
Advantages of the Automatic Bulk Bag Unloading System
Implementing an automatic powder bulk bag unloading pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly improves operational efficiency by reducing the time and labor required for manual unloading. This leads to increased production throughput and reduced downtime. Secondly, the system enhances safety by minimizing the risk of manual handling accidents, such as back injuries or exposure to dust. Thirdly, it improves material quality by preventing contamination and ensuring consistent flow rates. Additionally, the system reduces waste by minimizing material spillage and loss during the unloading process.
Applications and Industries
The automatic powder bulk bag unloading pneumatic conveying system is widely used in various industries that handle bulk powders, including food and beverage, pharmaceuticals, chemicals, and mining. In the food industry, it is used to handle ingredients like flour, sugar, and spices, ensuring that the products remain clean and free from contamination. In the pharmaceutical industry, the system is critical for handling active pharmaceutical ingredients (APIs) and excipients, as it maintains strict contamination control standards. In the chemical industry, it is used to convey materials such as powders, granules, and pellets, ensuring safe and efficient processing. The mining industry also benefits from this system by efficiently handling bulk materials like ore and minerals.
Customization and Integration
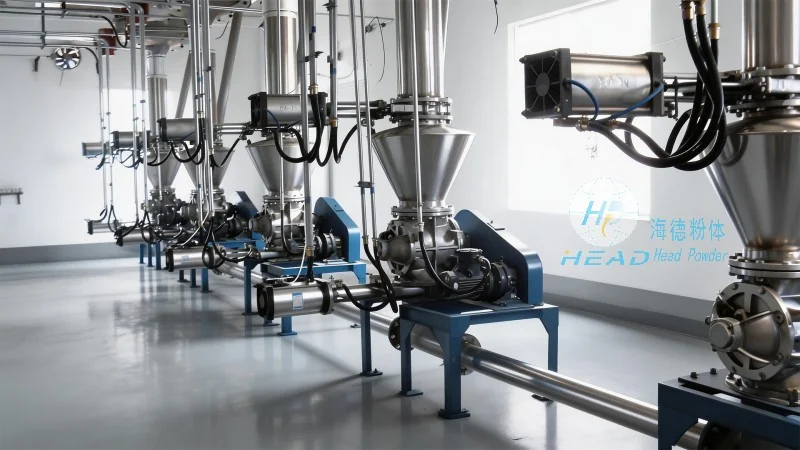
HeadPowder understands that each industrial application has unique requirements, and therefore, offers customized solutions for the automatic powder bulk bag unloading pneumatic conveying system. The company works closely with clients to understand their specific needs, such as the type of powder, the volume to be handled, and the distance to be conveyed. Based on this information, HeadPowder designs and manufactures a system that meets the client's requirements while ensuring optimal performance and reliability. The system can be integrated with existing processing equipment, such as silos, hoppers, and mixers, to create a seamless material handling process.
Maintenance and Support
Proper maintenance is essential to ensure the long-term performance and reliability of the automatic powder bulk bag unloading pneumatic conveying system. HeadPowder provides comprehensive maintenance and support services to its clients, including regular inspections, component replacement, and troubleshooting. The company's team of experienced technicians is available to provide on-site support and training to ensure that clients can operate and maintain the system effectively. By providing timely maintenance and support, HeadPowder helps clients maximize the lifespan of their equipment and minimize downtime.
Conclusion
The automatic powder bulk bag unloading pneumatic conveying system is a vital piece of equipment for industries that handle bulk powders. It offers numerous benefits, including improved efficiency, enhanced safety, and better material quality. HeadPowder, with its expertise and commitment to quality, provides reliable and customized solutions for this system, helping clients achieve their operational goals. By investing in this system, industries can streamline their material handling processes, reduce costs, and improve overall productivity.