

What is a Pharmaceutical Pneumatic Conveying System Equipment? What are its Design Principles?
Pharmaceutical pneumatic conveying systems represent a critical technology in the pharmaceutical industry, enabling the safe and efficient transport of powders, granules, and other bulk materials. These systems are essential for maintaining product integrity, ensuring regulatory compliance, and optimizing manufacturing processes. Understanding the functionality and design principles of such equipment is vital for pharmaceutical manufacturers seeking to enhance operational efficiency and product quality.
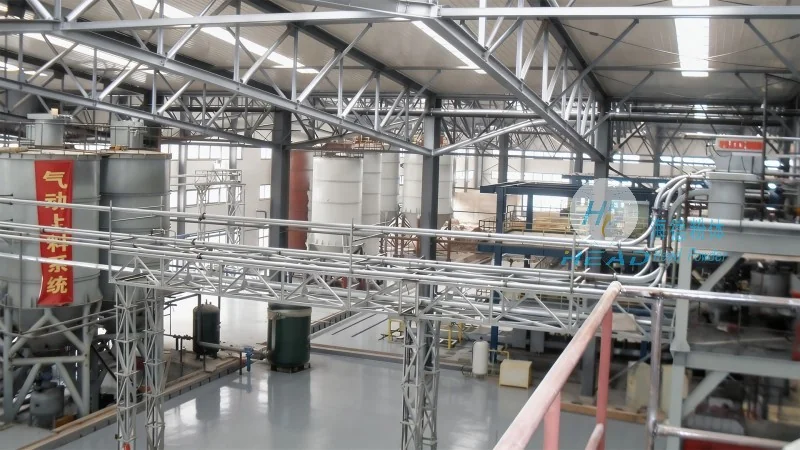
Overview of Pharmaceutical Pneumatic Conveying Systems
Pharmaceutical pneumatic conveying systems utilize air or gas to move materials through a closed or semi-closed system. Unlike mechanical conveying methods, which rely on physical contact or gravity, pneumatic systems use pressure differentials to transport materials. This approach offers several advantages, including reduced risk of contamination, improved material handling flexibility, and the ability to transport materials in sterile environments. The systems are commonly used in pharmaceutical manufacturing for tasks such as transferring raw materials, intermediates, and finished products between processing units, storage areas, and packaging lines.
Key Components and Their Functions
The primary components of a pharmaceutical pneumatic conveying system include a material hopper, a conveyor line (positive or negative pressure), a dust collector, and a discharge hopper. The material hopper serves as the initial storage and feeding unit, controlling the flow rate of the bulk material into the system. The conveyor line, which operates under either positive or negative pressure, moves the material through the system using air or gas. Positive pressure systems push material through the line, while negative pressure systems draw material from the source. A dust collector is integral to the system, capturing any airborne particles and preventing environmental contamination. The discharge hopper collects the material at the destination, ensuring controlled and consistent release.
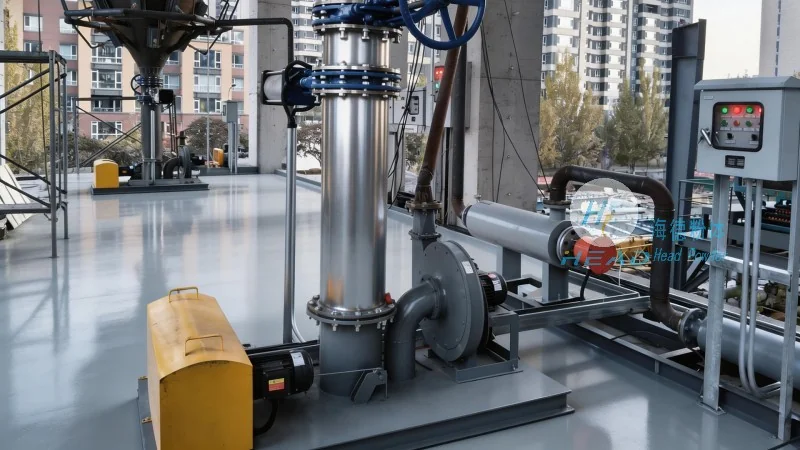
Design Principles for Optimal Performance
The design of pharmaceutical pneumatic conveying systems follows rigorous principles to ensure safety, efficiency, and compliance with industry standards. One fundamental principle is the use of sterile and non-contaminating materials, such as stainless steel, for all system components. This prevents cross-contamination and ensures product purity. Another key principle is the maintenance of a closed system, which minimizes exposure to external contaminants and maintains a controlled environment. Designers also consider factors such as material flow rates, air pressure, and system capacity to ensure the system can handle the required throughput without compromising performance. Additionally, the system must be designed for easy cleaning and sanitization, which is critical in pharmaceutical manufacturing to meet regulatory requirements.
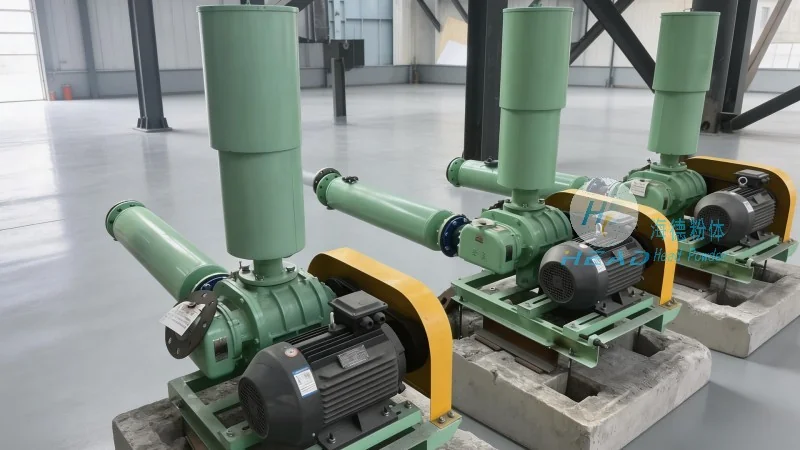
Operational Considerations and Maintenance Protocols
Operational considerations for pharmaceutical pneumatic conveying systems include regular maintenance to ensure long-term reliability and performance. This includes routine checks of air pressure, flow rates, and component integrity. Cleaning and sanitization procedures are also essential to prevent the buildup of residue or microbial growth. Proper maintenance helps prevent system downtime and ensures consistent product quality. Additionally, operators must be trained to handle the system safely, adhering to all safety protocols and regulatory guidelines. This includes understanding how to respond to system failures or leaks and ensuring that all components are properly maintained and replaced as needed.
HeadPowder Engineering Co., Ltd.: Your Trusted Partner in Pharmaceutical Conveying Solutions
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a leading manufacturer specializing in the design, development, and installation of pharmaceutical pneumatic conveying systems. With a strong commitment to quality and innovation, HeadPowder provides customized solutions tailored to the unique needs of pharmaceutical manufacturers. The company adheres to strict quality control standards and regulatory compliance, ensuring that its products meet the highest industry standards. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific requirements and develop efficient, reliable systems. The company's focus on customer satisfaction and technical excellence has established it as a trusted partner in the pharmaceutical industry, helping companies enhance their manufacturing processes and improve product quality.