

Introduction to Diatomite Powder Pneumatic Conveying and the Working Principle of Pneumatic Conveyin
HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With a focus on high-efficiency and reliable material transport, the company provides tailored solutions for various industrial applications, including the handling of diatomite powder—a lightweight, porous mineral widely used in filtration, cosmetics, and construction industries.
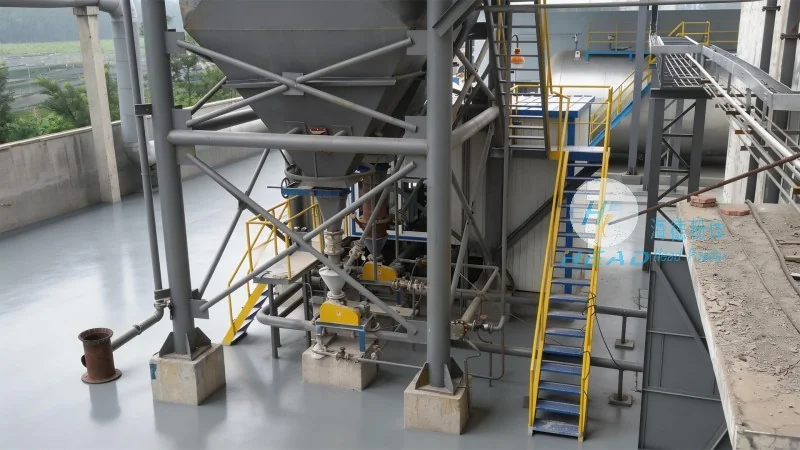
Understanding Diatomite Powder and Its Handling Challenges
Diatomite powder, derived from fossilized diatoms, is characterized by its low density, high porosity, and excellent filtration properties. These attributes make it a valuable raw material in multiple sectors, yet its fine particle size and light weight present unique challenges during transportation. Traditional methods like bucket elevators or belt conveyors often struggle with dust generation, material segregation, and system inefficiencies, especially when dealing with such delicate powders. This is where pneumatic conveying systems emerge as a superior alternative, offering a dust-free, continuous, and controlled transport solution.
The Fundamentals of Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. These systems are categorized into two primary types: positive pressure (or pressure) systems and negative pressure (or vacuum) systems. Positive pressure systems generate air pressure above atmospheric levels to push material through the pipeline, while negative pressure systems create a vacuum to draw material into the system. Both methods are designed to handle fine powders like diatomite efficiently, ensuring minimal loss and maximum material integrity.
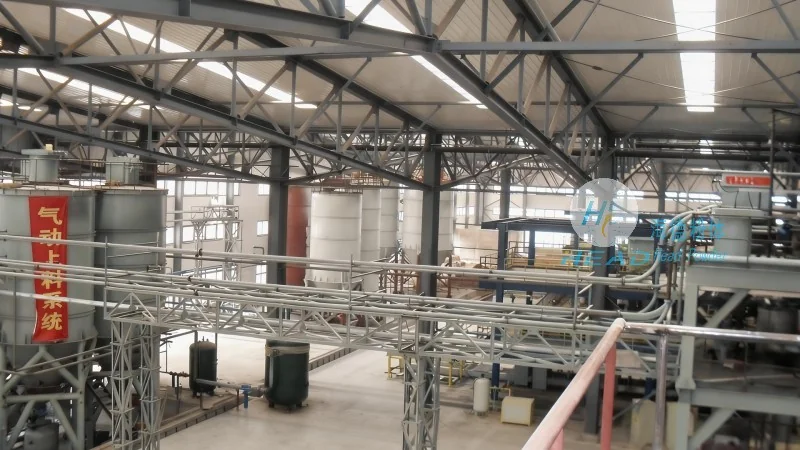
How a Diatomite Powder Pneumatic Conveying System Works
The operation of a diatomite powder pneumatic conveying system involves several key components and steps. First, the diatomite powder is fed into a hopper or feeder, where it is metered at a controlled rate to prevent overloading. Next, the material is introduced into the conveying line, either by a positive pressure blower or a vacuum pump, depending on the system design. The air or gas then carries the powder particles through the pipeline, maintaining a consistent flow rate and preventing clogging. At the destination point, the powder is separated from the air using a cyclone separator or a filter, and the air is either recirculated or vented. This process ensures that the diatomite powder reaches its final destination—such as a storage silo, processing plant, or packaging line—without degradation or loss.
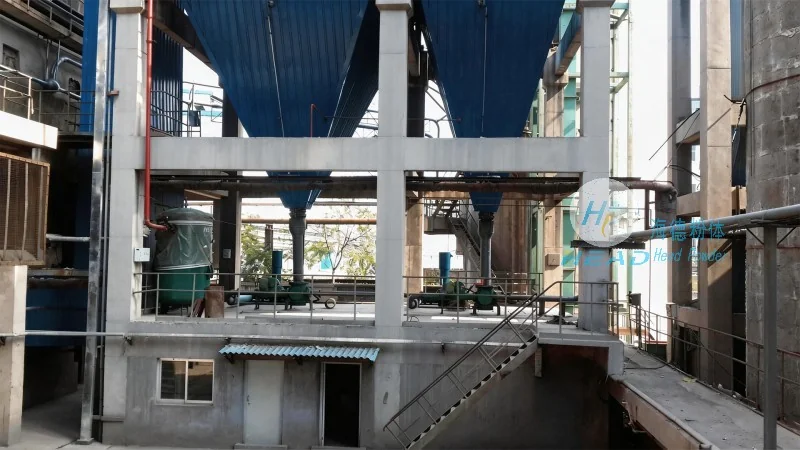
Key Advantages of Pneumatic Conveying for Diatomite Powder
Implementing a pneumatic conveying system for diatomite powder offers numerous benefits that enhance operational efficiency and product quality. Firstly, the system provides a dust-free environment, which is critical for maintaining product purity and ensuring workplace safety. Unlike mechanical conveyors, pneumatic systems do not generate dust clouds, reducing the risk of respiratory issues and contamination. Secondly, the continuous and controlled flow of material minimizes segregation and agglomeration, preserving the diatomite's fine particle structure and filtration properties. Thirdly, the system's compact design and flexible pipeline layout allow for easy integration into existing industrial facilities, adapting to various spatial constraints and layout requirements. Additionally, pneumatic conveying systems are highly scalable, capable of handling varying material volumes and flow rates, making them suitable for both small-scale and large-scale production environments.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer and supplier of advanced material handling equipment. With years of experience in the industry, the company has developed a strong reputation for delivering high-quality pneumatic conveying systems tailored to the specific needs of its clients. The company's team of engineers and technicians specializes in designing customized solutions that optimize material transport efficiency, reduce operational costs, and enhance overall productivity. HeadPowder's commitment to innovation and customer satisfaction has made it a trusted partner for businesses across various industries, including chemical, food, and pharmaceutical sectors. The company's facilities in Shandong are equipped with state-of-the-art technology and rigorous quality control measures, ensuring that every product meets the highest standards of performance and reliability.