Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in pneumatic conveying systems for mineral particles. This article provides an in-depth look at the working principle and key features of our equipment, designed to meet the demands of various industrial applications.
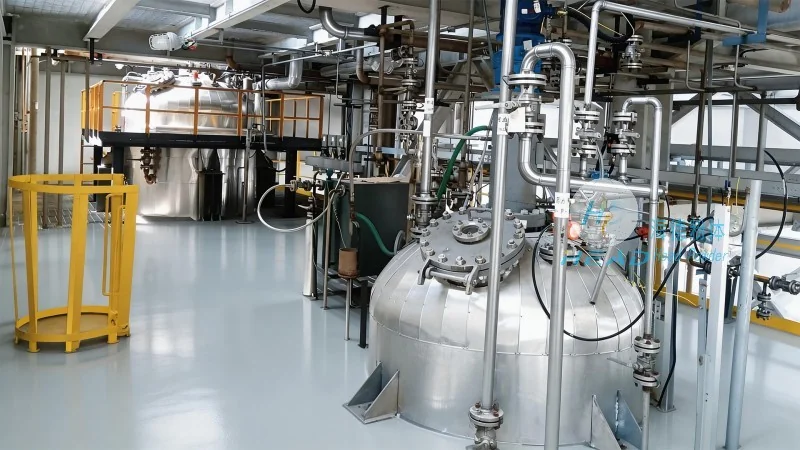
Pneumatic conveying systems for mineral particles operate by utilizing air or gas as the primary medium to transport bulk materials. The process typically involves a combination of positive and negative pressure zones to move materials from one location to another. At the inlet, the system draws in mineral particles and a controlled amount of air. The mixture is then accelerated through a pipeline network, where the air pressure and velocity are carefully managed to ensure efficient transport without damaging the particles. The system's design includes components such as feeders, cyclones, and filters to handle different particle sizes and flow rates. The working principle can be broadly categorized into two types: dilute-phase and dense-phase conveying. Dilute-phase systems use higher air velocities to move particles in a suspended state, while dense-phase systems operate at lower velocities, allowing particles to settle and be conveyed in a more compact form. This flexibility allows the system to adapt to various material characteristics and process requirements.
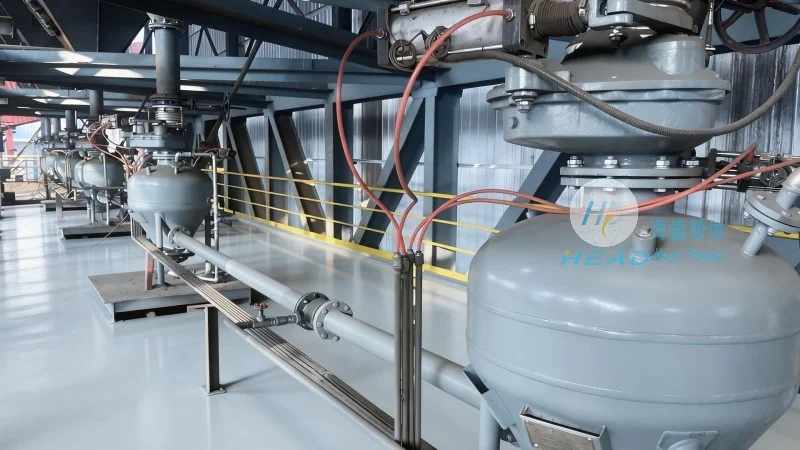
Our pneumatic conveying systems for mineral particles are engineered with several key features that enhance performance, reliability, and efficiency. One of the primary features is the ability to handle a wide range of particle sizes and densities, from fine powders to coarse granules. The system's modular design allows for easy integration into existing production lines, reducing installation time and costs. Another important feature is the low maintenance requirement, thanks to the use of durable materials and advanced components that minimize wear and tear. The equipment also incorporates advanced control systems that monitor pressure, flow, and particle concentration in real-time, ensuring optimal operation and preventing system failures. Additionally, the system is designed to be energy-efficient, with optimized air usage and minimal energy consumption. This not only reduces operational costs but also aligns with sustainability goals. The safety features, including explosion-proof designs and overpressure protection, ensure safe operation in industrial environments. The versatility of the system allows it to be used in various industries, including mining, chemical processing, and food processing, making it a versatile solution for bulk material handling.
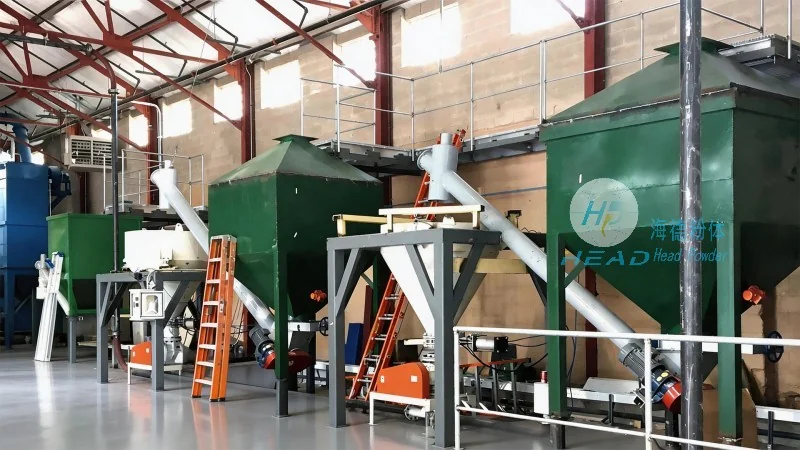
The mineral particle pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. offer numerous benefits in industrial applications. The primary advantage is the ability to transport materials over long distances without the need for mechanical components like belts or conveyors, which can be prone to maintenance issues. This reduces downtime and increases productivity. The system also provides a hygienic and dust-free environment, which is crucial in industries such as food and pharmaceuticals where contamination control is essential. The compact design of the equipment saves space in production facilities, allowing for better layout and workflow optimization. Furthermore, the system's ability to handle abrasive materials without significant wear ensures long service life and minimal replacement costs. The flexibility in system configuration allows for customization to meet specific customer requirements, ensuring that the equipment is tailored to the unique needs of each application. The overall efficiency of the system leads to lower operational costs and higher return on investment over time.
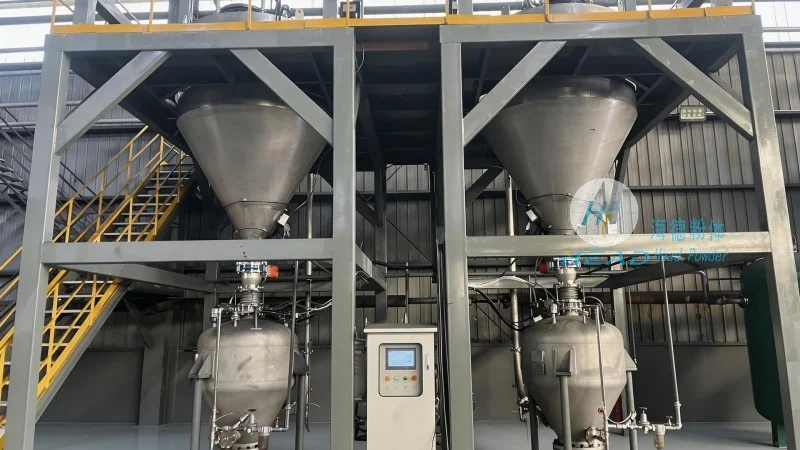
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality pneumatic conveying systems for mineral particles, combining advanced technology with reliable performance. Our equipment is designed to meet the diverse needs of industrial applications, offering efficient, safe, and cost-effective solutions for bulk material handling. With a focus on innovation and customer satisfaction, we continue to develop and improve our systems to meet the evolving demands of the industry. Based in Shandong, China, our company leverages local expertise and resources to deliver superior products and services to clients worldwide. Whether you are in the mining, chemical, or food industry, our pneumatic conveying systems are the ideal solution for your material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top