For industries dealing with bulk powder materials, efficient and reliable transport systems are crucial for operational efficiency and product quality. The metering bin pump, a specialized equipment designed for handling and transporting powders, plays a vital role in modern material processing. This article explores the working principle and key characteristics of the metering bin pump, providing insights into its application and performance in various industrial settings.
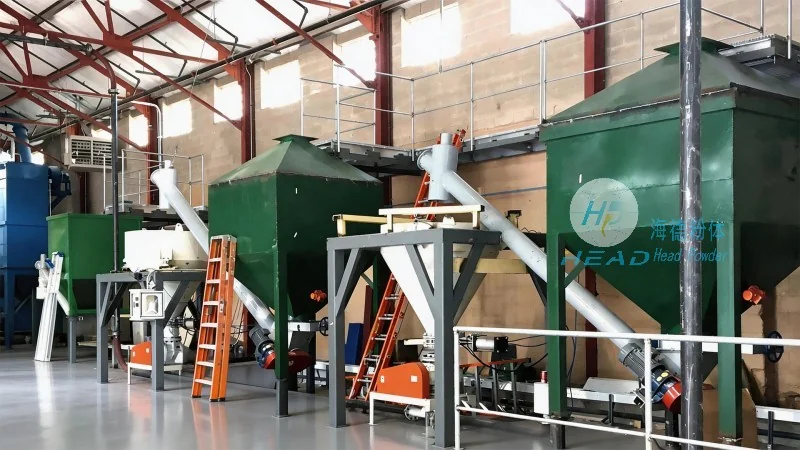
The metering bin pump, also known as a pressure bin pump or pneumatic bin pump, is a device used to transport dry bulk materials from a storage bin to a processing or delivery point. It operates by creating a pressure differential to move the material through a pipeline. The technology behind this equipment combines mechanical and pneumatic principles to ensure accurate and controlled powder handling. As a core component in many material handling systems, the metering bin pump is essential for industries such as cement, chemicals, food processing, and pharmaceuticals, where consistent flow and minimal material degradation are critical.
The working principle of the metering bin pump involves several key steps that ensure the smooth and controlled transport of powder materials. The process begins with the material being stored in a hopper or bin. When the pump is activated, compressed air is introduced into the bin, creating a pressure that forces the powder into the pump chamber. The pump then uses a diaphragm or piston mechanism to compress the air and material mixture, increasing the pressure and propelling the powder through the discharge line. The metering function is achieved through a controlled air supply, which regulates the flow rate of the material, ensuring precise delivery. This mechanism allows for consistent flow rates, even with varying material properties or bin levels. The pump can be operated in a continuous or intermittent mode, depending on the application requirements. The design of the metering bin pump ensures that the material is transported without segregation or degradation, maintaining the integrity of the powder.
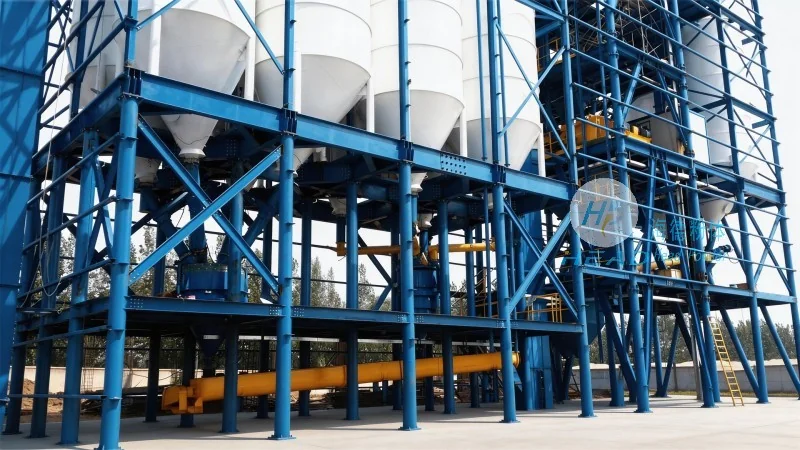
Several distinct characteristics define the metering bin pump and make it a preferred choice for powder handling applications. First, its ability to handle a wide range of powder types, from fine powders to coarse granules, without clogging or blockages. The pump's design minimizes friction and abrasion, reducing wear and extending the equipment's lifespan. Second, the metering capability provides precise control over the material flow rate, which is essential for processes that require exact dosing or batching. This feature enhances process control and reduces waste. Third, the pneumatic operation of the metering bin pump offers flexibility and safety. Unlike mechanical systems, it eliminates the risk of material contamination from lubricants and reduces the need for regular maintenance. The pump can be easily integrated into existing material handling systems, making it a cost-effective solution for upgrading or expanding operations. Additionally, the metering bin pump is compact and can be installed in various locations, including confined spaces, due to its lightweight and modular design.
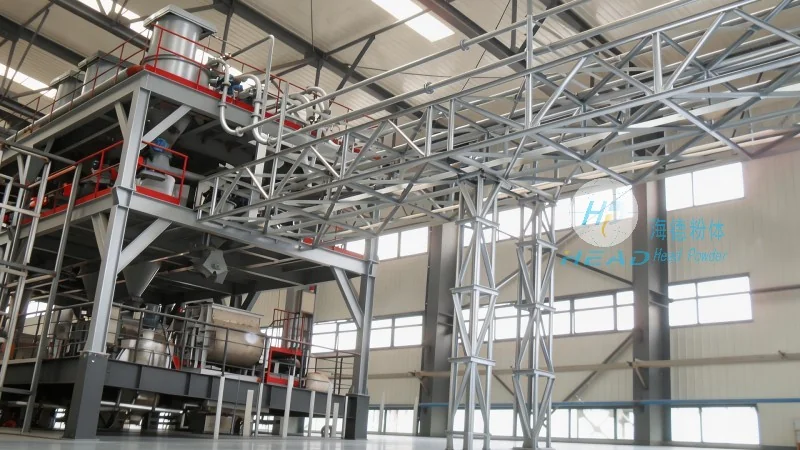
The metering bin pump is widely used in various industrial applications where reliable powder transport is required. In the cement industry, it is used to transport raw materials and finished products from storage silos to processing units. In the chemical industry, it handles reactive powders and additives, ensuring safe and controlled delivery. The food processing industry utilizes the metering bin pump for transporting flour, sugar, and other dry ingredients, maintaining hygiene and product quality. In the pharmaceutical sector, the pump is used for handling active pharmaceutical ingredients (APIs) and excipients, where precision and contamination control are paramount. The performance of the metering bin pump is characterized by high efficiency, with minimal energy consumption and low maintenance requirements. The equipment can operate continuously for extended periods without significant performance degradation, making it suitable for high-volume production environments. The ability to adjust the flow rate on the fly allows operators to adapt to changing production demands, enhancing operational flexibility.
In summary, the metering bin pump is a sophisticated piece of equipment that combines advanced engineering principles to provide efficient and reliable powder transport. Its working principle, based on pneumatic pressure and controlled metering, ensures consistent performance and minimal material degradation. The key characteristics, including versatility, precision, and safety, make it an ideal solution for various industrial applications. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality metering bin pumps tailored to meet the specific needs of different industries. With a focus on innovation and customer satisfaction, the company provides reliable equipment that enhances operational efficiency and product quality. Based in Shandong, China, HeadPowder has established itself as a trusted partner for businesses seeking advanced powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top