

Preventing Dust Leakage in Pneumatic Conveying Systems for Organic Fertilizer Granules
HeadPowder, also known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer specializing in pneumatic conveying systems. With a focus on industrial solutions, the company provides high-quality equipment tailored to various material handling needs, including the efficient and dust-free transport of organic fertilizer granules. HeadPowder is committed to delivering reliable and effective systems that meet the demands of modern agricultural and industrial applications.
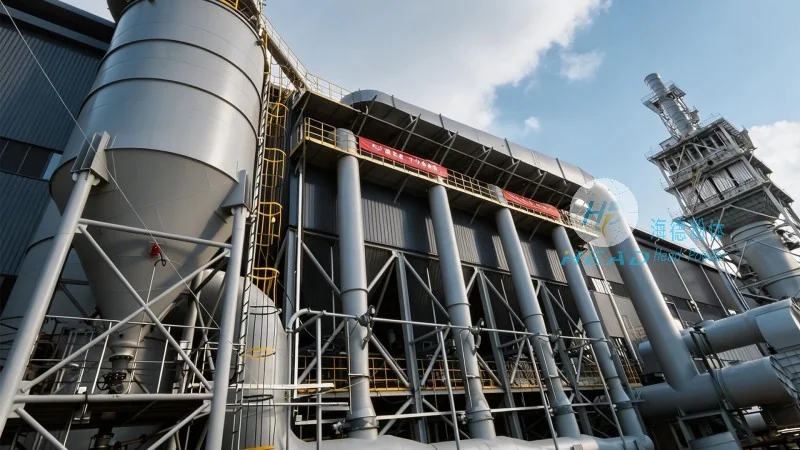
Pneumatic Conveying Systems for Organic Fertilizer Granules
HeadPowder's pneumatic conveying systems are engineered to handle organic fertilizer granules with precision and minimal dust generation. These systems utilize air pressure to move materials, offering a clean and efficient alternative to traditional bulk handling methods. The core technology involves a combination of high-efficiency airlocks, flexible hoses, and specialized dust collection units that work in tandem to ensure a dust-free operation. By integrating advanced materials and design principles, the systems are designed to maintain the integrity of the fertilizer granules while preventing any leakage or contamination. The product line is tailored to handle various granule sizes and moisture content, making it suitable for diverse organic fertilizer applications.
Techniques to Prevent Dust Leakage
Preventing dust leakage in pneumatic conveying systems for organic fertilizers involves several key strategies. One primary method is the use of high-quality airlocks that are specifically designed to seal the material feed points effectively. These airlocks are equipped with robust sealing mechanisms, such as rubber or metal gaskets, that create an airtight seal when the system is in operation. Additionally, the system incorporates advanced filtration and dust collection units that capture any airborne particles before they escape into the environment. The use of flexible, abrasion-resistant hoses also minimizes wear and tear, reducing the risk of leaks. Regular maintenance and inspection of these components are essential to ensure consistent performance and dust control. HeadPowder's systems are equipped with monitoring tools that alert operators to any potential issues, allowing for timely adjustments and preventing dust leakage incidents.
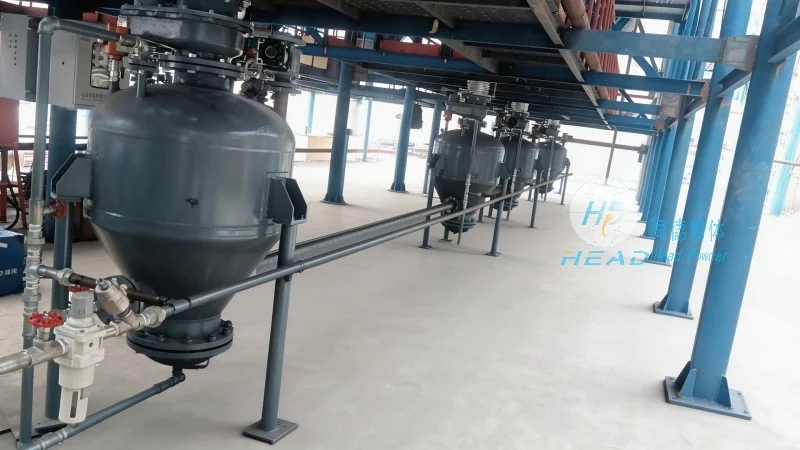
Technical Specifications and Design Features
The pneumatic conveying systems from HeadPowder are built with durability and efficiency in mind. The air handling units are designed to operate at optimal pressure levels, ensuring consistent material flow without excessive energy consumption. The system includes adjustable speed controls that allow operators to fine-tune the conveying rate based on the specific characteristics of the organic fertilizer granules. This adaptability is crucial for maintaining the quality of the material and preventing over-processing. The design also incorporates safety features, such as pressure relief valves, to protect the system from over-pressurization. The use of corrosion-resistant materials in the construction of the conveying lines and components ensures long-term reliability, even in harsh industrial environments. HeadPowder's engineering team continuously optimizes the system design to enhance performance and reduce operational costs, making it a cost-effective solution for organic fertilizer handling.
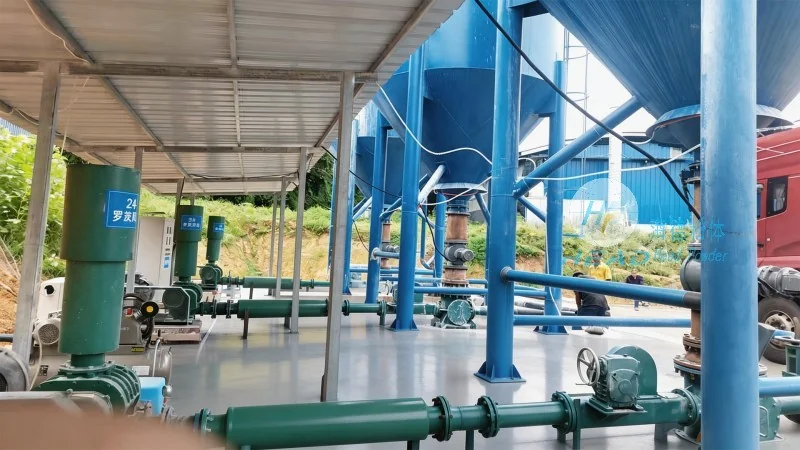
Real-World Applications
HeadPowder's pneumatic conveying systems have been successfully implemented in various organic fertilizer processing facilities across China. For instance, a large-scale organic fertilizer plant in Shandong Province has adopted the system to transport granules from storage silos to processing units. The implementation resulted in a significant reduction in dust emissions, improving workplace safety and compliance with environmental regulations. The system's ability to handle high volumes of material efficiently has also increased the plant's overall productivity. Another application involves a composting facility that uses the system to transfer processed organic matter to packaging lines. The dust-free operation has enhanced the quality of the final product, as the granules remain intact and free from contamination. These case studies demonstrate the effectiveness of HeadPowder's systems in addressing the unique challenges of organic fertilizer handling, including dust control and material integrity.
Conclusion
HeadPowder's pneumatic conveying systems offer a reliable and efficient solution for preventing dust leakage when transporting organic fertilizer granules. By integrating advanced sealing technologies, filtration systems, and robust design features, the company provides a comprehensive approach to material handling. The systems are tailored to meet the specific needs of organic fertilizer applications, ensuring minimal dust generation and maintaining the quality of the granules. With a commitment to quality and customer satisfaction, HeadPowder continues to be a leader in the industrial material handling sector, providing innovative solutions that enhance operational efficiency and environmental compliance. For businesses seeking to improve their organic fertilizer handling processes, HeadPowder's systems represent a valuable investment in reliability and performance.