

What is a Rice Starch Material Pneumatic Conveying Machine? And What Are Its Design Principles?
A pneumatic conveying machine, specifically designed for rice starch materials, is a crucial piece of equipment in the food processing and material handling industries. This type of equipment is engineered to transport dry, powdered materials like rice starch efficiently and safely through an enclosed system using air pressure. The primary goal is to ensure a reliable, dust-free, and low-maintenance method of material transfer, which is essential for maintaining product quality and operational efficiency in production lines.
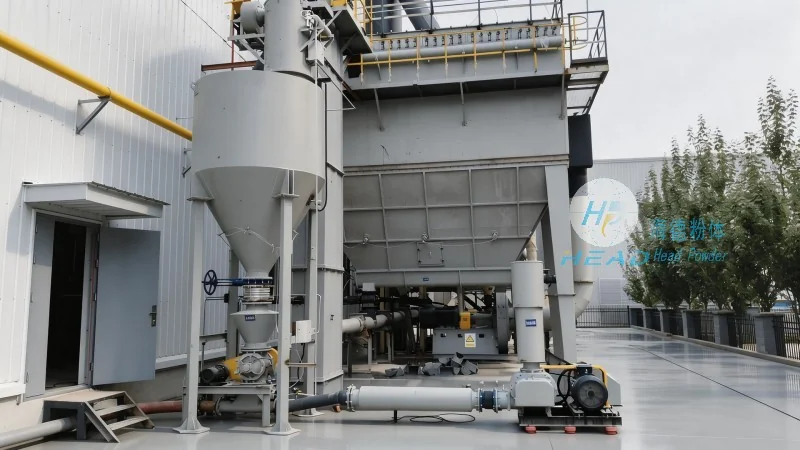
Key Design Principles of Pneumatic Conveying Systems
The design of a rice starch material pneumatic conveying machine is built on several fundamental principles that ensure optimal performance. First, the system relies on the creation of a pressure differential to move the material. This is typically achieved by using a blower or compressor to generate high-pressure air, which then propels the rice starch particles through the pipeline. The design must consider the specific properties of rice starch, such as its particle size, moisture content, and flowability, to prevent issues like blockages or degradation. Additionally, the system incorporates features like pulse jet technology or rotary valves to control the flow and prevent material buildup. The material handling process is also designed to minimize product contamination and maintain a consistent flow rate, which is critical for downstream processes like packaging or further processing.
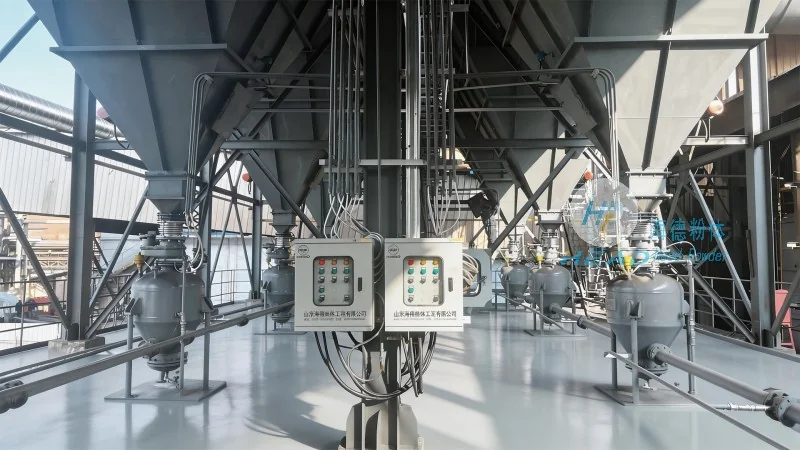
Components and Operational Mechanism
At the core of a rice starch pneumatic conveying machine are several key components that work in tandem to achieve effective material transport. The main components include a hopper for material storage, a feeder to control the flow rate, a blower or air compressor to generate the necessary air pressure, a pipeline system to guide the material, and a receiver or discharge hopper to collect the material at the destination. The operational mechanism begins when the rice starch is fed into the hopper. The feeder then regulates the amount of material released into the pipeline. The blower then creates a high-pressure air stream, which draws the rice starch particles into the pipeline and transports them to the receiver. The system may also include filters and cyclones to separate the material from the air, ensuring that the air is clean and the material is free from contaminants. The design of each component is critical to the overall efficiency and reliability of the system.
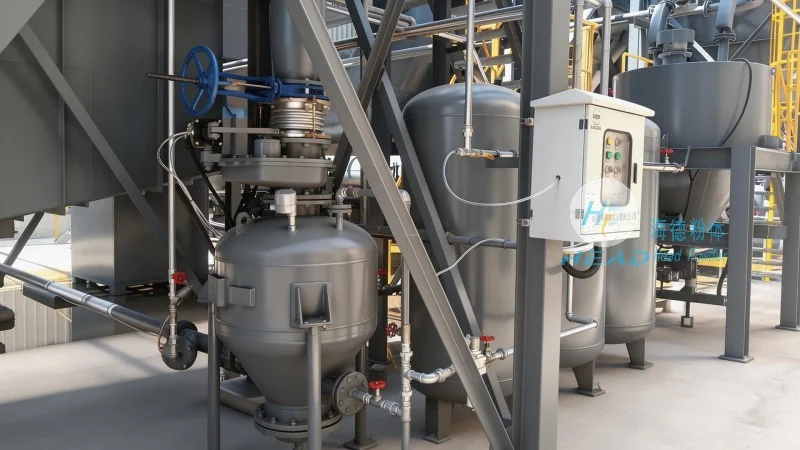
Benefits and Applications in the Food Industry
Using a specialized pneumatic conveying machine for rice starch offers numerous benefits for food processing facilities. One of the primary advantages is the ability to maintain a dust-free environment, which is essential for food safety and compliance with industry regulations. The enclosed system prevents the release of fine particles into the air, reducing the risk of contamination and improving workplace safety. Additionally, the system provides a high degree of control over the material flow, allowing for precise dosing and consistent product quality. This is particularly important in applications where the rice starch is used as an ingredient in other food products, as variations in the material can affect the final product's texture and taste. The machine also offers a low-maintenance solution compared to traditional mechanical conveyors, as there are fewer moving parts and less risk of mechanical failure. This reduces downtime and operational costs for the facility.
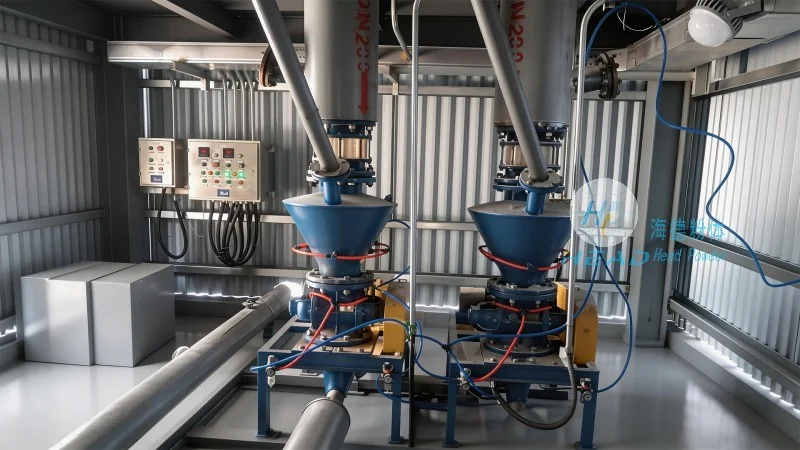
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and production of advanced material handling equipment, including pneumatic conveying systems tailored for various industrial applications. With a strong focus on innovation and customer satisfaction, the company has built a reputation for delivering high-quality, reliable, and efficient solutions for the food processing industry. HeadPowder's expertise lies in understanding the unique requirements of different materials, such as rice starch, and designing systems that meet those specific needs. The company's facilities are equipped with state-of-the-art technology and skilled professionals who ensure that each product is manufactured to the highest standards. By partnering with HeadPowder, food processing facilities can benefit from advanced equipment that enhances their operational efficiency and product quality. The company's commitment to quality and customer service makes it a trusted choice for businesses seeking reliable material handling solutions.